







Description
| Technical data | |
|---|---|
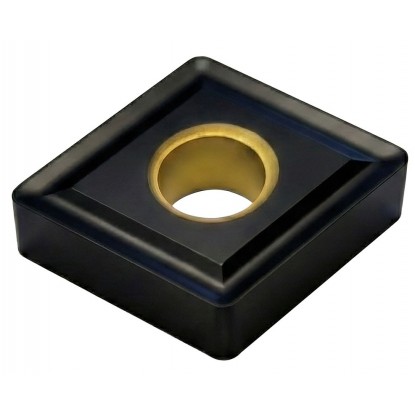
| Side length l | 12.7 mm |
| Insert thickness s | 4.76 mm |
| Hole diameter d1 | 5.16 mm |
| Corner radius rε | 1.2 mm |
| ANSI code | SNMG 433 |
finishing, semi-finishing, and roughing — ISO K group (cast iron)
| Material | Finishing | Semi-finishing | Roughing | ||||||
|---|---|---|---|---|---|---|---|---|---|
| Vc [m/min] | Feed f [mm/rev] | ap [mm] | Vc [m/min] | Feed f [mm/rev] | ap [mm] | Vc [m/min] | Feed f [mm/rev] | ap [mm] | |
| KCast iron | 180-300 | 0.1-0.2 | 0.5-2 | 120-180 | 0.2-0.4 | 1-4 | 100-150 | 0.3-0.6 | 2-6 |
double-sided 90° square with a hole and chip breaker
The SNMG 120412 turning insert is a double-sided, square indexable insert made of grade H5115 cemented carbide, designed for turning and boring cast iron castings. Shape S, a square with a 90° corner angle, provides a short, rigid edge with high strength — it withstands interrupted cuts and the hard inclusions typical of castings. Negative geometry with a 0° clearance angle allows both sides of the insert to be used, providing a total of eight cutting edges. The corner radius rε of 1.2 mm strengthens the cutting tip and allows higher feeds during semi-finishing and roughing. The hole with a chip breaker on both sides (type G according to ISO 1832) secures the insert and controls chip flow.
The SNMG 120412 insert (also written without a space as snmg120412) is suitable for external turning and boring of bodies, pulleys, bushings, and housings made of gray, ductile, and malleable cast iron. The CVD coating on grade H5115 allows cutting speeds up to approximately 400 m/min, reducing machining time in series production. Calculate spindle speed using the formula n = 1000·Vc/(π·D): for a shaft diameter of 80 mm at a cutting speed Vc = 250 m/min, the result is approximately 995 rpm. When roughing castings, maintain a depth of cut of several millimeters and a constant feed rate to load the cutting edge evenly. Indexable inserts in grade H5115 are supplied by the Korean brand Horn.
The 90° corner of the square insert is more robust than the corner of rhombic inserts, so it dissipates heat more effectively and is less prone to chipping with uneven casting allowances. In practice, this means predictable tool life in series production, provided the machine tool is fully rigid and the clamping is securely tightened. To make full use of all eight cutting edges, index the insert in its pocket only after the corner has become noticeably dull, and use compressed air or dust extraction instead of emulsion when machining cast iron.
Grade H5115 with a coating of CVD is optimized for cast iron (group ISO K). For turning structural steel or stainless steel, select an insert in a grade from group P or M — this coating performs differently on ductile materials than on cast iron.
how to read the SNMG 120412 code — designation positions 1–7
Designation SNMG 120412 according to the standard ISO 1832: 4 letters describe geometry and construction, 3 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
holders with a square 12 pocket — external turning and boring
use, turning tool selection, and turning parameters
Eight — a square has 4 corners per side, and the negative geometry (0° clearance angle) allows both sides of the insert to be used. Once a corner becomes dull, simply index the insert in its pocket without replacing the holder.
Holders with a square 12 pocket (IC 12.7 mm): for external turning TSSNR/L and PSSNR/L and TSDNN and PSDNN (45° entering angle), as well as TSKNR/L, PSKNR/L and PSBNR/L (75°) with shank cross sections of 20×20–32×32 mm; for boring, boring bars S25S–S50V with a TSKNR/L or PSKNR/L head. The full list is provided in the compatible turning tools section.
Only in corner radius: 0.4 mm is used for finishing at low feed rates, 0.8 mm is the general-purpose version, and 1.2 mm is selected for roughing castings at higher feed rates and depths of cut. The other dimensions (IC 12.7 mm, thickness 4.76 mm) are identical.
Grade H5115 is designed for cast iron (group ISO K) and provides the best tool life in this material. For structural steel or stainless steel, select an SNMG insert in a grade from group P or M, suited to ductile materials.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


