








Net price: €21.05
Description
| Technical data | |
|---|---|
| Side length l | 30 mm |
| Insert thickness s | 19.05 mm |
| Hole diameter d1 | 6.35 mm |
| Corner radius rε | 4 mm |
| Grade | 4025 (Sandvik) |
90° rectangle with a large corner radius for rough turning
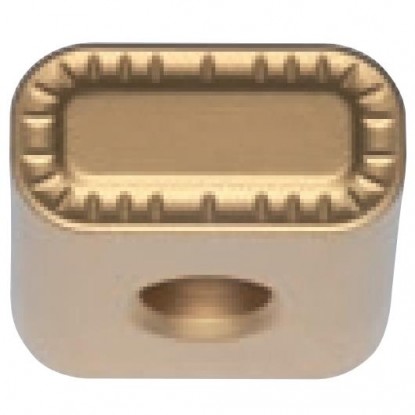
The LNUX 301940 turning insert is an indexable insert made of grade 4025 cemented carbide, designed for rough turning steel, cast steel, and stainless steel. The L shape, a rectangle with a 90° corner angle, and the large corner radius rε 4 mm create a strong edge for heavy stock removal. Negative geometry with a 0° clearance angle allows both sides of the insert to be used. With an edge length of 30 mm and a thickness of 19.05 mm, the insert withstands substantial cutting forces when machining profiles with varying cross sections. Tolerance class U indicates a broad dimensional tolerance range, acceptable for heavy roughing of large workpieces.
The LNUX 301940 insert (also written without a space as lnux301940) was developed for underfloor wheel lathes and turning wheelsets — locomotive and railcar wheels. It is suitable for applications that produce discontinuous chips with a large cross section and varying thickness, typical of railroad wheel reprofiling. Grade 4025 covers ISO P15-P40 and M25-M35, making it suitable for machining structural steel, cast steel, and stainless steel. The large corner radius distributes the load over a longer section of the edge and increases its resistance to chipping during rough turning. Unlike typical longitudinal turning inserts, the rectangular LNUX shape guides the edge along the profile rather than making contact only at the corner.
Select the cutting speed from the manufacturer's table for grade 4025. For reference, calculate the spindle speed using n = 1000·Vc/(π·D): at an example cutting speed of Vc = 120 m/min and a railway wheel diameter of 920 mm, the result is n ≈ 42 rpm. Such low speeds are typical of underfloor wheel lathes machining large diameters. Maintain rigid clamping of the workpiece and insert, as the large nose radius increases the radial component of the cutting force and promotes vibration on flexible parts. LNUX indexable inserts in grade 4025 are manufactured by the Swedish company Sandvik.
Grade 4025 covers ISO groups P15-P40 and M25-M35 — steel, cast steel, and stainless steel. It is not intended for cast iron, hardened materials, or aluminum alloys; select an appropriate insert grade for these applications.
how to read the LNUX 301940 code — designation positions 1–7
Designation LNUX 301940 according to the standard ISO 1832: 4 letters describe geometry and construction, 3 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
materials, applications, cutting edges, and nose radius
Grade 4025 covers groups ISO P15-P40 and M25-M35, namely structural steel, cast steel, and stainless steel. This carbide is intended for roughing operations that produce discontinuous chips with a large cross section and variable thickness. It is not used for cast iron or hardened materials.
It is an insert for underfloor wheel lathes and wheelset turning — wheel profiles on locomotives and railcars. The rectangular shape guides the cutting edge along the wheel profile being restored, while the large nose radius rε 4 mm increases edge resistance to chipping during rough stock removal.
The rectangular LNUX insert has two main cutting edges, and its negative geometry (clearance angle 0°) allows both sides of the insert to be used. When an edge wears out, the insert is indexed in the holder pocket without needing to be replaced.
Code 40 at position 7 of the designation, divided by 10, gives the radius rε = 4 mm. Such a large radius distributes the load over a longer section of the cutting edge and increases its strength during roughing. However, it increases the radial component of the cutting force, so rigid clamping of the workpiece and holder is required.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


