 Polski






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot
Description
Technical data for the M12 INOX die for stainless steel
| Technical Data | |
|---|---|
| Thread size D1 | M12 |
| Thread Pitch P | 1.75 mm |
| Outside Diameter D2 | 38 mm |
| Thickness H1 | 14 mm |
| Number of Chip Holes | 4 |
| Required Shaft Diameter | 11.83 mm |
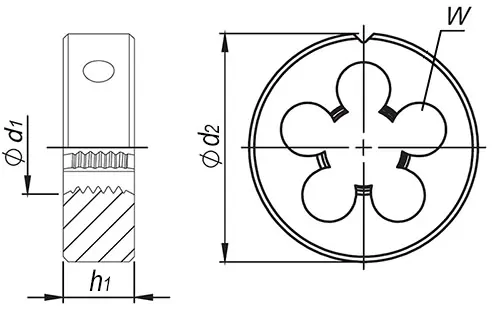
M12 HSSE die – professional stainless steel threading
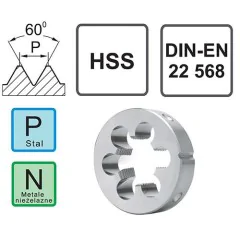
The M12 HSSE die is a top-quality tool designed for intensive threading of stainless steels and difficult-to-machine materials. Made from cobalt high-speed steel HSSE, M12 threading die meets the stringent requirements of DIN 22568 and ensures durable external threads in industrial installations, chemical equipment, and structures exposed to corrosion, with a tolerance of 6g.
Key features of the M12 HSSE die
- Cobalt HSSE steel provides a hardness of 67 HRC and heat resistance up to 600°C
- Versatile M12 size most commonly used in stainless steel industrial installations
- Polish manufacturer Fanar offers certified tool quality competitive with global brands
- Special cutting edge geometry reduces the chip adhesion typical of INOX
- Tool life increased by 250 percent compared with standard HSS dies
Plumbing installers and technicians in the food and pharmaceutical industries rely on the M12 HSSE metric die when making threaded connections in aggressive environments. Designed for plants manufacturing tanks, pipelines, and process equipment from austenitic steel. Choose a tool from a Polish manufacturer that delivers professional results in the most demanding corrosion-resistant applications.
Frequently asked questions
When threading stainless steel with the M12 HSSE die, use a peripheral speed of 3-5 meters per minute, corresponding to approximately 80-130 rpm at a diameter of 12 mm. Work sequentially - make one full turn forward, then half a turn backward for effective chip breaking. Avoid continuous threading without reversing, as stainless steel work-hardens during cutting and may cause the tool to seize.
The M12 HSSE die performs best in austenitic steels such as AISI 304, 316, and ferritic AISI 430. Threading duplex or hardened stainless steels requires lower speeds and more intensive lubrication. Superaustenitic steels with a nickel content above 25 percent may require dies with AlTiN coatings. Use on martensitic steels hardened above 35 HRC is not recommended without prior machining trials.
Under optimal conditions, the M12 HSSE INOX die can cut 300-500 threads in AISI 304 austenitic stainless steel or 200-350 in the harder AISI 316. By comparison, a standard HSS die lasts for only 100-150 threads. Key factors include lubrication quality, operating speed, and correct technique with regular reversing. With professional use, the tool can last several years in a workshop with moderate production intensity.
Product accessories


Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you




Viewed products


This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.