







Description
| Technical data | |
|---|---|
| Side length l | 8.7 mm |
| Insert thickness s | 4.76 mm |
| Hole diameter d1 | 5.16 mm |
| Corner radius rε | 0.8 mm |
| Inscribed circle diameter IC | 12.7 mm |
| ANSI code | WNMG 432 |
semi-finishing — ISO N materials
| Material | Semi-finishing | |
|---|---|---|
| Vc [m/min] | Feed f [mm/rev] | |
| NAluminum and nonferrous metals | 60-130 | 0.15 |
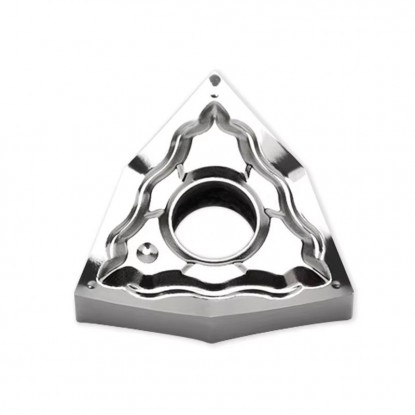
double-sided 80° trigon with a hole and chip breaker
The WNMG 080408 turning insert is a double-sided, trigon-shaped indexable insert made of fine-grained grade K10 cemented carbide, designed for turning aluminum and other nonferrous metals. Shape W, a trigon with a 80° corner angle, combines strength similar to a square insert with better access to the workpiece contour. The negative geometry with a 0° clearance angle allows both sides of the insert to be used — a total of six cutting edges. The rε 0.8 mm nose radius and sharp, often polished cutting edge limit built-up edge and maintain a smooth surface at a feed rate of approximately 0.15 mm/rev. Tolerance class M ensures repeatable cutting edge positioning after indexing the insert in the holder seat.
The WNMG 080408 insert is suitable for turning shafts, bushings, flanges, and housings made of aluminum alloys, brass, and bronze on conventional and CNC lathes. Fine-grained K10 carbide maintains cutting edge sharpness, which is essential for soft, ductile nonferrous materials prone to built-up edge. The hole with a double-sided chip breaker (type G per ISO 1832) controls the flow of long, ductile aluminum chips and protects the machined surface from scratching. Flood cooling with emulsion or oil also flushes chips out of the cutting zone and stabilizes the cutting edge temperature. The trigon shape is suitable for longitudinal turning, facing, and light copy turning without changing the insert.
The WNMG 080408 insert (also written without a space as wnmg080408) operates at a cutting speed of 60–130 m/min and a feed rate of 0.15 mm/rev in semi-finishing. Calculate spindle speed using n = 1000·Vc/(π·D): for a shaft diameter of 40 mm at Vc = 130 m/min, the result is approximately 1035 rpm. For smaller diameters, increase spindle speed to maintain the recommended cutting speed and limit built-up edge. Excessively low cutting speed promotes built-up edge and reduces surface finish quality, so for small diameters it is advisable to approach the upper end of the Vc range. Indexable inserts in grade K10 are supplied by the Korean brand Horn.
Grade K10 is intended for nonferrous metals (group ISO N). For turning structural steel or stainless steel, select an insert in a general-purpose grade from group ISO P/M — the sharp cutting edge for aluminum wears faster on steel materials.
how to read the WNMG 080408 code — positions 1–7 of the designation
Designation WNMG 080408 according to the standard ISO 1832: 4 letters describe geometry and construction, 3 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
holders with a 08 trigon pocket — external and internal turning
use, turning tool selection, and turning parameters
Six — the trigon has 3 corners per side, and the negative geometry (clearance angle 0°) allows both sides of the insert to be used. When a corner becomes dull, simply index the insert in the pocket without changing the holder.
Holders with a size 08 trigon insert seat: for external turning TWLNR/L, PWLNR/L and MWLNR/L (entering angle 95°) and MWDNN (50°) with shank cross sections of 20×20–40×40 mm; for internal turning, boring bars S25S–S50V with the suffix TWLNR/L, PWLNR/L, or MWLNR/L.
Only in corner radius: 0.4 mm is used for finishing at low feed rates, 0.8 mm is the general-purpose version, and 1.2 mm is selected for roughing. The remaining dimensions (IC 12.7 mm, thickness 4.76 mm) are identical.
Grade K10 is intended for aluminum and nonferrous metals (group ISO N), and its sharp, uncoated cutting edge wears faster on steel. For turning structural or stainless steel, select a WNMG insert in a general-purpose grade from group ISO P/M.

Reference: 0000004240 In stock > 10 items
€6.47 brutto
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


