







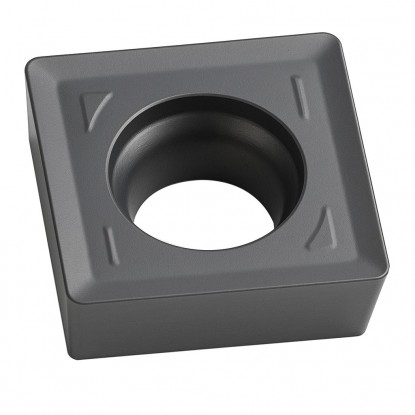

Description
| Technical data | |
|---|---|
| Side length l | 6.35 mm |
| Insert thickness s | 3.2 mm |
| Hole diameter d1 | 2.8 mm |
| Corner radius rε | 0.4 mm |
| Geometry code | DM — meaning according to the product data sheet |
| Carbide grade | H6018 (PVD) |
| ISO groups 513 | P (steel), M (stainless steel) |
| Brand | Horn |
disc milling and slot milling — conservative ranges for ISO P and M groups
| Material | Vc [m/min] | Feed per tooth fz [mm/tooth] | ap [mm] |
|---|---|---|---|
| PSteel | 130-200 | 0.10-0.20 | 1.0-4.0 |
| MStainless steel | 70-130 | 0.06-0.15 | 0.5-2.0 |
DM code without interpretation, PVD coating, ISO P and M groups
Milling insert MPHT 060304 is a replaceable cemented carbide indexable insert in grade H6018, designed for indexable milling cutters, primarily disc cutters. A disc cutter with replaceable inserts cuts narrow slots and parts off material without requiring the tool body to be resharpened. DM is the manufacturer's code; its properties in interrupted cutting require confirmation in the product data sheet. The PVD (physical vapor deposition) coating on grade H6018 increases the edge's resistance to abrasive wear and thermal shock. As a result, the insert maintains its performance even during prolonged, intensive use. The design covers material groups ISO P (steel) and ISO M (stainless steel), allowing the same insert type to be used in one-off and series production.
The MPHT 060304 indexable insert is suitable for slot milling, parting, and face milling narrow surfaces in structural steel and stainless steel with a disc cutter. Calculate spindle speed using n = 1000·Vc/(π·D): for a disc cutter with a diameter of 80 mm at a cutting speed Vc of 150 m/min, the result is approximately 597 rpm. Then calculate the table feed rate as vf = fz·z·n; with 10 inserts in the body and a feed per tooth (fz) of 0.1 mm, this gives nearly 597 mm/min. On CNC machining centers, use climb milling, which further extends cutting edge life.
For austenitic stainless steel, keep the cutting speed in the lower part of the range and maintain a constant feed to limit work hardening of the layer being cut and built-up edge formation. The positive insert geometry reduces cutting forces, which helps on less rigid machines and with longer milling arbors. Select a depth of cut that does not exceed the active cutting edge length, and apply a generous flow of emulsion for consistent chip and heat removal. Grade H6018 indexable inserts are supplied by the Korean brand Horn.
Grade H6018 is not intended for hardened steels above 45 HRC. For harder materials, select an insert in a more resistant grade, and always set the cutting data according to the data sheet for the specific disc cutter.
how to read the MPHT 060304 code — designation positions 1–7
Designation MPHT 060304 according to the standard ISO 1832: 4 letters describe geometry and construction, 3 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
ISO 1832 designation decoder — how to read the code
Positions 1–4 · ISO code
1MShape
86° rhombus
2 corners of 86° per side
2PClearance angle
α = 11°
positive, single-sided
3HTolerance
Class H (high precision)
ground insert — highest dimensional accuracy
4TType
Countersunk hole + chip breaker
countersink 40–60°, single-sided chip breaker
Positions 5–7 · dimensions [mm]
506Edge length
l = 6.35 mm
code 06 → edge length
603Thickness
s = 3.18 mm
between rake faces
704Corner radius
rε = 0.4 mm
code ÷ 10 → radius in mm
✓ 2 corners × 1 side = 2 cutting edges
disc cutters with an MPHT pocket — ISO P and M material range
Suitable applications:
| ✔ | Indexable disc cutters (slotting, parting) with an MPHT 060304 pocket |
| ✔ | Slot milling, parting, and face milling narrow surfaces |
| ✔ | Machining structural steels in ISO group P (P20-P40) |
| ✔ | Machining stainless steels in ISO group M (M20-M40) |
| ✔ | Interrupted cutting — after confirming the application of the DM code in the product data sheet |
| ✗ | Hardened steels above 45 HRC — outside the range of grade H6018 |
| ✗ | Aluminum and light alloys — sharp geometry for ISO group N required |
mounting, material selection, and milling parameters
Indexable milling cutters, primarily disc cutters with an MPHT pocket. The insert is secured with a central screw through a hole with a diameter of 2.8 mm. Always check the pocket designation in the data sheet for the specific cutter body.
Grade H6018 is a PVD-coated carbide for groups ISO P20-P40 (steel) and ISO M20-M40 (stainless steel). It is not suitable for hardened steels above 45 HRC or for aluminum alloys.
DM is a manufacturer code. Cutting characteristics should not be attributed to it without the product data sheet.
Use the formula n = 1000·Vc/(π·D). For a cutter with a diameter of 80 mm at Vc 150 m/min the result is approximately 597 rpm. Feed rate: vf = fz·z·n; with 10 inserts and fz 0.1 mm, it is approximately 597 mm/min. Verify the values against the tool data sheet.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


