






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot
Description
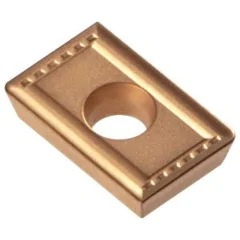
APKT 160408 milling insert – 85° rectangular insert for 90° milling heads
| Technical data | |
|---|---|
| Side length l | 16 mm |
| Insert thickness s | 4.76 mm |
| Corner radius rε | 0.8 mm |
| Clearance angle | 11° (P) |
| Number of edges | 2 |

APKT indexable insert — cutting data for steel and stainless steel
90° shoulder milling — conservative ranges for ISO P and M groups
| Material | Vc [m/min] | Feed per tooth fz [mm/tooth] | ap [mm] |
|---|---|---|---|
| PSteel | 130-200 | 0.10-0.20 | 1-4 |
| MStainless steel | 70-130 | 0.06-0.15 | 0.5-2 |
H6310 carbide insert – design and 90° shoulder milling
positive 85° rectangle with PVD coating for milling heads and indexable milling cutters
The APKT 160408 PDER milling insert is a positive indexable cemented carbide insert in grade H6310, designed for shoulder milling in steel and stainless steel. Shape A is a rectangle with a 85° corner angle. Combined with a 90° entering angle, it allows a vertical shoulder and a flat workpiece floor to be machined in one pass. The positive geometry with a 11° clearance angle reduces cutting resistance and spindle power consumption. The TiAlN PVD coating, deposited by physical vapor deposition, improves edge wear resistance and thermal stability at higher speeds. The corner radius rε 0.8 mm combines cutting edge strength with a smooth machined surface. Each insert provides two cutting edges, used in succession by rotating the insert in the milling head pocket.
Key benefits of the H6310 carbide milling insert
- Two cutting edges — the 85° rectangle provides 2 working corners on one insert; once worn, simply rotate the insert in the milling head pocket.
- Grade H6310 for ISO groups P and M — PVD-coated carbide for steel (P20-P40) and stainless steel (M20-M40) in a single item.
- Positive 11° geometry — lower cutting resistance and reduced spindle power consumption during shoulder milling.
- Tolerance class K ensures uniform height of all inserts in the milling head and lower surface roughness.
- The 0.8 mm corner radius rε combines cutting edge strength with a good machined surface finish.
- The 90° entering angle allows a vertical shoulder and a flat workpiece floor to be milled in one tool pass.
Applications and cutting data selection for the shoulder milling insert
This indexable insert performs well in milling heads and indexable milling cutters for peripheral milling, shoulder facing, and roughing and finishing surfaces in structural, alloy, and stainless steels. Calculate spindle speed using n = 1000·Vc/(π·D). For a milling head with a diameter of 50 mm at a cutting speed of 160 m/min, the result is approximately 1019 rpm. Calculate feed rate as vf = fz·z·n; with five cutting edges and a feed per tooth of fz 0.15 mm, this gives approximately 764 millimeters per minute. These settings maintain a stable edge load and consistent chip evacuation.
For stainless steel, maintain a cutting speed of 70-130 m/min and a constant feed to limit work hardening of the layer being cut. Select depth of cut ap according to system rigidity and machine power: for shoulder milling, typically 1-4 mm in steel and 0.5-2 mm in stainless materials. Grade H6310 inserts are supplied by the Korean brand Horn. Use a generous flow of emulsion or compressed air for cooling to remove chips from the cutting zone and protect the coating from overheating.
▲
Application limitation
Grade H6310 is not intended for hardened steels above 45 HRC — for harder materials, select an insert in grade H8320 or a milling head with a cubic boron nitride (CBN) cutting edge.
Parallelogram insert designation decoder according to ISO 1832
how to read the APKT 1604 PDER code — positions 1–10 of the designation
Designation APKT 1604 PDER according to the standard ISO 1832: 4 letters describe the geometry and construction, 2 numeric codes describe the dimensions, and the suffix PDER — the wiper edge geometry. Each field has a number, an icon and a brief description.
ISO 1832 designation decoder — how to read the code
1Ashape 2Pangle α 3Ktolerance 4Ttype – 516edge length 604thickness – 7Pangle κ 8Dland α′ 9Eedge 10Rhand
Positions 1–3 · ISO code
1AShape
Parallelogram 85°
2 corners of 85° per side
2PClearance angle
α = 11°
positive, single-sided
3KTolerance
Class K (precision)
ground thickness ±0.025 mm
Positions 4–6
4TType
Countersunk hole + chip breaker
countersink 40–60°, single-sided chip breaker
516Edge length
l = 16 mm
code 16 → edge length
604Thickness
s = 4.76 mm
between rake faces
PDER suffix · wiper edge
7PEntering angle
κ = 90°
90° angle milling cutters and milling heads
8DWiper land
α′ = 15°
wiper land clearance angle
9EEdge condition
Rounded (honed)
greater resistance to chipping
10RHand
Right-hand
standard clockwise spindle rotation
✓ 2 corners × 1 side = 2 cutting edges
Full designation: APKT 1604 PDER = parallelogram 85° · positive 11° · class K · countersunk hole and chip breaker · l 16 mm · s 4.76 mm · κ 90° · wiper chamfer 15° · rounded edge · right-hand (R)
Compatible 90° milling heads and indexable milling cutters
ST90 milling cutters and TK90 milling heads confirmed for this insert
ST90 AP16 D25 W25 L120 Z02⌀25 mm | 2 cutting edges | L120 mm | Weldon ⌀25
⌀25
ST90 AP16 D32 W25 L120 Z03⌀32 mm | 3 cutting edges | L120 mm | Weldon ⌀25
⌀32
ST90 AP16 D32 W32 L120 Z03⌀32 mm | 3 cutting edges | L120 mm | Weldon ⌀32
⌀32
ST90 AP16 D40 W32 L120 Z04⌀40 mm | 4 cutting edges | L120 mm | Weldon ⌀32
⌀40
ST90 AP16 D25 W25 L150 Z02⌀25 mm | 2 cutting edges | L150 mm | Weldon ⌀25
⌀25
ST90 AP16 D32 W32 L150 Z03⌀32 mm | 3 cutting edges | L150 mm | Weldon ⌀32
⌀32
ST90 AP16 D35 W32 L150 Z03⌀35 mm | 3 cutting edges | L150 mm | Weldon ⌀32
⌀35
ST90 AP16 D40 W32 L150 Z04⌀40 mm | 4 cutting edges | L150 mm | Weldon ⌀32
⌀40
ST90 AP16 D25 C25 L200 Z02⌀25 mm | 2 cutting edges | L200 mm | Straight shank ⌀25
⌀25
ST90 AP16 D32 C32 L200 Z03⌀32 mm | 3 cutting edges | L200 mm | Straight shank ⌀32
⌀32
ST90 AP16 D35 C32 L200 Z03⌀35 mm | 3 cutting edges | L200 mm | Straight shank ⌀32
⌀35
ST90 AP16 D40 C32 L200 Z04⌀40 mm | 4 cutting edges | L200 mm | Straight shank ⌀32
⌀40
TK90 AP16 D40 A16 Z04-H⌀40 mm | 4 cutting edges | 90° | mounting ⌀16
⌀4090°
TK90 AP16 D50 A22 Z05-H⌀50 mm | 5 cutting edges | 90° | mounting ⌀22
⌀5090°
TK90 AP16 D63 A22 Z06-H⌀63 mm | 6 cutting edges | 90° | mounting ⌀22
⌀6390°
TK90 AP16 D80 A27 Z07-H⌀80 mm | 7 cutting edges | 90° | mounting ⌀27
⌀8090°
TK90 AP16 D100 A32 Z08-H⌀100 mm | 8 cutting edges | 90° | mounting ⌀32
⌀10090°
TK90 AP16 D125 B40 Z09⌀125 mm | 9 cutting edges | 90° | mounting ⌀40
⌀12590°
TK90 AP16 D160 C40 Z10⌀160 mm | 10 cutting edges | 90° | mounting ⌀40
⌀16090°
TK90 AP16 D200 B60 Z12⌀200 mm | 12 cutting edges | 90° | mounting ⌀60
⌀20090°
Frequently asked questions about the APKT 160408 insert
number of edges, milling head selection, and cutting data
Two — the 85° rectangle has 2 working corners, and the positive geometry with a 11° clearance angle makes the insert single-sided, cutting only with its top face. Once a corner becomes dull, rotate the insert in the milling head pocket to the second edge without changing the tool.
It fits end mills ST90 AP16 with diameters of 25–40 mm and shell milling heads TK90 AP16 with diameters of 40–200 mm and 4 to 12 cutting edges — the tool bodies listed in the compatibility table above. For other tools, compare the pocket designation and size with the manufacturer's data.
Only in tolerance class. APKT has class K with thickness and height ground to ±0.025 mm, so all inserts in the milling head sit at the same height — lower roughness when finishing. APMT has class M (±0.05–0.13 mm), which is less expensive and sufficient for rough milling.
Yes — grade H6310 covers group ISO M20-M40. Maintain a cutting speed of 70–130 m/min, a constant feed, and continuous cooling: austenitic steel dissipates heat poorly and work-hardens when cutting is too slow.
Product accessories

Milling head TK90 AP16 D80 A27 Z07-H Smoxh
Reference: 05321 In stock < 10 items
€92.11
€113.29 brutto
Milling head TK90 AP16 D100 A32 Z-08 Smoxh
Reference: 53252 In stock < 10 items
€102.63
€126.24 brutto
End mill ST90-AP16-D25-W25-L150-Z02 Smoxh
Reference: 10897 In stock < 10 items
€60.53
€74.45 brutto
Milling head TK90 AP16 D63 A22 Z-06 H Smoxh
Reference: 05320 In stock < 10 items
€76.32
€93.87 brutto

Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you





This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.