







Description
| Technical Data | |
|---|---|
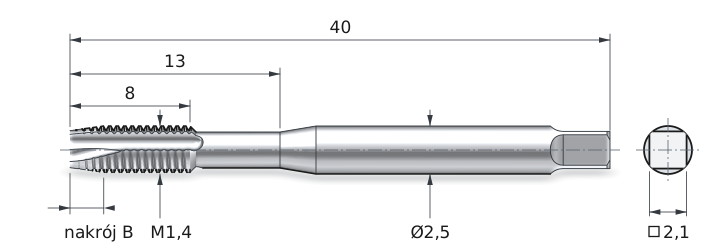
| Nominal Diameter d1 | M1.4 |
| Thread Pitch P | 0.3 mm |
| Overall Length l1 | 40 mm |
| Flute Length l2 | 8 mm |
| Length l3 | 13 mm |
| Shank Diameter d2 | 2.5 mm |
| Square Drive Size a | 2.1 mm |
| Tap Drill Diameter | 1.1 mm |
| Chamfer | B (3.5÷5.5) P |
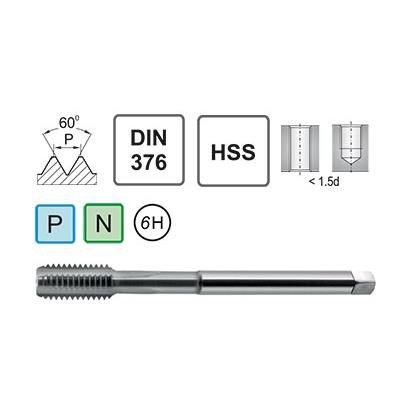
| Thread tolerance | 6H |
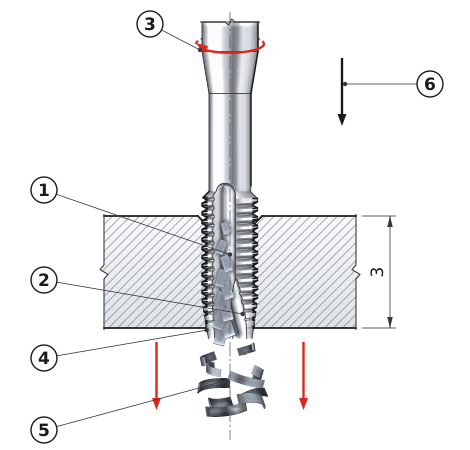
Chips exit at the bottom instead of returning through the thread
The form B through-hole chamfer has a chip breaker at the front of the tap – an angled cut in the cutting edges. The chip breaker directs chips down the hole, ahead of the tap tip. The chip curls into a coil, breaks into short pieces, and exits the hole on the other side of the workpiece. Threads already cut remain clean because chips do not pass through them on their way up. The M1.4 x0.3 tap has a reinforced shank in accordance with DIN 371: diameter 2.5 mm, square 2.1 mm.
The M1.4 machine tap for through holes from the Werko series is designed for precision machining and maintenance in manufacturing plants. HSS high-speed steel construction with a hardness of 62-65 HRC guarantees long cutting edge life when tapping materials with a tensile strength up to 800 MPa. Type B straight-flute geometry directs chips forward, which is essential when tapping miniature through holes. The tool meets DIN 371 requirements and provides the 6H thread tolerance class required in the production of electronic components and precision mechanisms.
The M1.4 machine tap for through holes is suitable for maintenance departments performing thread restoration and repairs on electronic equipment and precision mechanisms. It is also used by industrial service providers and workshops repairing measuring equipment. Form B with straight flutes directs chips forward, eliminating the risk of jamming in miniature through holes.
| Material | Cutting speed Vc [m/min] | Spindle speed n [rpm] | Feed f [mm/min] |
|---|---|---|---|
| PSteel | 5-20 | 1137-4547 | 341-1364 |
| MStainless steel | 5-10 | 1137-2274 | 341-682 |
| KCast iron | 5-15 | 1137-3410 | 341-1023 |
| NAluminum | 10-25 | 2274-5684 | 682-1705 |
NC spotting drill 90°
Ø 1.1 mm
M1.4
Tolerance 6H
Standard: DIN 371 | Chamfer: B (straight) | Application: through holes
| Class | Accuracy | Application | Status |
|---|---|---|---|
| 4H / 4g | High | Precision connections, hydraulics | — |
| 6H / 6g | Standard | Machine building, general-purpose | SELECTED |
| 7H / 8g | Low | Large clearance, easy assembly | — |
6H = internal thread (nut, hole) | 6g = external thread (screw)
The recommended tap drill diameter for the M1.4 thread is 1.1 mm. At such small diameters, hole accuracy is critical — use high-precision drill bits and rigid workpiece clamping.
When tapping aluminum and brass, cooling with a 5-8% emulsion extends tool life and improves thread quality. Plastics can be machined dry or with minimum lubrication to avoid contaminating the material.
The M1.4 DIN 371 form B tap is designed exclusively for through holes. Straight flutes direct chips forward — in blind holes, chips would jam and damage the tool or thread.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


