






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot
Description
Angle to the axis45 degrees
Diameter range10–31 mm
Inserts2 × TCMT 16T304
Length100 mm
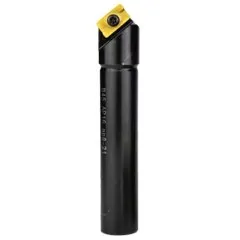
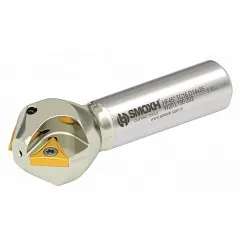
Indexable countersink 10x31 mm – 45° chamfer mill for TCMT inserts
Technical data for the 10x31 mm 45° indexable countersink – 20 mm Weldon shank
| Technical data | |
|---|---|
| Cutting edge angle to the axis | 45° (90° cone) |
| Minimum diameter D2 | 10 mm |
| Maximum diameter D1 | 31 mm |
| Max. cutting depth | 10.5 mm |
| Flute length l | 35 mm |
| Overall length L | 100 mm |
| Shank diameter d | 20 mm, Weldon |
| Number of inserts Z | 2 |
| Insert | TCMT 16T3 (e.g., 16T304) |
| Manufacturer | Smoxh, Turkey (HF45 TC16 D10-31) |
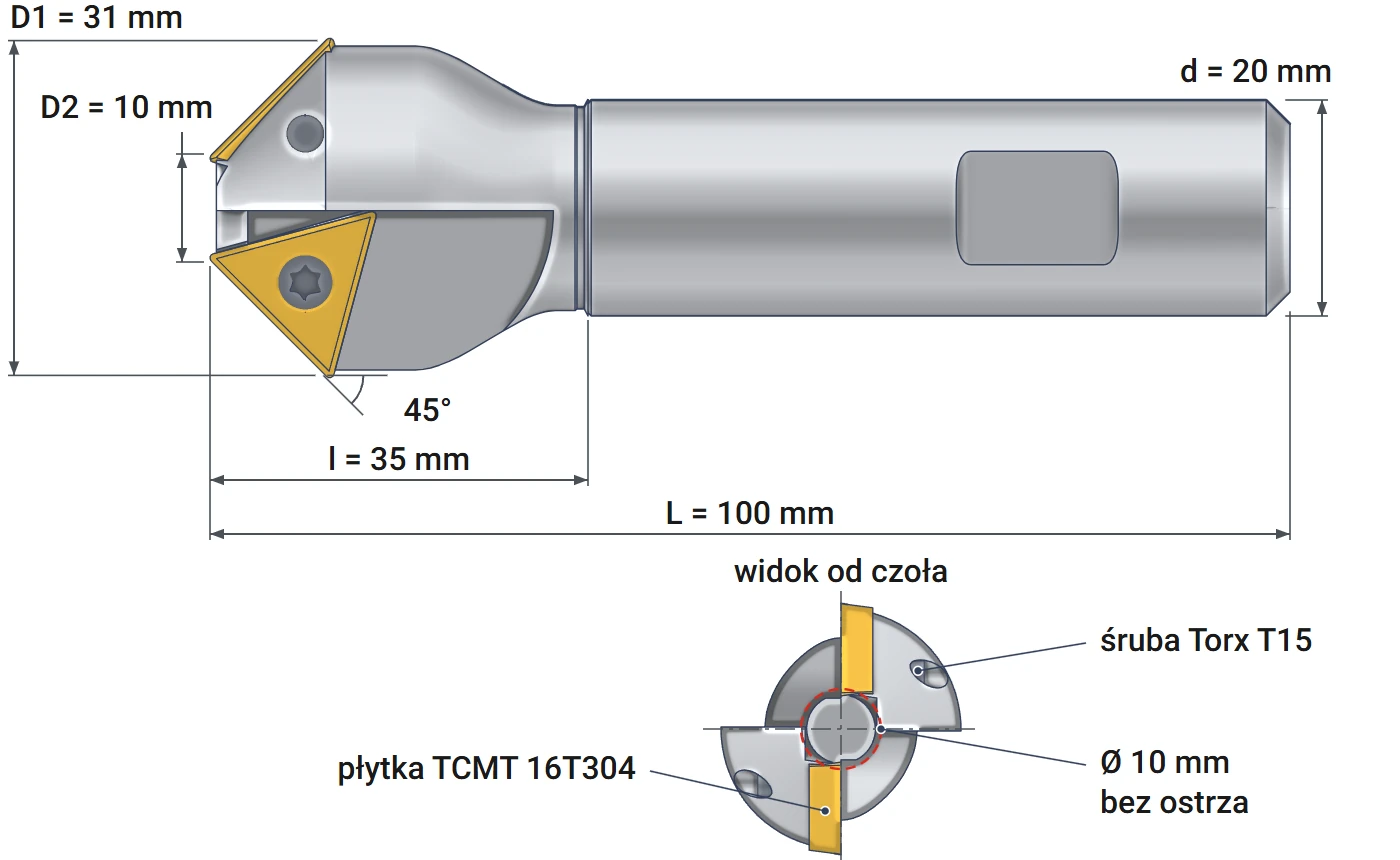
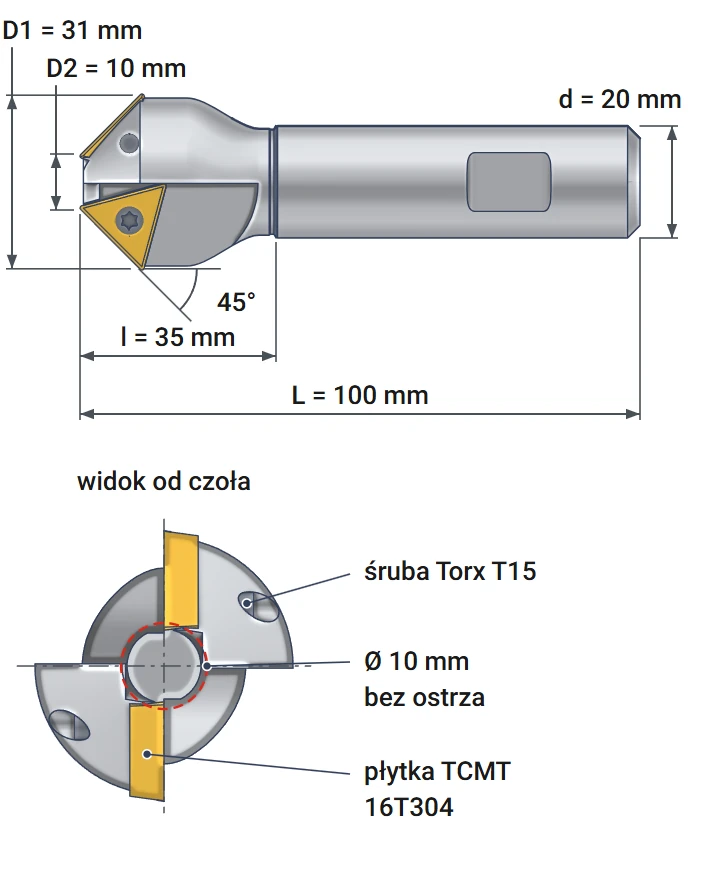
Indexable countersink 10x31 mm by Smoxh countersinks seats for flat-head screws and chamfers edges. It cuts with two TCMT 16T304 inserts over diameters from 10 to 31 mm. Each insert has three cutting edges. A dull edge is replaced by rotating the insert by 120°, without resharpening the tool.
The 45° angle is measured between the insert cutting edge and the tool axis. The rotating inserts therefore sweep out a 90° cone. This is the head angle of a metric flat-head screw. Each of the two inserts covers the full diameter range, so they share the feed per revolution and each removes half the chip. The 20 mm shank has a Weldon flat for the holder screw, which locks the tool in the holder.
Applications – countersunk screw seat and slot chamfers
Operations with the 45° countersink
The countersink also works as a 45° chamfer mill. The same insert edges cut in every operation. Only the toolpath and depth of engagement change. The countersink machines holes and slots wider than 10 mm.
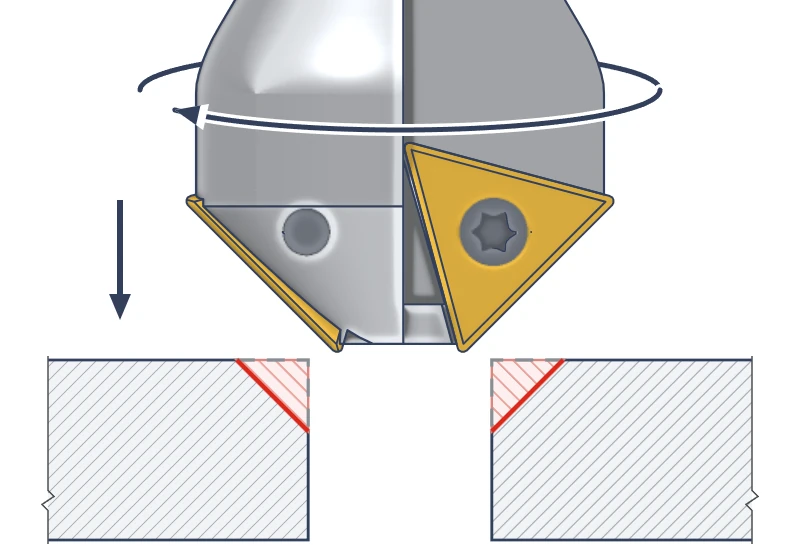
Countersunk screw seat
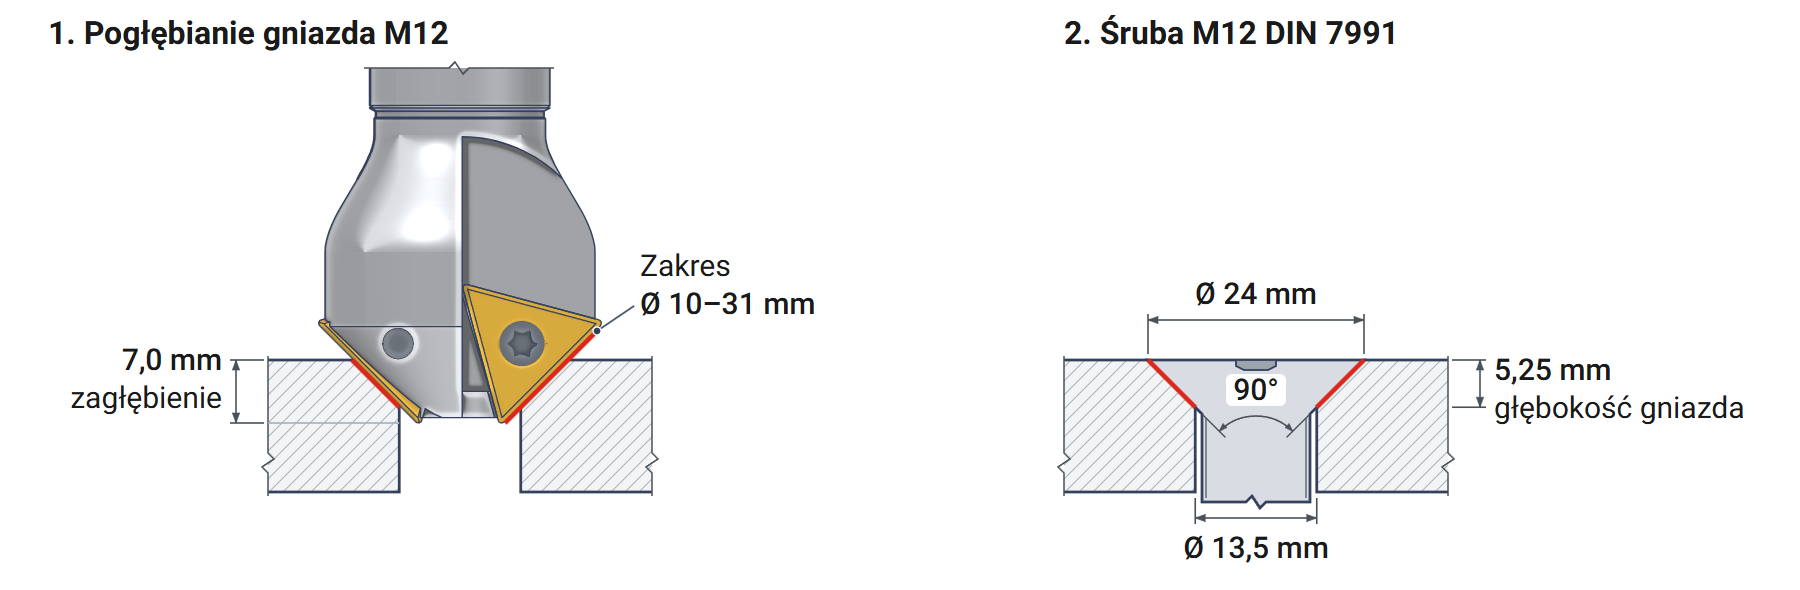
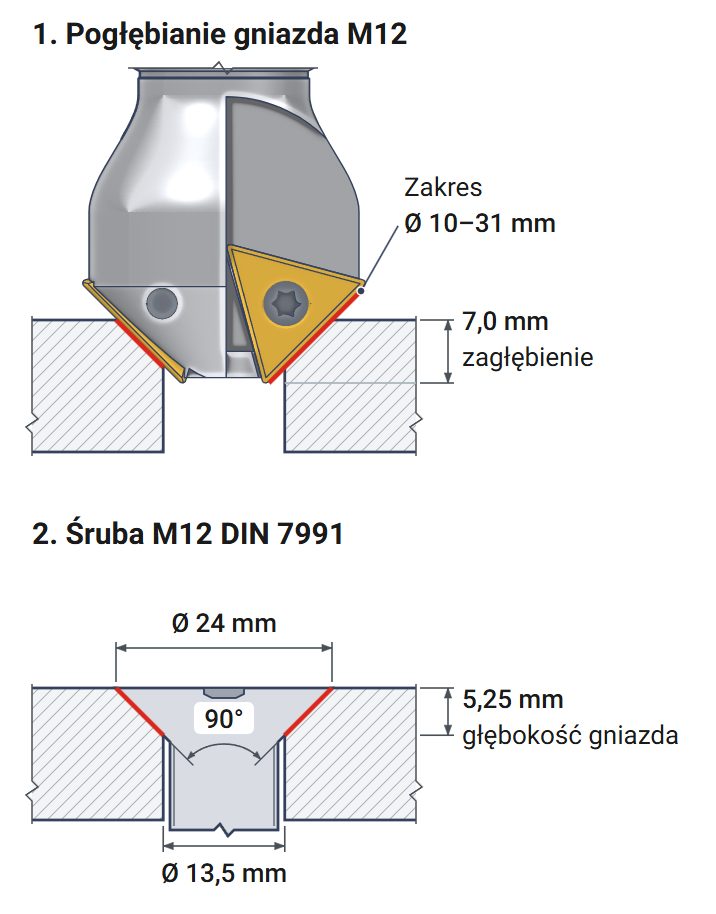
The inserts sweep a 90° cone, matching the screw head specified in DIN 7991. The countersink feeds axially into the clearance hole to the calculated depth. It accommodates M10, M12, and M16 heads with diameters of 20, 24, and 30 mm. The head sits flush with the workpiece surface or 0.1 mm below it.
Chamfer on both slot edges
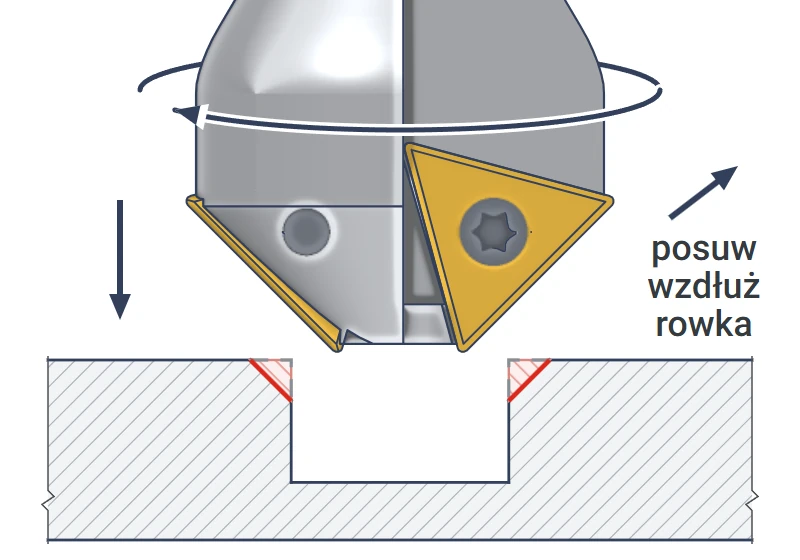
The tool is guided along the center of a slot wider than 10 mm. The inserts chamfer both upper edges in a single pass. Chamfer width is set by the plunge depth. This method is used to chamfer keyway and guideway edges.
Screw head recess – selection and depth
Which screws fit and how deep to plunge
The countersink cuts from 10 mm to 31 mm in diameter. A complete recess requires two conditions. The clearance hole must be larger than 10 mm. The screw head must be less than 31 mm in diameter.
Calculator: Z-axis plunge depth for recess diameter
With a 90° cone, each millimeter of downward travel adds 2 mm to the diameter. Plunge depth is measured from the workpiece surface to the insert corners at a diameter of 10 mm. Plunge depth = (recess diameter − 10 mm) ÷ 2, e.g., (24 − 10) ÷ 2 = 7 mm for an M12 head.
▲
Clearance hole wider than 10 mm
The countersink cuts from a diameter of 10 mm. In a clearance hole wider than 10 mm, e.g., 11 mm for M10, the recess is complete and the head seats fully.
TCMT 16T304 inserts – three edges and indexing
Triangular insert to ISO 1832, Torx T15 screw
The insert designation is interpreted according to ISO 1832. T indicates a triangle, so the insert has three cutting edges. C indicates a 7° clearance angle: the insert has positive geometry and cuts freely. M is the medium tolerance class, the most common for these inserts. The next T indicates a countersunk screw hole and a chip breaker on one side – a profile that curls and breaks the chip. 16 indicates an edge of approx. 16.5 mm, T3 a thickness of 3.97 mm, and 04 a corner radius of 0.4 mm.
The insert's 60° angle does not determine the recess angle. The 90° cone results from the insert's orientation in the body. The store offers the TCMT 16T304 H6310 insert from the Korean brand Horn. Grade H6310 is a general-purpose grade for steel and stainless steel. The countersink is sold without inserts.
Changing edges step by step
1Loosening the screw
Key: Torx T15
2Indexing the insert
Rotation: 120°
3Cleaning the insert seat
Chips: removed
4Tightening the screw
Torque: 2.7 N·m
✓Second insert
Repeat: steps 1–4
M3.5x10 screw and T15 key according to the Smoxh catalog
Both inserts are indexed at the same time because they cut on the same cone. A chip under an insert shifts its cutting edge and changes the recess diameter, so the insert seat must be cleaned before each installation.
Cutting data – starting values
Cutting speed and feed per tooth – conservative ranges
The conservative ranges for material groups P, M, and K according to ISO 513 are based on milling with a 45° entering angle. The entering angle is the angle between the insert edge and the machined surface. Start at the lower limit and increase the values while monitoring the chips and spindle sound.
| Workpiece material | Cutting speed vc [m/min] | Feed per tooth fz [mm] |
|---|---|---|
| P Structural and alloy steel | 150–220 | 0.10–0.22 |
| M Stainless steel | 80–140 | 0.08–0.18 |
| K Gray cast iron | 180–300 | 0.10–0.28 |
Calculating spindle speed and feed rate – M12 recess in steel
Spindle speed is calculated for the largest diameter engaged in the material, here the 24 mm head. Spindle speed = 1000 × cutting speed 150 m/min ÷ (3.14 × diameter 24 mm) ≈ 1980 rpm. Feed rate = feed per tooth 0.10 mm × 2 inserts × 1980 rpm ≈ 390 mm/min. These two values are entered in the machine tool program.
When machining stainless steel, coolant protects the hole edge from overheating.
Indexable countersink 10x31 mm Smoxh cuts 90° recesses for M10, M12, and M16 heads. It also chamfers holes from 10 mm, external edges, and slots. The tool requires a set of 2 TCMT 16T304 inserts. The 20 mm Weldon shank and 100 mm length fit standard milling tool holders.
Questions about the recess, inserts, and CNC setup
DIN 7991 screws, TCMT inserts, Z-axis plunge depth
For 90° countersunk screws to DIN 7991: M10, M12, and M16. Their head diameters are 20, 24, and 30 mm, and their clearance hole diameters are 11, 13.5, and 17.5 mm. The calculator above gives the plunge depth for each of these screws.
TCMT 16T3 inserts to ISO, e.g., TCMT 16T304 with a 0.4 mm corner radius. The store offers TCMT 16T304 H6310 Horn for steel and stainless steel. The insert is secured with an M3.5x10 screw with a Torx T15 socket.
Two TCMT 16T304 inserts, one in each seat. Each insert has three edges. A set of two inserts provides three usable edge positions: the first and two more after indexing by 120°.
Enter a 90° countersink with a tip diameter of 10 mm in the tool table. Measure the tool height to the insert corners. Plunge depth = (head diameter − 10 mm) ÷ 2, plus approx. 0.1 mm.
Product accessories


Carbide insert TCMT 16T308 H6310 Horn
Reference: 0000006146 In stock > 10 items
€3.68
€4.53 brutto
Carbide insert TCMT 16T304 H6310 Horn
Reference: 0000007829 In stock > 10 items
€3.68
€4.53 brutto


Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you





This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.