







Net price: €7.63
Description
| Technical data | |
|---|---|
| Side length l | 5 mm |
| Insert thickness s | 3.18 mm |
| Hole diameter d1 | 3.2 mm |
| Corner radius rε | 0.80 mm |
| Shape | W – 80° trigon |
| Number of edges | 3 |
| Type | X – drilling type |
| Grade | PH 6920 (CVD) |
central and peripheral inserts and ISO groups P, M, and K
An indexable drill uses two inserts — peripheral and central — and each position requires a different carbide grade. This division results from the distribution of cutting speed along the radius: speed approaches zero at the axis of rotation and reaches its maximum at the periphery. CVD-coated grades, such as PH 6920, are intended for the peripheral position, which determines hole diameter and quality. For the center, where the insert displaces material at low speed and under high axial forces, the body manufacturer selects a separate, tougher grade. Do not interchange inserts between positions, even if their ISO shapes are identical.
drilling steel, stainless steel, and cast iron with an indexable drill
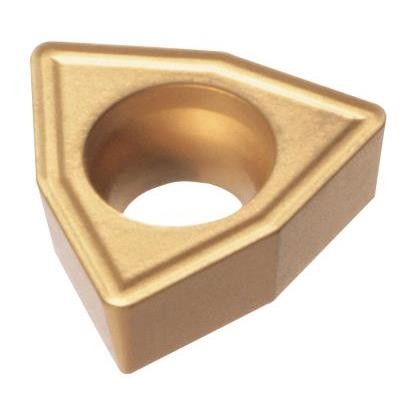
The WCMX 050308 carbide insert is an indexable insert for indexable drills in Palbit grade PH 6920. Shape W, a trigon with a 80° corner angle, and type X indicate a special design; confirm the presence and side of the chip breaker in the product data sheet. The insert is mounted in a compatible pocket in the steel drill body, allowing only the cutting edge to be replaced without replacing the entire tool. Grade PH 6920, coated by CVD (chemical vapor deposition), covers steel, stainless steel, and cast iron.
The insert is suitable for drilling holes in structural steel, stainless steels, and cast iron on CNC and conventional machine tools. Parameters are selected based on the nominal drill diameter and body specifications. For an example Ø30 mm drill, an overhang range of 4D–5D corresponds to a depth of 4·30 = 120 mm to 5·30 = 150 mm. Refer to the data sheet for the specific body for cutting speed and feed.
Grade PH 6920 offers strength under severe cutting conditions and resistance to abrasive wear at high temperatures. Heat resistance reaching 700–1000°C protects the carbide coating during long passes. Increased edge security supports drilling under unstable conditions, such as interrupted stock. Select the hole depth to match the body length, expressed as a multiple of the diameter (xD).
At a hole depth approaching 4×D–5×D internal coolant through the body channels (IK) is practically mandatory. Without flushing chips out of the flute, torque increases, creating a risk of clogging and insert or body breakage.
how to read the WCMX 050308 code — designation positions 1–7
Designation WCMX 050308 according to the standard ISO 1832: 4 letters describe geometry and construction, 3 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
ISO 1832 designation decoder — how to read the code
Positions 1–4 · ISO code
1WShape
80° trigon
3 corners of 80° per side
2CClearance angle
α = 7°
positive, single-sided
3MTolerance
Class M (intermediate)
IC ±0.05–0.15 · thickness ±0.13 mm
4XType
Manufacturer-specific special type
features outside the ISO 1832 code
Positions 5–7 · dimensions [mm]
505Edge length
l = 5 mm
code 05 → edge length
603Thickness
s = 3.18 mm
between rake faces
708Corner radius
rε = 0.8 mm
code ÷ 10 → radius in mm
✓ 3 corners × 1 side = 3 cutting edges
materials and tools compatible with the drilling insert
| Rating | Application |
|---|---|
| ✓ | Drilling structural steel — ISO group P |
| ✓ | Drilling stainless steel — ISO group M |
| ✓ | Drilling cast iron — ISO group K |
| ✓ | Indexable drills with a pocket for shape W (type X) |
| ✓ | CNC and conventional machine tools |
| ✗ | Turning and boring — this is a drilling insert, not a turning insert |
| ✗ | Operation without the central + peripheral insert set recommended for the body |
applications, grade PH 6920, and operation in an indexable drill
For indexable drills whose steel body has two pockets for replaceable inserts — central and peripheral. The insert is mounted in a compatible pocket, so after wear you replace only the cutting edge without replacing the body. The code WCMX describes shape W (80° trigon) and drilling type X.
Grade PH 6920 from Palbit is a CVD-coated carbide suitable for universal use in steel (ISO P), stainless steel (ISO M) and cast iron (ISO K). It retains abrasive wear resistance at cutting temperatures reaching 700–1000°C.
The central insert operates at a cutting speed from zero to approximately 50% vc max and displaces material at the drill axis. The peripheral insert operates from 50% to 100% vc max and determines hole diameter and surface quality. CVD grades, such as PH 6920, are used in the peripheral position; a separate, tougher grade is selected for the center.
No — the self-centering geometry of the two inserts guides the drill without spot drilling, despite the long overhang. At a depth of 4×D–5×D however, use internal coolant to flush chips out of the flute and prevent insert breakage.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


