







Description
| Technical data | |
|---|---|
| Side length l | 9.80 mm |
| Insert thickness s | 4.76 mm |
| Corner radius rε | 0.80 mm |
| ANSI code | SPMG 332 |
| Shape | square (S) |
| Carbide grade | H6310 (PVD) |
| Application | indexable drills |
conservative cutting speeds and feeds for steel and stainless steel
| ISO group / material | Vc [m/min] | Feed f [mm/rev] |
|---|---|---|
| PSteel | 50-75 | 0.15-0.40 |
| MStainless steel | 35-50 | 0.10-0.22 |
square drilling insert for holemaking on CNC machine tools
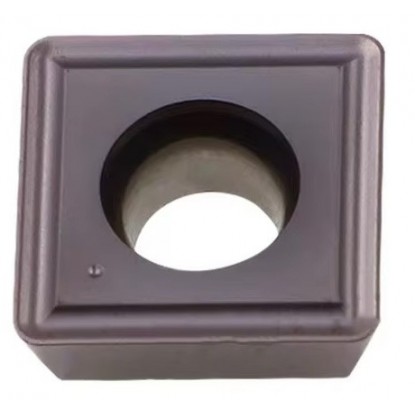
The SPMG 090408 carbide insert is a square indexable insert designed for indexable drills, tools with replaceable cutting edges for drilling holes on CNC machine tools. The documentation for the specific tool defines the position of the SPMG insert in the drill body — central or peripheral — as well as its grade and chip breaker geometry. The insert for indexable drills is made of grade H6310 cemented carbide with a PVD coating, applied by physical vapor deposition. This grade is designed for group P steel and group M stainless steel. The square profile with four corners and a corner radius of 0.8 mm provides strong cutting edges for heavy-duty, interrupted cutting conditions.
In an indexable drill, the central position operates at approximately 0–50% of the maximum cutting speed, and the peripheral position at approximately 50–100%; the body data sheet specifies the position of this insert. Calculate spindle speed using the formula n = 1000·Vc/(π·D), where D is the body diameter and Vc is selected from the reference range for the workpiece material. For D = 20 mm and Vc = 60 m/min: n = 1000·60/(π·20) ≈ 955 rpm. Select the feed according to the table and the body manufacturer's recommendations to avoid overloading the cutting edge.
When drilling group M stainless steel, maintain a constant feed and continuous cooling with coolant supplied through the holder to the cutting zone. Stainless steel can work-harden during machining, so avoid interruptions in feed. Reduce the feed as the drill enters and exits the material to limit corner chipping. An indexable drill requires rigid mounting of the body and spindle, as play causes vibration and reduces insert life. For holes with tighter tolerances, allow for reaming, since a typical indexable drill usually achieves tolerance grades H10–H12 (IT10–IT12).
Grade H6310 is not intended for steels hardened above 45 HRC. Inserts are not included with the drill — select them to fit the pocket of the specific body. For holes with tighter tolerances, allow for reaming, since a typical indexable drill achieves a tolerance grade of H10–H12 (IT10–IT12).
how to read the SPMG 090408 code — positions 1–7 of the designation
Designation SPMG 090408 according to the standard ISO 1832: 4 letters describe geometry and construction, 3 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
ISO 1832 designation decoder — how to read the code
Positions 1–4 · ISO code
1SShape
Square 90°
4 corners of 90° per side
2PClearance angle
α = 11°
positive, single-sided
3MTolerance
Class M (intermediate)
IC ±0.08 · thickness ±0.13 mm
4GType
Hole + chip breaker
chip breaker on both sides
Positions 5–7 · dimensions [mm]
509Size
l = 9.8 mm
IC = 9.8 mm (square: IC = l)
604Thickness
s = 4.76 mm
between rake faces
708Corner radius
rε = 0.8 mm
code ÷ 10 → radius in mm
✓ 4 corners × 1 side = 4 cutting edges
where the insert fits and where it should not be used
Applications and limitations
| Rating | Application |
|---|---|
| ✔ | Indexable drill bodies with a pocket for the insert SPMG 09 — position as specified in the body data sheet |
| ✔ | Drilling on CNC machine tools using a body with a suitable pocket for the SPMG 09 insert |
| ✔ | Steel (group P) and stainless steel (group M) |
| ✗ | Hardened steels above 45 HRC — outside the range of grade H6310 |
| ✗ | Solid carbide (VHM) drills and drills with brazed crowns — do not accept replaceable inserts |
| ✗ | Interchanging inserts between different manufacturers' systems without checking the pocket |
tool selection, materials, and drilling parameters
Indexable drills, meaning drills with replaceable inserts, with bodies featuring a pocket for the insert SPMG 09. The body documentation specifies the SPMG position and grade; the same ISO shape may be approved for both positions. Inserts are usually not included with the drill — select them to fit the pocket of the specific body.
Grade H6310 is PVD-coated carbide for steels in group P20-P40 and stainless steel M20-M40. It is not intended for steels hardened above 45 HRC.
The square profile provides 4 corners for use. When a cutting edge becomes dull, rotate the insert in the drill pocket to the next edge without replacing the entire body. The cutting edge dimensions are the side length 9.8 mm, thickness 4.76 mm and corner radius 0.8 mm.
Calculate spindle speed using the formula n = 1000·Vc/(π·D), where D is the body diameter. For steel, select Vc from the range 50-75 m/min and feed f from the range 0.15-0.40 mm/rev; verify the values against the drill documentation.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


