








Net price: €6.97
Description
| Technical data | |
|---|---|
| Side length l | 6.14 mm |
| Insert thickness s | 3.97 mm |
| Hole diameter d1 | 3.7 mm |
| Corner radius rε | 0.80 mm |
| ANSI code | WCMX 32.52 |
| Shape | W — 80° trigon |
| Number of edges | 3 |
| Grade | PHC 6920 (CVD coating) |
grade PHC 6920 (CVD) — ISO groups P, M, K
| Material | Vc [m/min] | Feed f [mm/rev] |
|---|---|---|
| PSteel | 50-75 | 0.15-0.40 |
| MStainless steel | 35-50 | 0.10-0.22 |
| KCast iron | 50-70 | 0.25-0.45 |
80° trigon, drilling design, grade PHC 6920
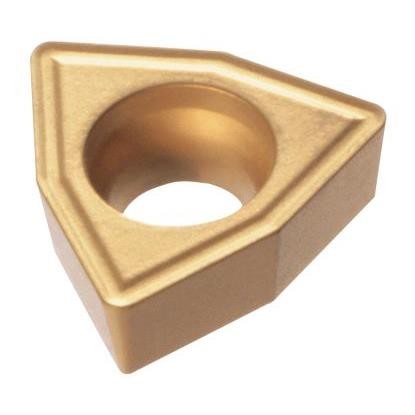
The WCMX 06T308 carbide insert is a replaceable cutting insert for indexable drills, also called U-drills. It is mounted in a pocket in the steel drill body, which replaces several solid carbide drills. A typical indexable drill uses two inserts — central and peripheral — serving as cutting edges on the tool face. Use CVD-coated grade PHC 6920 exclusively in the peripheral position; for the central position, select a tougher PVD grade specified by the drill manufacturer. Shape W denotes a trigon with a 80° corner angle, while the letter X indicates a special design with drilling geometry. The insert is made of cemented carbide in CVD-coated grade PHC 6920, intended for ISO groups P, M, and K; the P20-P45 range applies to machining steel and cast steel. The mounting hole diameter of 3.7 millimeters and corner radius of 0.80 millimeters are selected for operation in a drill body, not a turning tool holder.
The WCMX 06T308 insert for indexable drills is suitable for drilling holes in structural steel, cast steel, stainless steel, and cast iron. Calculate drill rotational speed using the formula n = 1000·Vc/(π·D). For a drill with a diameter of 30 millimeters and a cutting speed of Vc = 60 meters per minute, the result is approximately 636 rpm. Select feed for the material group from the cutting data table, maintaining steady tool movement for consistent chip breaking. Drill on a machine with stable guidance, without stopping the feed while the tool is in the material.
The center and peripheral inserts may have the same ISO code, but do not necessarily have the same grade or chip breaker geometry. Use the CVD-coated PHC 6920 variant only as a peripheral insert, and select a tougher PVD grade for the center as specified in the catalog data sheet for the drill system. Drilling depth is standardized as a multiple of diameter, and a reasonable range for a typical indexable drill extends to about four diameters. The flutes in the body evacuate chips, while the coolant channels deliver cutting fluid directly to the cutting zone, reducing the cutting edge temperature and facilitating chip removal from deep holes.
Insert WCMX 06T308 is a drilling insert — do not use it in a turning tool or milling head. Grade PHC 6920 CVD is intended exclusively for the peripheral position; use a tougher PVD grade specified by the drill manufacturer in the center.
how to read the WCMX 06T308 code — positions 1–7 of the designation
Designation WCMX 06T308 according to the standard ISO 1832: 4 letters describe geometry and construction, 3 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
ISO 1832 designation decoder — how to read the code
Positions 1–4 · ISO code
1WShape
80° trigon
3 corners of 80° per side
2CClearance angle
α = 7°
positive, single-sided
3MTolerance
Class M (intermediate)
IC ±0.05–0.15 · thickness ±0.13 mm
4XType
Manufacturer-specific special type
features outside the ISO 1832 code
Positions 5–7 · dimensions [mm]
506Edge length
l = 6.14 mm
code 06 → edge length
6T3Thickness
s = 3.97 mm
between rake faces
708Corner radius
rε = 0.8 mm
code ÷ 10 → radius in mm
✓ 3 corners × 1 side = 3 cutting edges
where the replaceable insert fits and where it does not
| Application | Compatibility |
|---|---|
| Indexable drills (U-drill) with a pocket for a WCMX 06T308 insert | ✔ yes |
| Peripheral position in the drill body — PHC 6920 CVD grade | ✔ yes |
| Steel, cast steel, stainless steel, cast iron (P/M/K) | ✔ yes |
| Turning tools and milling tool holders | ✗ no |
| Center position in the drill body — for PHC 6920 CVD | ✗ no; select a tougher PVD grade |
installation, drill selection, and drilling parameters
It is a replaceable insert for indexable drills (U-drill), mounted in a pocket in the steel body. Shape W is a trigon with an included corner angle of 80°, and the mounting hole has a diameter of 3.7 mm. The insert is not intended for turning or milling.
Grade PHC 6920 is carbide with a coating of CVD for steel and cast steel in the range P20-P45, and the product sources also confirm stainless steel and cast iron. Use it only in the peripheral position of the drill.
Use the formula n = 1000·Vc/(π·D). For a drill Ø30 mm at a cutting speed of Vc = 60 m/min the result is approximately 636 rpm. A smaller diameter requires a higher rotational speed, while a larger diameter requires a lower speed.
Despite having the same ISO code, they are functionally different inserts. Use PHC 6920 CVD grade only as a peripheral insert; select a tougher PVD grade for the center position as specified in the drill system catalog data sheet.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


