







Description
| Technical data | |
|---|---|
| Side length l | 5.0 mm |
| Insert thickness s | 3.18 mm |
| Hole diameter d1 | 3.2 mm |
| Corner radius rε | 0.80 mm |
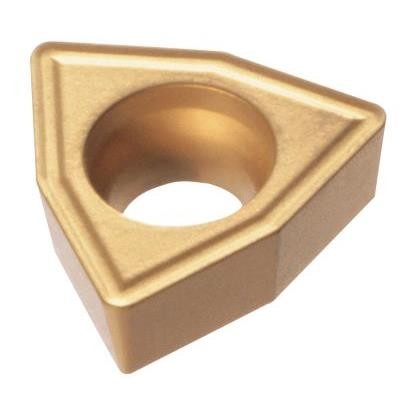
| Shape / type | W – trigon 80° / X |
| Grade | H6310 (PVD) |
reference values for grade H6310 — ISO groups P and M
| Material | Vc [m/min] | Feed f [mm/rev] |
|---|---|---|
| PSteel | 50-75 | 0.15-0.40 |
| MStainless steel | 35-50 | 0.10-0.22 |
80° trigon for indexable drills; position according to body documentation
The WCMX 050308 carbide insert is an indexable insert for indexable drills in grade H6310 from the Korean brand Horn. The W trigon shape with a 80° corner angle and type X design make it suitable for screw mounting in an indexable drill pocket. Cemented carbide with a coating applied by physical vapor deposition (PVD) combines a hard, wear-resistant surface with a tough core. This grade is designed for group P steel and group M stainless steel. Successive trigon corners are indexed by rotating the insert in its pocket after the cutting edge wears out. The 3.2 mm diameter hole guides the retaining screw, and the 0.80 mm corner radius strengthens the edge under axial feed.
The drilling insert is suitable for drilling into solid structural steel and stainless steel. Calculate spindle speed using the formula n = 1000·vc/(π·D), where D is the drill diameter and vc is selected from the table for the workpiece material group. For stainless steel, maintain a constant feed f and a lower cutting speed to limit work hardening.
In an indexable drill, the central position operates at approximately 0–50% of the maximum cutting speed, while the peripheral position operates at approximately 50–100% and affects hole diameter and quality. The body documentation specifies which position a particular WCMX variant occupies and its grade or chip breaker; the same ISO shape may be approved for both positions. Do not swap positions without confirmation in the body data sheet. The inserts are supplied by the Korean brand Horn. For deeper holes, coolant supplied through channels in the body flushes out chips and protects the cutting edges from overload.
Grade H6310 covers steel (ISO P20-P40) and stainless steel (M20-M40) — it is not intended for hardened steels in group ISO H. If the body has coolant channels, direct coolant to the cutting zone to facilitate chip evacuation.
how to read the WCMT 050308 code — positions 1–7 of the designation
Designation WCMT 050308 according to the standard ISO 1832: 4 letters describe geometry and construction, 3 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
ISO 1832 designation decoder — how to read the code
Positions 1–4 · ISO code
1WShape
80° trigon
3 corners of 80° per side
2CClearance angle
α = 7°
positive, single-sided
3MTolerance
Class M (intermediate)
IC ±0.05–0.15 · thickness ±0.13 mm
4TType
Countersunk hole + chip breaker
countersink 40–60°, single-sided chip breaker
Positions 5–7 · dimensions [mm]
505Edge length
l = 5 mm
code 05 → edge length
603Thickness
s = 3.18 mm
between rake faces
708Corner radius
rε = 0.8 mm
code ÷ 10 → radius in mm
✓ 3 corners × 1 side = 3 cutting edges
indexable drills — screw mounting, selection according to the body data sheet
| Rating | Compatibility |
|---|---|
| ✔ | Indexable drills with a pocket for the insert WCMX 05 03 08, secured with a screw |
| ✔ | Compatibility with a specific body, including the system Sandvik CoroDrill 880, must be confirmed in its data sheet; CoroDrill 870 is an exchangeable-head system and does not confirm compatibility with this insert |
| ✔ | Position central or peripheral, grade and chip breaker of the WCMX insert as specified in the data sheet for the body |
| ✗ | Holders and turning tools — WCMX is a drilling insert, not a turning insert |
| ✗ | Installation in an arbitrary body without checking pocket dimensions and geometry |
| ✗ | Hardened steels (group ISO H) — outside the range of grade H6310 |
drill selection, workpiece materials, and ISO designation
For indexable drills, in which a fixed body has two pockets and the inserts are secured with screws. The ISO code WCMX is used in systems including Sandvik CoroDrill 880, but confirm the compatibility of this variant and its position in the body data sheet. CoroDrill 870 is an exchangeable-head system, so it does not confirm compatibility with this insert.
PVD-coated carbide in grade H6310 covers steels in groups ISO P20-P40 and stainless steel M20-M40. Select cutting speed and feed from the table for the workpiece material. The grade does not cover hardened steels in group ISO H.
The complete code specifies the insert family, size, and geometry. When ordering, match the exact designation in the product name and check it against the drill body documentation; a similar shape does not guarantee pocket compatibility.
If the drill body has coolant channels, supply coolant to the cutting zone. It facilitates chip evacuation from the flutes and limits cutting edge overload; select cooling conditions to suit the material and the body manufacturer's recommendations.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


