





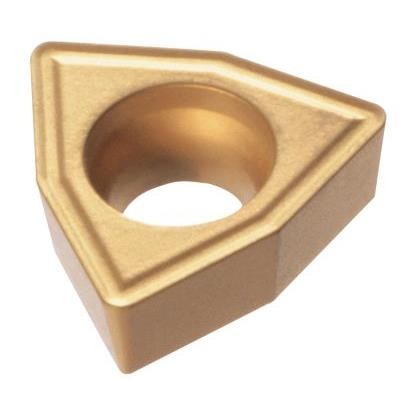

Description
| Technical data | |
|---|---|
| Side length l | 3.47 mm |
| Insert thickness s | 2.38 mm |
| Hole diameter d1 | 2.8 mm |
| Corner radius rε | 0.80 mm |
| Shape | trigon 80° (W) |
| Grade | H6310 (PVD) |
center and peripheral inserts, cutting speed selection and cooling
An indexable drill uses two inserts seated in the body: a center insert near the axis and a peripheral insert at the outside diameter. The two inserts share the work and wear through different mechanisms, so they are selected separately. Read the cutting data from the catalog data sheet for the specific body rather than a universal table.
type W trigon insert for indexable drills in steel and stainless steel
The WCMX 030208 carbide insert is a type W trigon indexable insert with an eighty° corner angle, designed for indexable drills. The letter X in the designation indicates a special design with drilling geometry, while tolerance class M ensures repeatable seating in the body pocket. Grade H6310 is cemented carbide with a PVD coating (applied by physical vapor deposition), suitable for general use in steel and stainless steel. The indexable drill insert has a d1 hole with a diameter of 2.8 mm and operates as a center or peripheral cutting edge in a compatible body pocket.
The WCMX 030208 indexable insert (also written as wcmx030208) is used for drilling into solid structural steels and stainless steels on machining centers and CNC lathes. Calculate the spindle speed using n = 1000·vc/(π·D): for a drill diameter of 25 mm at a cutting speed of vc = 60 m/min, the result is approximately 764 rpm. Select the speed and feed for the nominal drill diameter, since the tool periphery operates at the highest cutting speed.
The PVD coating reduces abrasive and thermal edge wear at elevated cutting zone temperatures. The center insert chips due to material deformation near the axis, while the peripheral insert experiences thermal and crater wear at the full diameter. For deeper holes, supply internal coolant through the body to remove chips and protect both inserts from overload. Select the center and peripheral insert grades according to the body manufacturer's recommendations.
Grade H6310 is not intended for steels hardened above 45 HRC. The center and peripheral inserts must not be swapped — select them according to the catalog data sheet for the specific indexable drill body.
how to read the WCMT 030208 code — positions 1–7 of the designation
Designation WCMT 030208 according to the standard ISO 1832: 4 letters describe geometry and construction, 3 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
ISO 1832 designation decoder — how to read the code
Positions 1–4 · ISO code
1WShape
80° trigon
3 corners of 80° per side
2CClearance angle
α = 7°
positive, single-sided
3MTolerance
Class M (intermediate)
IC ±0.05–0.15 · thickness ±0.13 mm
4TType
Countersunk hole + chip breaker
countersink 40–60°, single-sided chip breaker
Positions 5–7 · dimensions [mm]
503Edge length
l = 3.47 mm
code 03 → edge length
602Thickness
s = 2.38 mm
between rake faces
708Corner radius
rε = 0.8 mm
code ÷ 10 → radius in mm
✓ 3 corners × 1 side = 3 cutting edges
workpiece material groups for grade H6310
| Materials machined with grade H6310 | |
|---|---|
| ✓ | Structural and alloy steel — ISO P group (P20-P40) |
| ✓ | Austenitic stainless steel — ISO M group (M20-M40) |
| ✗ | Steel hardened above 45 HRC — outside the range of grade H6310 |
| ✗ | Center and peripheral inserts — not interchangeable between positions |
installation, number of edges, materials and drill operation
Indexable drills with a fixed body and two pockets, where the insert has a hole d1 2.8 mm and operates as a center or peripheral cutting edge. Always verify the exact designation and clamping method against the catalog data sheet for the specific body.
Three — the trigon shape W (corner angle 80°) in the single-sided version provides three indexable edges. When one edge is worn, index the insert in the pocket to the next edge without replacing the entire drill. The thickness 2.38 mm and tolerance class M ensure repeatable seating after each indexing.
H6310 PVD-coated carbide covers structural and alloy steel in group ISO P20-P40 and stainless steel M20-M40. It is not intended for steels hardened above 45 HRC — separate grades are used for harder materials.
No — the self-centering geometry of the two inserts guides the drill without prior spot drilling or a guide bushing. However, at a hole depth of approximately 4–5× the diameter provide internal coolant through the body to flush chips away and protect both inserts from overload.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


