







Net price: €6.05
Description
| Technical data | |
|---|---|
| Side length l | 9.80 mm |
| Insert thickness s | 4.76 mm |
| Corner radius rε | 0.80 mm |
| ANSI code | SPMG 332 |
| Shape | square (S) |
| Design | right-hand |
| Carbide grade | MG-CX31NS |
cutting speed vc and feed fn for ISO group P steels
| Material | Vc [m/min] | Feed fn [mm/rev] |
|---|---|---|
| PSteel | 50-75 | 0.15-0.40 |
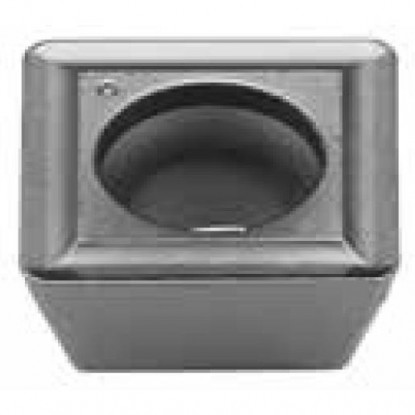
square carbide insert for indexable drill bodies
The SPMG 090408 carbide insert is a square indexable insert for indexable drills, manufactured by the Korean company Winstar. It is mounted in the body of a drill with replaceable cutting edges (known as a U-drill), where it replaces the cutting edge of a solid drill. The insert has four corners and is used on one side, providing four usable cutting edges. The square shape with a positive clearance angle reduces axial forces during drilling. Carbide grade MG-CX31NS has a CVD coating that increases the cutting edge's resistance to abrasive wear. Side length l is 9.80 mm, thickness s is 4.76 mm, and corner radius rε is 0.80 mm. The right-hand insert is designed for interrupted cutting of carbon and low-alloy steels.
The insert for indexable drills is selected based on the nominal drill diameter, not the insert itself. Calculate spindle speed using the formula n = 1000·vc/(π·D), where D is the drill diameter and vc is selected from the table. For D = 20 mm and vc = 60 m/min: n = 1000·60/(π·20) ≈ 955 rpm. In carbon and low-alloy steels, maintain a cutting speed of 50–75 m/min according to the cutting data table. Select feed to suit the drill diameter and rigidity — the greater the overhang, the lower the fn value.
In an indexable drill, the central position operates at approximately 0–50% of the maximum cutting speed, while the peripheral position operates at approximately 50–100% and determines hole diameter and quality. The body documentation specifies the position of the SPMG insert, its grade, and chip breaker geometry; the same ISO shape may be approved for both positions. Inserts for the two positions are purchased separately and selected as a matching pair according to the drill data sheet. Reduce feed at drill entry and exit to limit corner chipping. Rigid body mounting and coolant supplied through internal channels via the holder evacuate chips and protect the cutting edges from overheating. This variant is designed for 3D-class indexable drills; allow for reaming for high-precision holes, as indexable drilling provides lower dimensional accuracy than finishing operations.
This SPMG insert is exclusively a central insert (square) — it cannot replace the peripheral insert, which is a WCMT or WCMX trigon insert (80° trigon) of a different shape and size. For a complete indexable drill, select both inserts separately, in the grades and positions recommended by the body manufacturer — swapping them risks cutting edge chipping.
how to read the SPMG 090408 code — positions 1–7 of the designation
Designation SPMG 090408 according to the standard ISO 1832: 4 letters describe geometry and construction, 3 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
ISO 1832 designation decoder — how to read the code
Positions 1–4 · ISO code
1SShape
Square 90°
4 corners of 90° per side
2PClearance angle
α = 11°
positive, single-sided
3MTolerance
Class M (intermediate)
IC ±0.08 · thickness ±0.13 mm
4GType
Hole + chip breaker
chip breaker on both sides
Positions 5–7 · dimensions [mm]
509Size
l = 9.8 mm
IC = 9.8 mm (square: IC = l)
604Thickness
s = 4.76 mm
between rake faces
708Corner radius
rε = 0.8 mm
code ÷ 10 → radius in mm
✓ 4 corners × 1 side = 4 cutting edges
where the insert works and where to choose another solution
Applications of the central insert
| Rating | Application |
|---|---|
| ✔ | Indexable drill bodies (U-drill) with a pocket for the insert SPMG in size 09, in the position specified in the documentation |
| ✔ | Drilling into solid carbon and low-alloy steels — including interrupted cutting |
| ✔ | Holes produced with an indexable drill of class 3D |
| ✗ | Arbitrary assignment of SPMG to the central or peripheral position without checking the body documentation |
| ✗ | High-precision holes without subsequent reaming |
drill selection, insert position, and drilling parameters
Indexable drill bodies (U-drill) with a pocket for a square SPMG insert in size 09. The cutting edge dimensions are the side length 9.80 mm, thickness 4.76 mm and corner radius 0.80 mm. Inserts are not included with the body — select them for the specific drill system.
The position of this SPMG insert is specified in the documentation for the specific body. The central position operates at very low speed near the axis, while the peripheral position determines the diameter at maximum speed; the same ISO shape may be approved for both positions, but with a different grade or chip breaker. Select the inserts as a matching pair according to the drill data sheet and purchase them separately.
Using the formula n = 1000·vc/(π·D), where D is the drill diameter. For carbon steel, select vc from the range 50–75 m/min and feed fn from the range 0.15–0.40 mm/rev.
Carbon and low-alloy steels in group ISO P. According to the description, grade MG-CX31NS is designed for interrupted cutting of these materials.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


