









Net price: €6.58
Description
| Technical data | |
|---|---|
| Shape | R — round |
| Clearance angle | N — 0° (negative) |
| Tolerance class | M |
| Design type | G — hole and chip breaker (double-sided) |
| Inscribed circle diameter IC | 19 mm |
| Insert thickness s | 6.35 mm |
| Grade | 6630 Pramet (CVD) |
| ISO 513 range | P20-P45 |
CVD grade for steel and cast steel — medium machining and roughing under demanding conditions
| ISO group 513 | Material | Grade application range | Machining operation | Operating conditions |
|---|---|---|---|---|
| PSteel and cast steel | Structural steel, cast steel | P20-P45 | Medium machining and roughing | Demanding conditions, high temperature, high-productivity machining |
double-sided, negative N=0° geometry with a hole and chip breaker
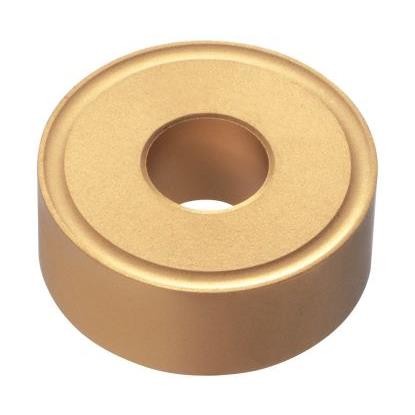
The RNMG 190600 turning insert is a round, negative indexable insert made of cemented carbide in grade 6630 from Pramet. The zero clearance angle means a double-sided design, so both faces of the insert carry a cutting edge. The round shape provides the strongest and most durable edge among turning inserts and withstands demanding turning conditions. The mounting hole and small chip breaker guide the chip during medium machining and roughing of steel and cast steel. Grade 6630 has a CVD coating (applied by chemical vapor deposition), which increases abrasion resistance while maintaining core strength. The letter N in the code confirms negative geometry, while G indicates a mounting hole with a chip breaker on both sides of the insert. The manufacturer specifies an application range of P20-P45.
The RNMG 190600 insert is suitable for longitudinal and copy turning of shafts, discs and forgings made of structural steels and cast steel. With a round insert, the entering angle increases with depth of cut, thinning the chip and allowing higher feeds. Calculate spindle speed using n = 1000·Vc/(π·D). For example, for a workpiece with a diameter of 60 mm and a cutting speed Vc = 200 m/min, the result is approximately 1061 rpm. Select the specific cutting speed from the data sheet for the grade 6630 and the holder used.
The CVD coating and strong core help maintain the edge at the high temperatures of high-productivity turning. In accordance with the range P20-P45 the insert is used for medium machining and roughing, rather than mirror finishing. Keep the depth of cut below the insert radius to maintain a small entering angle and smooth chip evacuation. Apply a generous coolant flow for consistent chip breaking and longer tool life. A constant coolant supply limits temperature buildup at the edge and reduces the risk of plastic deformation of the cutting edge.
Grade 6630 covers the range P20-P45 — steel and cast steel. It is not intended for mirror finishing or hardened steels; for hard turning, select a cubic boron nitride (CBN) cutting edge.
how to read the RNMG 190600 code — positions 1–6 of the designation
Designation RNMG 190600 according to the standard ISO 1832: 4 letters describe geometry and construction, 2 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
ISO 1832 designation decoder — how to read the code
Positions 1–3 · ISO code
1RShape
Round
peripheral edge without corners
2NClearance angle
α = 0°
negative, double-sided
3MTolerance
Class M (intermediate)
IC ±0.10 · thickness ±0.13 mm
Positions 4–6
4GType
Hole + chip breaker
chip breaker on both sides
519Diameter
d = 19 mm
round insert — full radius
606Thickness
s = 6.35 mm
between rake faces
✓ Peripheral edge — full circle, no corners
materials, operating conditions and holder types for round inserts
APPLICATION RANGE:
| ✓ | Structural steel and cast steel (ISO P20-P45) |
| ✓ | Medium machining and roughing, including interrupted cuts |
| ✓ | Demanding conditions, high temperature, high-productivity turning |
| ✓ | Holders for round RNMG inserts with a hole — lever, clamp or screw clamping |
| ✗ | Hardened steels, hard turning (a CBN grade is required) |
| ✗ | Finishing to very low surface roughness |
| ✗ | Nonferrous metals and aluminum (ISO group P grade) |
design, grade, dimensions and material range
Double-sided. The clearance angle N = 0° (negative insert) means that the cutting edge runs along both sides. When one side is worn, turn the insert over in its pocket and use the other working face.
Grade 6630 from Pramet is a carbide with a coating of CVD for steel and cast steel in the range ISO P20-P45. It covers medium machining and roughing under demanding conditions and at high cutting temperatures.
The inscribed circle diameter is 19 mm, and the insert thickness is 6.35 mm. The shape is round (letter R), without a corner — the entire edge forms a single continuous arc with a full radius.
Not as standard. Grade 6630 is intended for medium machining and roughing of steel and cast steel (P20-P45), not hardened steels — cubic boron nitride (CBN) inserts are used for hard turning.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


