









Net price: €6.05
Description
| Technical data | |
|---|---|
| Designation | SDHT 1504 AESN |
| Shape | Square 90° (S) |
| Clearance angle | 15° (D) |
| Side length l | 15.875 mm |
| Insert thickness s | 4.76 mm |
| ANSI code | SDHT 53 |
| Grade | GM43 (P20-P40) |
| Material | Cemented carbide |
| Chip breaker | AESN — manufacturer code, not interpreted |
alloy and tool steel milling — ISO P group, conservative values
| Workpiece material | vc [m/min] | fz [mm/tooth] | ap [mm] | ae [% D] |
|---|---|---|---|---|
| PAlloy and tool steel | 130-200 | 0.10-0.20 | 1.0-4.0 | 30-70 |
AESN code not interpreted, four cutting edges, 15° clearance angle
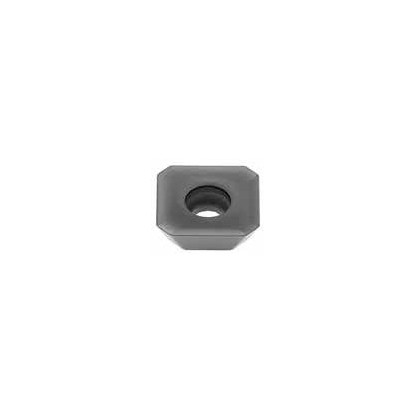
The SDHT 1504 AESN GM43 milling insert is a square indexable cemented carbide insert designed for milling alloy, tool, and stainless steels. The square shape with a fifteen-degree clearance angle (designation D) provides four cutting edges per side and high corner strength. AESN is a manufacturer code and cannot be interpreted without the product data sheet. The insert with 15° clearance and a mounting hole (type T) performs well in shoulder, step, and pocket milling systems and general steel machining. Grade GM43 in the ISO P20-P40 group combines wear resistance with resistance to thermal cracking, allowing the insert to withstand heavy, interrupted milling conditions. Side length l is 15.875 mm, and thickness s is 4.76 mm.
The insert performs well in shoulder, step, and face milling, as well as roughing and semi-finishing alloy steel housings, plates, and castings. Calculate milling head speed using n = 1000·vc/(π·D): for a milling head with a diameter of 63 mm at a cutting speed of vc = 180 m/min, the result is approximately 909 rpm. Maintain feed per tooth (fz) within 0.10–0.20 mm for structural steels, selecting the number of milling head teeth to suit its diameter. For larger milling head diameters, reduce rpm proportionally according to the formula while maintaining the recommended cutting speed.
Chip thickness depends on the milling head entering angle — the smaller the angle, the thinner the chip and the higher the permissible feed rate at the same edge load. For stainless, acid-resistant, and heat-resistant steels, reduce cutting speed and use flood cooling to limit work hardening and dissipate heat. Select depth of cut ap so that it does not exceed the active cutting edge length of the insert. Climb milling on CNC machining centers further extends edge life and improves the machined surface finish.
Grade GM43 belongs to the ISO P group (P20-P40). For hardened steels and hard machining, select a grade explicitly specified for this application by the tool manufacturer.
how to read the SDHT 1504 AESN code — positions 1–10 of the designation
Designation SDHT 1504 AESN according to the standard ISO 1832: 4 letters describe the geometry and construction, 2 numeric codes describe the dimensions, and the suffix AESN — the wiper edge geometry. Each field has a number, an icon and a brief description.
ISO 1832 designation decoder — how to read the code
Positions 1–3 · ISO code
1SShape
Square 90°
4 corners of 90° per side
2DClearance angle
α = 15°
positive, single-sided
3HTolerance
Class H (high precision)
ground insert — highest dimensional accuracy
Positions 4–6
4TType
Countersunk hole + chip breaker
countersink 40–60°, single-sided chip breaker
515Size
l = 15.875 mm
IC = 15.875 mm (square: IC = l)
604Thickness
s = 4.76 mm
between rake faces
AESN suffix · wiper edge
7AEntering angle
κ = 45°
45° angle milling cutters and milling heads
8EWiper land
α′ = 20°
wiper land clearance angle
9SEdge condition
Chamfered and rounded
S-land — strongest edge
10NHand
Right-hand and left-hand
symmetrical design
✓ 4 corners × 1 side = 4 cutting edges
milling heads with square pockets — materials and operations
Insert applications and limitations:
| Rating | Application |
|---|---|
| ✓ | Shoulder, step, and face milling in alloy and tool steels |
| ✓ | Milling stainless, acid-resistant, and heat-resistant steels at reduced speed |
| ✓ | Machining cast steel and cast iron on conventional machine tools and CNC machining centers |
| ✓ | Milling heads with a pocket for a square insert (SDHT type) |
| ✗ | Hardened steels and hard machining without a manufacturer-approved grade |
| ✗ | Pockets designed for a different insert shape, clearance angle, or size |
dimensions, grade, milling head selection, and cutting data
The square single-sided insert has 4 corners at 90° each, providing 4 cutting edges. Once an edge becomes dull, rotate the insert in the milling head pocket to the next edge without replacing the tool.
Grade GM43 covers group ISO P20-P40 — alloy and tool steels machined at high and medium speeds. It is also suitable for stainless, acid-resistant, and heat-resistant steels, cast steel, and cast iron at reduced cutting speed.
The side length l is 15.875 mm, and the insert thickness s 4.76 mm. The shape is a 90° square (S) with a clearance angle of 15° (D); the AESN code requires the product data sheet and is not interpreted here.
The square shape (S) with a clearance angle of 15° and a mounting hole (type T) fits milling heads with a pocket for a 1504 square insert. Select the milling head for the operation — shoulder, pocket, or face milling — and match the number of teeth to its diameter and the machine power.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


