







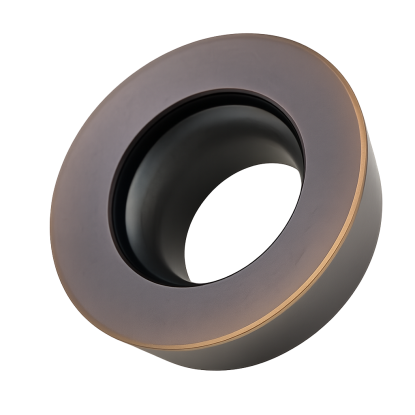

Description
| Technical data | |
|---|---|
| Insert diameter d | 5 mm |
| Insert thickness s | 1.59 mm |
| Full radius R | 2.5 mm |
| Hole diameter d1 | 2.3 mm |
| Clearance angle α | 15° |
| Chip breaker | none (W) |
mold and profiled surface milling — ISO P and M groups, conservative values
| Material | Vc [m/min] | fz [mm/tooth] | ap [mm] | ae [% D] |
|---|---|---|---|---|
| PSteel | 150-220 | 0.10-0.22 | 0.5-1.25 | 60-80 |
| MStainless steel | 80-140 | 0.08-0.18 | 0.3-1.25 | 50-70 |
full radius 2.5 mm, positive geometry, variable entering angle
Milling insert RDMW 0501 MO is a round indexable insert made of cemented carbide in grade H6310, designed for copy, profile and plunge milling. The round outline with a diameter of 5 mm and a full radius of 2.5 mm has no corner that could chip, so the edge cuts stably in interrupted cutting. The fifteen° clearance angle (letter D in the designation) provides positive geometry that reduces cutting forces. A distinctive feature of the round insert is its variable effective entering angle κ: at a shallow depth of cut, κ is small and chip thickness decreases, protecting the edge.
The round insert is suitable for milling heads used to machine molds, dies and 3D surfaces in structural steels, as well as stainless steel components. Since forces increase with depth of cut, selecting ap determines machining stability. The effective entering angle depends directly on ap: at the recommended maximum ap = 0.5 × R = 1.25 mm, the result is κ_eff = arccos((2.5 − 1.25) / 2.5) = arccos(0.5) = 60°. Shallower passes produce a smaller angle and a thinner chip, so keep ap at no more than half the radius for stable machining.
Grade H6310 is a PVD-coated (physical vapor deposition) carbide with a versatile application range: steel in groups P20-P40 and stainless steel M20-M40. The PVD coating withstands the thermal and impact loads typical of milling, in which each tooth repeatedly enters and exits the material per revolution. The indexable insert in this grade is supplied by the Korean brand Horn. Use climb milling and maintain a constant feed per tooth (fz) to limit friction and work hardening of the stainless steel layer being cut.
Grade H6310 covers groups P20-P40 and M20-M40 and is not intended for steels hardened above 45 HRC; for harder materials, consider H8320. For a radius R = 2.5 mm, keep ap no greater than 0.5 × R = 1.25 mm.
how to read the RDMW 0501 code — designation positions 1–6
Designation RDMW 0501 according to the standard ISO 1832: 4 letters describe geometry and construction, 2 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
ISO 1832 designation decoder — how to read the code
Positions 1–3 · ISO code
1RShape
Round
peripheral edge without corners
2DClearance angle
α = 15°
positive, single-sided
3MTolerance
Class M (intermediate)
IC ±0.05 · thickness ±0.13 mm
Positions 4–6
4WType
Countersunk hole, no chip breaker
40–60° countersink, smooth rake face
505Diameter
d = 5 mm
round insert — full radius
601Thickness
s = 1.59 mm
between rake faces
✓ Peripheral edge — full circle, no corners
machining groups for grade H6310 — applications and materials to avoid
| Material / ISO group | Suitability |
|---|---|
| Structural and alloy steel (ISO P20-P40) | ✓ recommended |
| Stainless steel (ISO M20-M40) | ✓ recommended |
| Hardened steel above 45 HRC | ✗ not recommended |
| Harder materials / outside the P-M range (consider H8320) | ✗ different grade |
operations, materials and depth of cut selection
For copy, profile and plunge milling, as well as 3D mold and die machining. The round edge with a full radius of 2.5 mm has high mechanical strength, and its effective entering angle increases with depth of cut. For this insert, maintain ap ≤ 0.5 × R = 1.25 mm.
PVD-coated carbide in grade H6310 covers steel in group P20-P40 and stainless steel M20-M40. Do not use it for hardened steels above 45 HRC; for harder materials, consider H8320.
The effective entering angle increases with depth: at the recommended maximum ap = 0.5 × R = 1.25 mm it is κ_eff = arccos(0.5) = 60°. Shallower passes produce a smaller angle, a thinner chip and lower forces.
Insert diameter 5 mm, thickness 1.59 mm, hole diameter 2.3 mm, full radius 2.5 mm, clearance angle 15° (letter D in the designation). Class M tolerance ensures repeatable insert seating in the milling head pocket.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


