





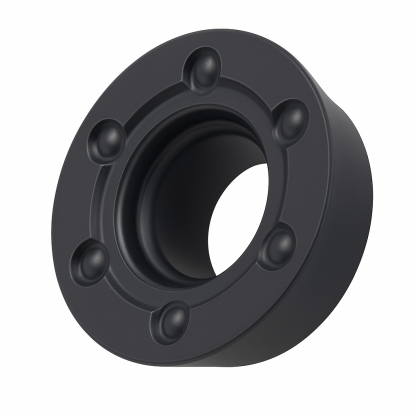

Description
| Technical data | |
|---|---|
| Diameter d (side length l) | 12.70 mm |
| Insert thickness s | 4.76 mm |
| Full radius R | 6.35 mm |
| Clearance angle α | 11° (positive) |
| Tolerance class | M |
| Grade | H6310 (PVD) |
face and copy milling — conservative ranges for ISO P and M groups
| Material | vc [m/min] | Feed fz [mm/tooth] | ap [mm] | ae [% D] |
|---|---|---|---|---|
| PSteel, cast steel | 150-220 | 0.10-0.22 | 0.5-3.0 | 60-80 |
| MStainless steel | 80-140 | 0.08-0.18 | 0.3-2.0 | 50-70 |
full radius, positive geometry, discontinuous chips of varying thickness
The RPMT 1204MO milling insert is a round, positive indexable insert made of grade H6310 cemented carbide, designed for milling steel, cast steel, and stainless steel. The R shape, a full circle, forms one continuous edge with no corners that could chip under load. This allows the insert to withstand varying dynamic loads with a large and variable uncut chip cross section. The eleven° clearance angle in the positive geometry reduces cutting resistance and power consumption. A diameter of 12.70 mm and thickness of 4.76 mm provide a rigid edge for roughing, face milling, and copy milling. The Korean brand Horn offers this grade as a versatile solution for steel and stainless steel.
The RPMT 1204MO insert performs well in copy and profile milling of molds, dies, and 3D surfaces, as well as rough face milling of steel and cast steel. Calculate the milling head speed using n = 1000·vc/(π·D): for a head with a diameter of 50 mm at vc = 180 m/min, the result is approximately 1146 rpm. Keep the feed per tooth (fz) within 0.10–0.22 mm for steel to maintain uniform chip thickness. The round geometry provides a long, strong edge, allowing a single insert to machine a large volume of material between indexing operations.
Select the depth of cut to keep cutting forces low: set ap no greater than half the radius, or approximately 3 mm for a radius of 6.35 mm. For stainless steel, reduce the cutting speed to 80–140 m/min and apply coolant continuously, because austenite conducts heat poorly and work-hardens. Climb milling on a CNC machine with table backlash eliminated extends tool life and improves surface quality. When machining materials with a varying chip cross section, a round carbide insert is particularly resistant to impact loads.
Grade H6310 is not intended for hardened steels — for harder materials, choose grade H8320 or an insert with a ceramic or cubic boron nitride (CBN) cutting edge.
how to read the RPMT 1204 code — positions 1–6 of the designation
Designation RPMT 1204 according to the standard ISO 1832: 4 letters describe geometry and construction, 2 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
ISO 1832 designation decoder — how to read the code
Positions 1–3 · ISO code
1RShape
Round
peripheral edge without corners
2PClearance angle
α = 11°
positive, single-sided
3MTolerance
Class M (intermediate)
IC ±0.08 · thickness ±0.13 mm
Positions 4–6
4TType
Countersunk hole + chip breaker
countersink 40–60°, single-sided chip breaker
512Diameter
d = 12 mm
round insert — full radius
604Thickness
s = 4.76 mm
between rake faces
✓ Peripheral edge — full circle, no corners
grade H6310 — ISO groups and workpiece materials
| Workpiece material | ISO group | Recommendation |
|---|---|---|
| Structural steel and cast steel | P20-P40 | ✔ recommended |
| Stainless steel | M20-M40 | ✔ recommended |
| Discontinuous chips with a large and variable cross section | P / M | ✔ advantage of the round edge |
| Hardened steel | H | ✗ outside the H6310 application range |
materials, round geometry, and cutting parameter selection
For structural steel and cast steel in group ISO P20-P40 and stainless steel in group ISO M20-M40. PVD-coated grade H6310 performs well with discontinuous chips of large and variable cross section. Do not use it for hardened steels.
The round edge has no corners, so it distributes the load over a long section and is highly resistant to chipping. The entering angle varies with the depth of cut: at a shallow depth ap forces are low and increase only at greater depths. This is an advantage in copy milling and roughing.
To keep cutting forces low, set ap no greater than half the radius. For a radius of 6.35 mm this gives approximately 3 mm per pass. Greater depth increases the entering angle and chip thickness, requiring a more rigid milling head and greater spindle power.
The insert diameter is 12.70 mm, corresponding to a full radius of 6.35 mm, and the thickness is 4.76 mm. Tolerance class M ensures repeatable edge positioning after the insert is rotated in the milling head pocket.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


