








Net price: €8.82
Description
| Technical data | |
|---|---|
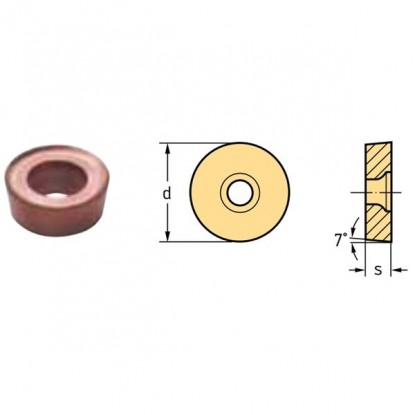
| Insert shape | round (R) |
| Insert diameter d | 5.00 mm |
| Insert thickness s | 1.51 mm |
| Clearance angle | 15° (D) |
| Tolerance class | H (very precise) |
| Chip breaker | without a chip breaker |
| Grade | PC9530 (Korloy) |
copy milling and profile milling — ISO group M
| Material | ISO group | Vc [m/min] | Feed fz [mm/tooth] | ap [mm] |
|---|---|---|---|---|
| MStainless steel | M | 80-140 | 0.08-0.18 | 0.3-1.25 |
positive 15° geometry, tolerance H, without a chip breaker
The RDHW 0501 milling insert is a round indexable insert made of cemented carbide in Korloy grade PC9530, designed for copy milling and profile milling of stainless steel. Shape R, a full circle with a diameter of 5.00 mm, has no corner that could chip, giving the edge exceptional mechanical strength. The clearance angle of fifteen degrees, designated by the letter D, creates positive geometry that reduces cutting forces and power consumption. Tolerance class H ensures precise, repeatable insert seating in the milling head pocket. The thickness of 1.51 mm and the absence of a chip breaker indicate light finishing of molds, dies and curved surfaces. The round outline forms one continuous edge — once the working sector is worn, simply index the insert in the pocket.
The RDHW 0501 round insert performs well when copy milling dies, injection molds and three-dimensional surfaces in stainless steel. The effective entering angle (κ) varies with the depth of cut. For a radius R = 2.5 mm and a depth ap = 0.5 mm, it is κ ≈ arccos((2.5 − 0.5) / 2.5), or approximately 37°. A shallow depth produces a thin chip and low forces, allowing smooth tool operation on slender arbors and at long overhangs. Select a depth of cut that does not exceed half the insert radius.
For stainless steel, maintain a cutting speed of 80–140 m/min and a feed per tooth (fz) of 0.08–0.18 mm to limit work hardening of the layer being cut. Calculate chip thickness using hex = fz × sin κ. Constant cooling and a uniform feed protect the edge against chip adhesion, which is typical when machining stainless steel. Cutting too slowly hardens the surface and accelerates cutting edge wear. Indexable inserts in grade PC9530 are supplied by Korloy.
Product sources confirm grade PC9530 for stainless steel (ISO M). For other material groups, select a grade confirmed by the tool manufacturer.
how to read the RDHW 0501 code — positions 1–6 of the designation
Designation RDHW 0501 according to the standard ISO 1832: 4 letters describe geometry and construction, 2 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
ISO 1832 designation decoder — how to read the code
Positions 1–3 · ISO code
1RShape
Round
peripheral edge without corners
2DClearance angle
α = 15°
positive, single-sided
3HTolerance
Class H (high precision)
ground insert — highest dimensional accuracy
Positions 4–6
4WType
Countersunk hole, no chip breaker
40–60° countersink, smooth rake face
505Diameter
d = 5 mm
round insert — full radius
601Thickness
s = 1.59 mm
between rake faces
✓ Peripheral edge — full circle, no corners
pocket for a round insert with a diameter of 5.00 mm and a clearance angle of 15°
Tool selection and operating range
| Rating | Tool, material or application |
|---|---|
| ✔ | Copy milling, profile milling and plunge milling of three-dimensional molds and dies |
| ✔ | Milling heads and cutters for round inserts R with a pocket for a diameter of 5.00 mm |
| ✔ | Stainless steel — group ISO M |
| ✔ | Compatible pocket for a round insert with a diameter of 5.00 mm and a thickness of 1.51 mm |
| ✗ | Other material groups — require a grade confirmed by the manufacturer |
| ✗ | Milling right-angle 90° shoulders — a round insert does not produce a square corner |
geometry, cutting data selection and applications
Grade PC9530 by Korloy is designed for stainless steel — group ISO M. For other material groups, select a grade confirmed by the manufacturer.
The clearance angle is 15° (designation D in the ISO code). This produces positive, single-sided geometry — the insert cuts on its top face, reducing cutting forces and power consumption.
As a conservative starting point, maintain a cutting speed of 80-140 m/min, a feed per tooth of 0.08-0.18 mm and a depth of 0.3-1.25 mm. Use continuous cooling and a uniform feed to limit work hardening of the layer being cut.
A circle has no corner that could chip, so the edge withstands high loads. The effective entering angle increases with the depth of cut — at a shallow depth ap the chip is thin and forces are low.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


