







Description
| Technical data | |
|---|---|
| Shape | Round (R) |
| IC diameter | 10 mm |
| Insert radius | 5 mm |
| Thickness s | 3.18 mm |
| Clearance angle | 15° (D) |
| Grade | H6310 (PVD) |
copy, profile, and plunge milling — ISO P and M groups
| Material | vc [m/min] | fz [mm/tooth] | ap [mm] | ae [% D] |
|---|---|---|---|---|
| PSteel | 150-220 | 0.10-0.22 | 0.5-2.5 | 60-80 |
| MStainless steel | 80-140 | 0.08-0.18 | 0.3-2.0 | 50-70 |
positive 15° geometry with a hole, without a chip breaker
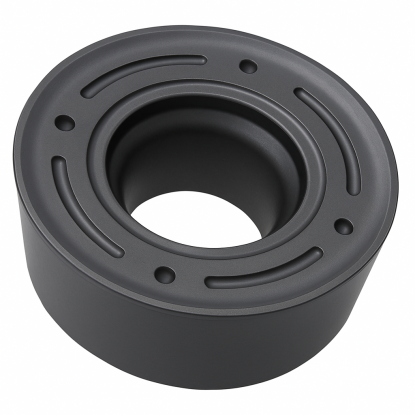
Milling insert RDMW 1003 MO is a round indexable insert made of cemented carbide in grade H6310, designed for milling structural steels and stainless steel. The round shape (letter R) with a diameter of 10 mm and a radius of 5 mm provides a continuous cutting edge without a corner that could chip. A clearance angle of fifteen ° (letter D) creates positive geometry that reduces cutting forces. The PVD (physical vapor deposition) coating improves resistance to abrasive wear and elevated operating temperatures. The carbide insert is secured with a central screw through the hole, and the absence of a chip breaker (type W) promotes smooth chip evacuation during copy machining.
Round insert RDMW performs best in copy, profile, and plunge milling, where a variable depth of cut requires a strong edge. An advantage of round geometry is that forces scale automatically with the depth of cut. At a shallow depth ap, the effective entering angle κ is small, so the chip is thin and edge loading is light. For ap 1 mm and a radius of 5 mm, this angle is approximately arccos((5−1)/5) = arccos(0.8) ≈ 37°. Calculate the milling head speed using n = 1000·Vc/(π·D): for a milling head with a diameter of 50 mm at Vc 200 m/min, the result is approximately 1273 rpm.
To protect the round edge, a depth of cut no greater than half the radius is recommended, meaning ap up to 2.5 mm for this insert. Select the feed per tooth fz (the distance traveled by one tooth per revolution) according to the material group: lower for stainless steel, higher for structural steel. Grade H6310 covers steel in ISO P20-P40 and stainless steel in M20-M40, so a single insert handles a wide range of workshop materials. Indexable inserts made of H6310 cemented carbide are supplied by the Korean brand Horn. For austenitic steel, maintain a constant feed and continuous coolant flow to limit work hardening of the layer being cut.
Grade H6310 is not intended for hardened steels above 45 HRC. For a round insert with a radius of 5 mm maintain a depth of cut ap up to 2.5 mm (half the radius) to maintain a small entering angle and protect the edge.
how to read the RDMW 1003 code — designation positions 1–6
Designation RDMW 1003 according to the standard ISO 1832: 4 letters describe geometry and construction, 2 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
ISO 1832 designation decoder — how to read the code
Positions 1–3 · ISO code
1RShape
Round
peripheral edge without corners
2DClearance angle
α = 15°
positive, single-sided
3MTolerance
Class M (intermediate)
IC ±0.08 · thickness ±0.13 mm
Positions 4–6
4WType
Countersunk hole, no chip breaker
40–60° countersink, smooth rake face
510Diameter
d = 10 mm
round insert — full radius
603Thickness
s = 3.18 mm
between rake faces
✓ Peripheral edge — full circle, no corners
where to use the H6310 round insert — ISO material groups
| Material / application | ISO group | Recommendation |
|---|---|---|
| Structural and alloy steel | P20-P40 | ✔ recommended |
| Stainless steel | M20-M40 | ✔ recommended |
| Copy, profile, and plunge milling | — | ✔ round geometry |
| Hardened steel above 45 HRC | H | ✗ outside the range |
| Aluminum and its alloys | N | ✗ outside the grade's application range |
edges, materials, and depth of cut selection
The round insert has one continuous edge around its entire circumference. Depending on the depth of cut and indexing in the pocket, you use successive sectors of the circumference by rotating the insert after one section wears out — without replacing the tool holder.
For steel in group ISO P20-P40 and stainless steel M20-M40. The PVD coating increases resistance to heat and abrasive wear. The grade is not intended for hardened steels above 45 HRC.
For a radius of 5 mm the recommended depth is ap ≤ 2.5 mm (half the radius). This maintains a small effective entering angle and a thin chip.
A round edge has no corner, so it is stronger and better withstands copy milling of 3D molds. Forces increase gradually with the depth of cut, reducing vibration on thin workpieces and protecting the edge against chipping.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


