
Description
| Technical data | |
|---|---|
| Shape | R — round |
| Insert diameter d | 10.0 mm |
| Insert thickness s | 3.97 mm |
| Clearance angle α | 11° (positive) |
| Tolerance class | M |
| Mounting type | T — hole with chip breaker |
| Grade | H6310 (PVD) |
finishing, semi-finishing and roughing — ISO P and M groups
| Material | Finishing | Semi-finishing | Roughing | ||||||
|---|---|---|---|---|---|---|---|---|---|
| Vc [m/min] | Feed fz [mm/tooth] | ap [mm] | Vc [m/min] | Feed fz [mm/tooth] | ap [mm] | Vc [m/min] | Feed fz [mm/tooth] | ap [mm] | |
| PSteel | 180-220 | 0.10-0.14 | 0.3-0.8 | 160-200 | 0.14-0.18 | 0.8-1.5 | 150-180 | 0.18-0.22 | 1.5-2.5 |
| MStainless steel | 110-140 | 0.08-0.12 | 0.3-0.7 | 100-130 | 0.12-0.15 | 0.7-1.3 | 80-120 | 0.15-0.18 | 1.3-2.0 |
round shape R, positive 11° geometry, hole with chip breaker
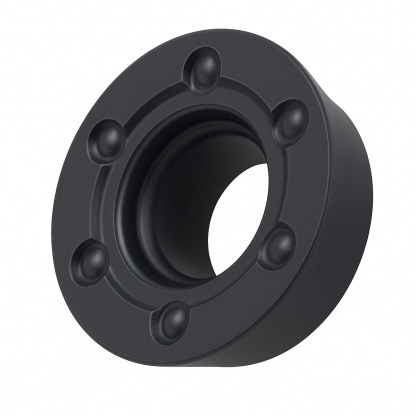
This MOE milling insert is a round, positive indexable insert made of H6310 cemented carbide, designed for milling steel and stainless steel. The round R shape has no corner, giving the edge exceptional mechanical strength and good resistance to interrupted cutting. The eleven° clearance angle, indicated by the letter P, reduces cutting forces, facilitating machining on lower-powered machines. The round geometry provides a variable entering angle: at a shallow depth of cut, the effective angle is small and the chip is thin. The insert is mainly used for copy and profile milling, as well as machining three-dimensional molds. The countersunk hole and single-sided chip breaker, designated type T according to ISO 1832, guide the chip during machining.
The round insert is suitable for copy milling molds, dies and curved surfaces in structural steels, as well as stainless steel components. For an insert with a radius R of five millimeters, the rule ap ≤ 0.5×R limits the recommended depth of cut to 2.5 mm. At a depth ap of 1 mm, calculate the entering angle using kappa = arccos((5−1)/5), giving approximately 37°. This results in a thin chip and low cutting forces, so the insert runs smoothly even with a longer tool overhang. Select a cutting speed from 150 to 220 m/min for steel and a lower speed for stainless steel.
Grade H6310 is a versatile carbide grade for steel and stainless steel with a PVD coating applied by physical vapor deposition. When machining stainless steel, maintain a constant feed fz and continuous coolant flow to limit work hardening of the layer being cut. Select a depth of cut no greater than half the insert radius, since deeper engagement increases the entering angle and edge load. The round design allows the insert to be indexed repeatedly around its circumference. Indexable inserts in grade H6310 are supplied by the Korean brand Horn.
Grade H6310 is not intended for hardened steels above 45 HRC or for cast iron and nonferrous metals. For groups ISO K and N select a grade approved by the tool manufacturer.
how to read the RPMT 10T3 code — positions 1–6 of the designation
Designation RPMT 10T3 according to the standard ISO 1832: 4 letters describe geometry and construction, 2 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
ISO 1832 designation decoder — how to read the code
Positions 1–3 · ISO code
1RShape
Round
peripheral edge without corners
2PClearance angle
α = 11°
positive, single-sided
3MTolerance
Class M (intermediate)
IC ±0.08 · thickness ±0.13 mm
Positions 4–6
4TType
Countersunk hole + chip breaker
countersink 40–60°, single-sided chip breaker
510Diameter
d = 10 mm
round insert — full radius
6T3Thickness
s = 3.97 mm
between rake faces
✓ Peripheral edge — full circle, no corners
grade H6310 — ISO groups and types of milling operations
| Material / operation | Application |
|---|---|
| Structural and alloy steel (ISO P20-P40) | ✔ recommended |
| Cast steel | ✔ recommended |
| Stainless steel (ISO M20-M40) | ✔ recommended |
| Copy milling, profile milling and 3D mold machining | ✔ recommended |
| Hardened steel above 45 HRC | ✗ no |
| Cast iron and nonferrous metals (ISO K/N) | ✗ no |
materials, round geometry and milling data selection
Grade H6310 is versatile: it covers steel in group ISO P20-P40 and stainless steel ISO M20-M40. It is a PVD-coated carbide for steel, cast steel and stainless steel. Do not use it for hardened steels above 45 HRC or for cast iron and nonferrous metals.
The round cutting edge has no corner, giving it high mechanical strength and resistance to chipping. It also has a variable entering angle: at a shallow depth of cut, the chip is thin and forces are low. This type of insert performs best in copy milling, profile milling and mold machining 3D.
For round inserts, the rule is ap ≤ 0.5×R. With a radius of R = 5 mm the recommended depth should not exceed 2.5 mm. At ap = 1 mm, the entering angle is approximately 37°, resulting in a thin chip and smooth operation. Deeper engagement increases cutting forces.
Yes — grade H6310 covers group ISO M20-M40. Maintain a cutting speed of 80-140 m/min, a constant feed and continuous emulsion cooling. Stainless steel can dissipate heat poorly and work-harden if cutting is too slow, so avoid interrupting the feed.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |


This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.