





- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot
Description
CUTTING WIDTH4 mm
CUTTING DEPTH T MAX25 mm
MAX. BAR DIAMETERØ50 mm
INSERT · 2 EDGESMGMN 400
Parting tool 20X20 4 mm T25 Smoxh
Technical data for the holder for Korloy MGMN 400 inserts
| Technical data | |
|---|---|
| Designation | BDKT R 2020 K4C T25 |
| Type | holder for parting and external grooving |
| Shank height h | 20 mm |
| Shank width B | 20 mm |
| Overall length L | 125 mm |
| Dimension S (to the insert edge) | 20.4 mm |
| Cutting depth T max | 25 mm |
| Max. parting diameter D max | Ø50 mm |
| Insert pocket | MGM. 4C (MGMN 400, width 4 mm) |
| Hand | R – right-hand (left-hand version: SM38844) |

BDKT-R 2020 K4C T25 – operation with MGMN inserts
What this tool can do, screw clamping and a double-edged insert
Parting tool 4 mm BDKT-R 2020 K4C T25 (Smoxh) parts off bars up to Ø50 mm and cuts external grooves. It uses MGMN 400 carbide inserts clamped from above by the flexible lip of the head. The BKTV M6x25 screw tightens the lip, and the insert can be changed in a dozen or so seconds.
The insert is supported by the narrow blade of the head, 25 mm long — this is the cutting depth T max. Beyond this point, the body widens to the shank width, so only the blade fits into the 4 mm slot. This limits the tool to parting off bars up to Ø50 mm, or twice T max.
Dimension S = 20.4 mm means that the cutting edge projects 0.4 mm beyond the side of the 20 mm wide shank. This allows cutting close to the chuck jaws without the shank rubbing against the workpiece face. The 20x20 mm shank with a length of 125 mm is a common size for tool posts on conventional and CNC lathes.
The MGMN 400 insert has two cutting edges at opposite ends. When the first becomes dull, rotate the insert by 180° and use the second.
Applications of the 4 mm parting tool – parting off workpieces and grooving
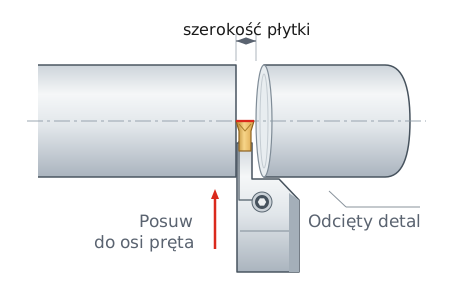
Parting – cutting a part off a bar
The blade enters the bar all the way to the axis and the part separates. Bars up to Ø50 mm, a 4 mm kerf, and material loss limited to the insert width.
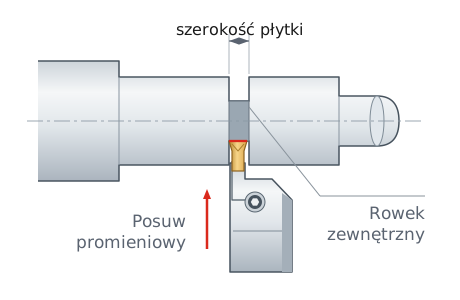
Cutting external grooves
A 4 mm groove between shaft shoulders or a retaining ring groove at the end of a journal, up to 25 mm deep. Cut wider grooves with several adjacent passes.

Screw clamping from above
The BKTV M6x25 screw draws the flexible lip of the head against the insert. Change the insert with an AA5 key without removing the tool from the tool post.

Double-edged insert
MGMN 400 has a cutting edge at both ends. One edge dull? Rotate the insert by 180° and use the other.

Material loss: 4 mm
Each parting cut turns only 4 mm of bar into chips. For 100 parts, this consumes 10 cm less bar than a tool with a 5 mm insert.
Dimensions and cutting reach – dimensional drawing
Side view and top view
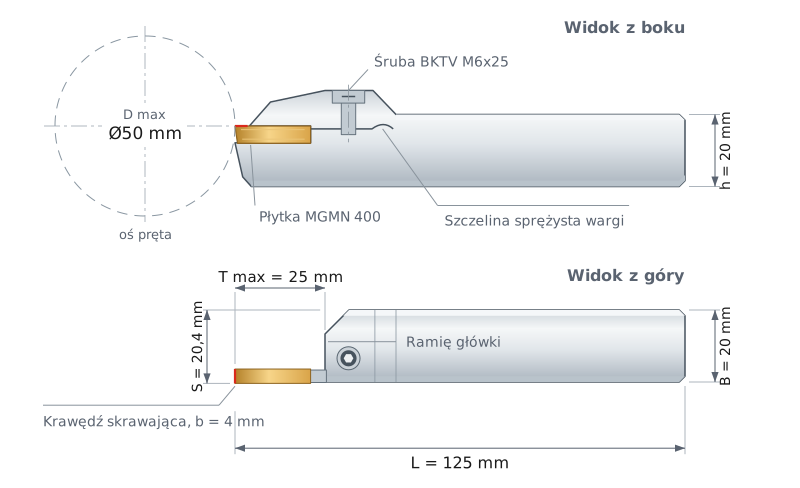

HEIGHT h
20 mm

WIDTH B
20 mm

LENGTH L
125 mm

DIMENSION S
20.4 mm
Measure T max from the insert tip to the point where the blade transitions into the wider head. Grooves up to 25 mm deep can also be cut in bars larger than Ø50 mm.
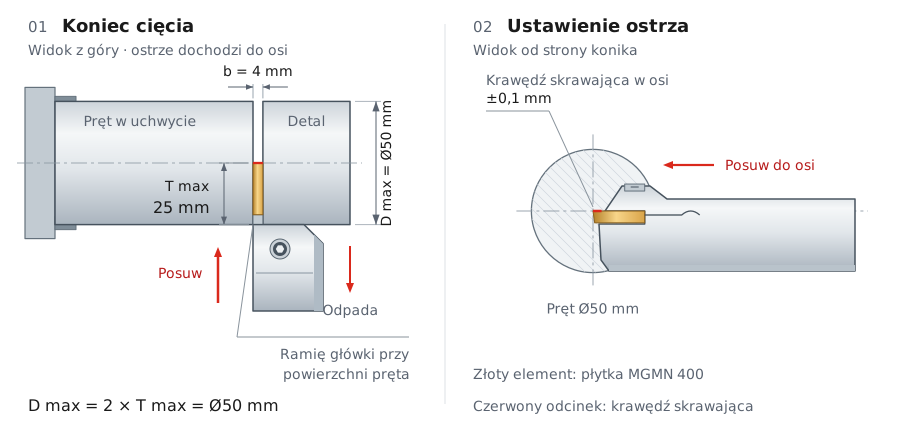
At the end of the cut, the insert tip is at the bar centerline and the shoulder of the head touches the bar surface. The second panel shows the cutting edge height: the edge must be on the centerline within ±0.1 mm. An edge below center leaves a pip; above center, it rubs against the material.
Decoding the BDKT R 2020 K4C T25 designation
Five elements of the Smoxh code, read from the left
Designation: BDKT R 2020 K4C T25
BDKT
Element 1
holder type
holder type
For parting
BDKT
BDKT
Smoxh series for external grooving and parting with screw clamping. The counterpart for internal grooving is designated BIKT.
R
Element 2
hand
hand
Right-hand
R
R
Standard configuration with the workpiece held in a chuck to the left of the tool. Version L is a mirror image – code SM38844.
2020
Element 3
shank
shank
20x20 mm
2020
2020
The first two digits indicate height h, and the next two indicate width B. Fits a tool post for 20 mm tools.
K4C
Element 4
insert pocket
insert pocket
MGM. 4C
K4C
K4C
K – Korloy MGMN insert system, 4 – cutting width of 4 mm. Versions K2C…K8C accept inserts from 2 to 8 mm.
T25
Element 5
depth
depth
T max 25 mm
T25
T25
Blade length from the insert tip to the head shoulder. Maximum parting diameter is 2 × T max = Ø50 mm.
Smoxh catalog convention, not ISO 5608 · dimensions: h 20 · B 20 · L 125 · S 20.4 mm
Parting data – speeds and feeds for a 4 mm insert
Starting values with coolant; refer to the insert grade data sheet for definitive data
The table provides starting values for coated MGMN 400 inserts with coolant. Select the upper speed range when clamping is rigid and tool overhang is short.
| Workpiece material | Vc [m/min] | fn [mm/rev] |
|---|---|---|
| PCarbon steel | 120–200 | 0.07–0.15 |
| PAlloy steel | 130–180 | 0.07–0.15 |
| PHardened steel | 70–130 | 0.07–0.12 |
| MStainless steel | 120–160 | 0.07–0.15 |
| KCast iron | 130–210 | 0.07–0.15 |
Starting spindle speed: n = (1000 × Vc) / (π × D). For a Ø50 mm carbon steel bar at Vc = 170 m/min: n = (1000 × 170) / (3.14 × 50) ≈ 1080 rpm. At constant spindle speed, the cutting speed decreases to zero at the centerline, so enable constant surface speed (G96) with a spindle speed limit on a CNC lathe.
▲
Operating limitations
Do not part off bars larger than Ø50 mm: the head arm will contact the material before the cutting edge reaches the centerline. Keep tool post overhang as short as possible. Over the last 2 mm before the centerline, reduce the feed by as much as 75% and direct coolant straight into the cut. A 25 mm long blade deflects more easily than a short one, so start at the lower end of the feed range.
Installing the MGMN 400 insert in 3 steps
1Loosen
the BKTV M6x25 screw with the wrench AA5, 2–3 turns
2Seat
clean the pocket, slide the insert in until fully seated
3Tighten
and check that the cutting edge is on the lathe centerline ±0.1 mm
✓Ready
parting off bars up to Ø50 mm
Cutting insert not included
COMPATIBLE WITH:
| ✓ | MGMN 400 parting inserts (Smoxh: MGM. 4C) – width 4.0 mm, length 21 mm, height 4.8 mm |
| ✓ | BKTV M6x25 clamping screw (spare part) and AA5 wrench |
| ✓ | Left-hand version BDKT-L 2020 K4C T25 (SM38844) with the same dimensions |
Smoxh parting tools and boring bars for MGMN 400 inserts
BDKT R/L 2020 K4C T2020x20 mm | L 125 mm | T max 20 mm | Ø40 mmR right-hand
←L left-hand
→
←L left-hand
→
BDKT R/L 2020 K4C T T2020x20 mm | L 125 mm | T max 20 mm | Ø40 mmR right-hand
←L left-hand
→
←L left-hand
→
BDKT R/L 2525 K4C T2225x25 mm | L 150 mm | T max 22 mm | Ø44 mmR right-hand
←L left-hand
→
←L left-hand
→
BDKT R/L 2525 K4C T T2225x25 mm | L 150 mm | T max 22 mm | Ø44 mmR right-hand
←L left-hand
→
←L left-hand
→
BDKT R/L 2525 K4C T2525x25 mm | L 150 mm | T max 25 mm | Ø50 mmR right-hand
←L left-hand
→
←L left-hand
→
BDKT R/L 2525 K4C T T2525x25 mm | L 150 mm | T max 25 mm | Ø50 mmR right-hand
←L left-hand
→
←L left-hand
→
BDKT R/L 2525 K4C T4025x25 mm | L 170 mm | T max 40 mm | Ø80 mmR right-hand
←L left-hand
→
←L left-hand
→
BDKT R/L 3232 K4C T2232x32 mm | L 170 mm | T max 22 mm | Ø44 mmR right-hand
←L left-hand
→
←L left-hand
→
BIKT R/L 20 K4C T6Ø20 mm | Ømin 26 mm | L 170 mm | T max 6 mmR right-hand
←L left-hand
→
←L left-hand
→
BIKT R/L 25 K4C T7Ø25 mm | Ømin 32 mm | L 200 mm | T max 7 mmR right-hand
←L left-hand
→
←L left-hand
→
BIKT R/L 32 K4C T8Ø32 mm | Ømin 40 mm | L 250 mm | T max 8 mmR right-hand
←L left-hand
→
←L left-hand
→
BIKT R/L 40 K4C T10Ø40 mm | Ømin 50 mm | L 300 mm | T max 10 mmR right-hand
←L left-hand
→
←L left-hand
→
BIKT R/L 50 K4C T15Ø50 mm | Ømin 65 mm | L 350 mm | T max 15 mmR right-hand
←L left-hand
→
←L left-hand
→
Inserts from other grooving systems, such as DGN, GTN or KGM, do not fit the pocket. The 4 mm BDKT-R 2020 K4C T25 parting tool cuts carbon, alloy and stainless steel as well as cast iron, provided the insert grade matches the material. The limit remains a Ø50 mm bar. With parting off hardened steel reduce the speed to 70–130 m/min. In metalworking and fabrication shops, it parts off pins, spacers and bushings from bar stock.
Frequently asked questions
An MGMN 400 parting insert (in the Smoxh catalog: MGM. 4C) with a width of 4.0 mm, length of 21 mm, and height of 4.8 mm. It is double-ended, so one insert provides two cutting edges. DGN, GTN, and KGM inserts do not fit this pocket.
Ø50 mm, or twice the cutting depth T max = 25 mm. For larger bars, choose the 2525 K4C T40 version (up to Ø80 mm). Grooves shallower than 25 mm can also be cut on larger diameters.
The right-hand R version is standard: the workpiece is held in the chuck to the left of the tool. Choose the left-hand L version (code SM38844) when the workpiece is clamped on the opposite side of the tool or when the tool post arrangement on your lathe requires it. Both versions have identical dimensions.
A pip remains when the cutting edge is not on the lathe centerline. Set it within ±0.1 mm and check that the insert is fully seated in the pocket. Over the final 2 mm before the centerline, reduce the feed by as much as 75%.
Product accessories


Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you


Viewed products


This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.