





- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot
Description
CUTTING WIDTH4 mm
CUTTING DEPTH T MAX40 mm
MAX. BAR DIAMETERØ80 mm
INSERT · 2 EDGESMGMN 400
Parting tool 25X25 4 mm T40 Smoxh
Technical data for the holder for Korloy MGMN 400 inserts
| Technical data | |
|---|---|
| Designation | BDKT R 2525 K4C T40 |
| Type | holder for parting and external grooving |
| Shank height h | 25 mm |
| Shank width B | 25 mm |
| Overall length L | 170 mm |
| Dimension S (to the insert edge) | 25.4 mm |
| Cutting depth T max | 40 mm |
| Max. parting diameter D max | Ø80 mm |
| Insert pocket | MGM. 4C (MGMN 400, width 4 mm) |
| Hand | R – right-hand (left-hand version: SM25110) |

BDKT-R 2525 K4C T40 with screw clamping – operating principle
What this tool can do, screw clamping and a double-edged insert
Parting tool 4 mm BDKT-R 2525 K4C T40 (Smoxh) parts off bars up to Ø80 mm and cuts external grooves. It uses MGMN 400 carbide inserts clamped from above by the flexible lip of the head. The BKTV M6x25 screw tightens the lip, and the insert can be changed in a dozen or so seconds.
The insert edge projects 0.4 mm beyond the side of the shank (S = 25.4 mm with B = 25 mm). When cutting close to the chuck, only the cutting edge engages; the shank does not rub against the workpiece face. The 25x25 mm shank, 170 mm long, provides the rigidity required by a narrow cutting edge in an enclosed groove.
The head forms a thin blade 40 mm long, which determines the cutting depth T max. Behind the blade, the head widens to the full shank width and can no longer enter the 4 mm groove. This sets the limit: the tool parts off bars up to Ø80 mm, or twice T max.
The MGMN 400 insert is double-edged: when one edge becomes dull, rotate it by 180° and cut with the other end.
Parting and grooving with the BDKT-R 2525 K4C T40 tool – typical operations
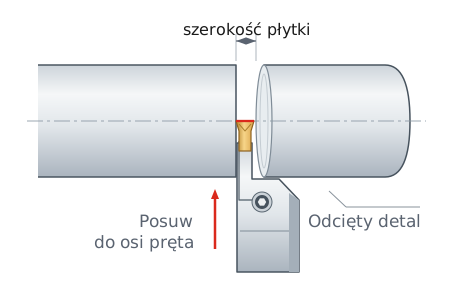
Parting – cutting a part off a bar
The blade enters the bar all the way to the axis and the part separates. Bars up to Ø80 mm, a 4 mm kerf, and material loss limited to the insert width.
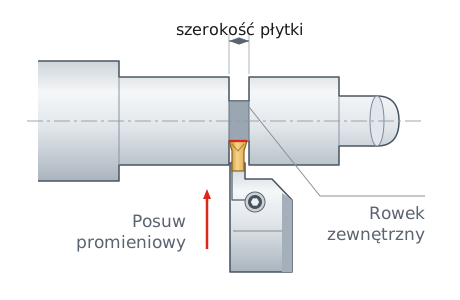
Cutting external grooves
A 4 mm groove between shaft shoulders or a retaining ring groove at the end of a journal, up to 40 mm deep. Cut wider grooves with several adjacent passes.

Screw clamping from above
The BKTV M6x25 screw draws the flexible lip of the head against the insert. Change the insert with an AA5 key without removing the tool from the tool post.

Double-edged insert
MGMN 400 has a cutting edge at both ends. One edge dull? Rotate the insert by 180° and use the other.

Material loss: 4 mm
Each parting cut turns only 4 mm of bar into chips. For 100 parts, this consumes 10 cm less bar than a tool with a 5 mm insert.
Dimensions and cutting reach – dimensional drawing
Side view and top view
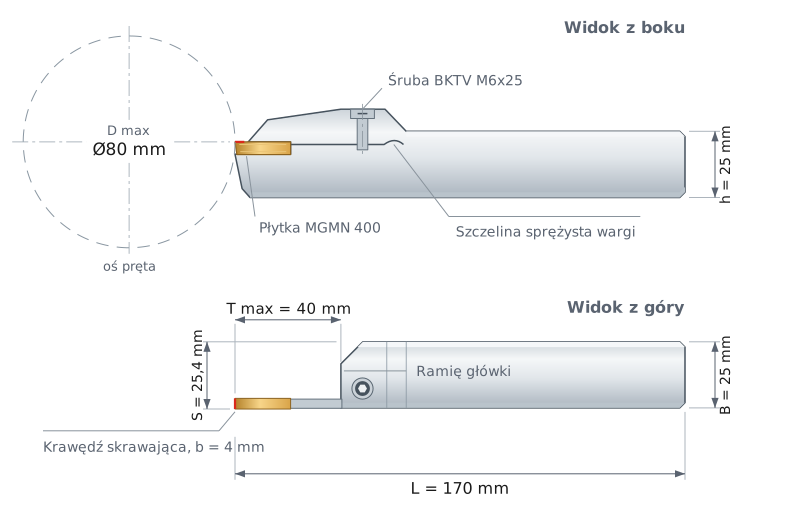

HEIGHT h
25 mm

WIDTH B
25 mm

LENGTH L
170 mm

DIMENSION S
25.4 mm
T max is measured from the insert tip to the head shoulder. A groove shallower than 40 mm can also be cut in a bar larger than Ø80 mm.
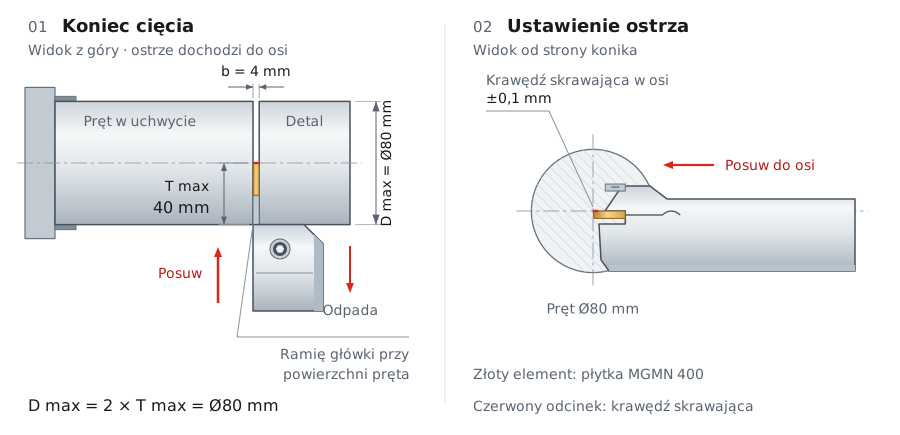
The left panel of the diagram shows the end of the cut: the insert tip is on the bar axis, and the head shoulder touches its surface. The right panel shows cutting edge height: set the edge on the centerline to within ±0.1 mm. Below the centerline, a pip remains; above the centerline, the cutting edge rubs against the material.
Decoding the BDKT R 2525 K4C T40 designation
Five elements of the Smoxh code, read from the left
Designation: BDKT R 2525 K4C T40
BDKT
Element 1
holder type
holder type
For parting
BDKT
BDKT
Smoxh series for external grooving and parting with screw clamping. The counterpart for internal grooving is designated BIKT.
R
Element 2
hand
hand
Right-hand
R
R
Standard configuration with the workpiece held in a chuck to the left of the tool. Version L is a mirror image – code SM25110.
2525
Element 3
shank
shank
25x25 mm
2525
2525
The first two digits indicate height h, and the next two indicate width B. Fits a tool post for 25 mm tools.
K4C
Element 4
insert pocket
insert pocket
MGM. 4C
K4C
K4C
K – Korloy MGMN insert system, 4 – cutting width of 4 mm. Versions K2C…K8C accept inserts from 2 to 8 mm.
T40
Element 5
depth
depth
T max 40 mm
T40
T40
Blade length from the insert tip to the head shoulder. Maximum parting diameter is 2 × T max = Ø80 mm.
Smoxh catalog convention, not ISO 5608 · dimensions: h 25 · B 25 · L 170 · S 25.4 mm
Parting data – speeds and feeds for a 4 mm insert
Starting values with coolant; refer to the insert grade data sheet for definitive data
The values apply to coated MGMN 400 inserts used with coolant. Use the higher speeds with rigid clamping and short overhang.
| Workpiece material | Vc [m/min] | fn [mm/rev] |
|---|---|---|
| PCarbon steel | 120–200 | 0.07–0.15 |
| PAlloy steel | 130–180 | 0.07–0.15 |
| PHardened steel | 70–130 | 0.07–0.12 |
| MStainless steel | 120–160 | 0.07–0.15 |
| KCast iron | 130–210 | 0.07–0.15 |
Starting spindle speed: n = (1000 × Vc) / (π × D). For a Ø80 mm carbon steel bar at Vc = 170 m/min: n = (1000 × 170) / (3.14 × 80) ≈ 680 rpm. At constant spindle speed, the cutting speed decreases to zero at the centerline, so enable constant surface speed (G96) with a spindle speed limit on a CNC lathe.
▲
Operating limitations
Do not part off bars larger than Ø80 mm: the head arm will contact the material before the cutting edge reaches the centerline. Keep tool post overhang as short as possible. Over the last 2 mm before the centerline, reduce the feed by as much as 75% and direct coolant straight into the cut. A 40 mm long blade deflects more easily than a short one, so start at the lower end of the feed range.
Installing the MGMN 400 insert in 3 steps
1Loosen
the BKTV M6x25 screw with the wrench AA5, 2–3 turns
2Seat
clean the pocket, slide the insert in until fully seated
3Tighten
and check that the cutting edge is on the lathe centerline ±0.1 mm
✓Ready
parting off bars up to Ø80 mm
Cutting insert not included
COMPATIBLE WITH:
| ✓ | MGMN 400 parting inserts (Smoxh: MGM. 4C) – width 4.0 mm, length 21 mm, height 4.8 mm |
| ✓ | BKTV M6x25 clamping screw (spare part) and AA5 wrench |
| ✓ | Left-hand version BDKT-L 2525 K4C T40 (SM25110) with the same dimensions |
Smoxh parting tools and boring bars for MGMN 400 inserts
BDKT R/L 2020 K4C T2020x20 mm | L 125 mm | T max 20 mm | Ø40 mmR right-hand
←L left-hand
→
←L left-hand
→
BDKT R/L 2020 K4C T T2020x20 mm | L 125 mm | T max 20 mm | Ø40 mmR right-hand
←L left-hand
→
←L left-hand
→
BDKT R/L 2020 K4C T2520x20 mm | L 125 mm | T max 25 mm | Ø50 mmR right-hand
←L left-hand
→
←L left-hand
→
BDKT R/L 2525 K4C T2225x25 mm | L 150 mm | T max 22 mm | Ø44 mmR right-hand
←L left-hand
→
←L left-hand
→
BDKT R/L 2525 K4C T T2225x25 mm | L 150 mm | T max 22 mm | Ø44 mmR right-hand
←L left-hand
→
←L left-hand
→
BDKT R/L 2525 K4C T2525x25 mm | L 150 mm | T max 25 mm | Ø50 mmR right-hand
←L left-hand
→
←L left-hand
→
BDKT R/L 2525 K4C T T2525x25 mm | L 150 mm | T max 25 mm | Ø50 mmR right-hand
←L left-hand
→
←L left-hand
→
BDKT R/L 3232 K4C T2232x32 mm | L 170 mm | T max 22 mm | Ø44 mmR right-hand
←L left-hand
→
←L left-hand
→
BIKT R/L 20 K4C T6Ø20 mm | Ømin 26 mm | L 170 mm | T max 6 mmR right-hand
←L left-hand
→
←L left-hand
→
BIKT R/L 25 K4C T7Ø25 mm | Ømin 32 mm | L 200 mm | T max 7 mmR right-hand
←L left-hand
→
←L left-hand
→
BIKT R/L 32 K4C T8Ø32 mm | Ømin 40 mm | L 250 mm | T max 8 mmR right-hand
←L left-hand
→
←L left-hand
→
BIKT R/L 40 K4C T10Ø40 mm | Ømin 50 mm | L 300 mm | T max 10 mmR right-hand
←L left-hand
→
←L left-hand
→
BIKT R/L 50 K4C T15Ø50 mm | Ømin 65 mm | L 350 mm | T max 15 mmR right-hand
←L left-hand
→
←L left-hand
→
Inserts from other grooving systems (DGN, GTN, KGM) use different pockets and do not fit this holder. The 4 mm BDKT-R 2525 K4C T40 parting tool parts off workpieces from bars up to Ø80 mm and cuts external grooves with a width of 4 mm. When the groove width is a fit dimension, choose an MGGN insert with a tolerance of ±0.025 mm. Groove depth is limited to T max = 40 mm. In maintenance work, it is useful for making replacement bushings, pins, and spacer rings.
Frequently asked questions
An MGMN 400 parting insert (in the Smoxh catalog: MGM. 4C) with a width of 4.0 mm, length of 21 mm, and height of 4.8 mm. It is double-ended, so one insert provides two cutting edges. DGN, GTN, and KGM inserts do not fit this pocket.
Ø80 mm, which is twice the cutting depth T max = 40 mm. This is the greatest cutting depth in the K4C series. Grooves shallower than 40 mm can also be cut on larger diameters.
Start at approximately 680 rpm for carbon steel, at Vc = 170 m/min with a 4 mm insert. Cutting speed decreases closer to the centerline, so use G96 constant surface speed with a spindle speed limit on a CNC lathe. For stainless steel, use Vc 120–160 m/min.
Up to 40 mm, which is the holder's T max. In a single pass, the groove width equals the insert width of 4 mm; wider grooves require several adjacent passes. For deep grooves, retract the insert every few millimeters to clear chips.
Product accessories


Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you


Viewed products


This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.