







- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot

Description
ThreadM6 × 1
Tolerance class6g
SetGO + NO-GO
StandardISO 1502
Technical specifications of the M6 × 1 thread ring gauge
Gauge set specifications according to ISO 1502
| Technical data | |
|---|---|
| Gauge type | GO + NO-GO thread ring gauge set |
| Thread | M6 × 1 mm |
| Tolerance class | 6g |
| Nominal diameter (d) | Ø6.000 mm |
| Pitch diameter (d2) | 5.350 mm |
| d2 range for 6g | 5.212 – 5.324 mm |
| Thread pitch (P) | 1.0 mm |
| Thread angle | 60° |
| Material | Tool steel, hardened |
| Hardness | 58–62 HRC |
| Gauge standard | ISO 1502 / DIN 2285 + DIN 2299 |
| Thread standard | ISO 965-1 / DIN 13-1 |
| Reference temperature | 20 °C |
| Manufacturer | Varel |
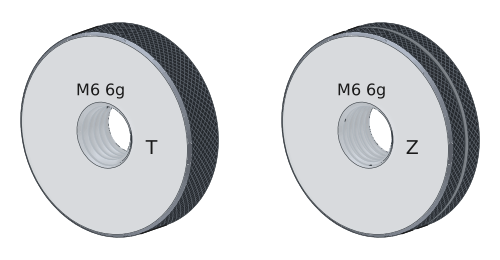
T
GO ring gauge — screwed on by hand along the full bolt thread.
Z
NO-GO ring gauge with a groove in the knurled surface — stops after no more than 2 turns.
The M6-6g engraving on the face of both rings indicates the size and tolerance class of the bolt being inspected.
Limit gauging principle: GO + NO-GO
Gauge for M6 external threads according to ISO 1502
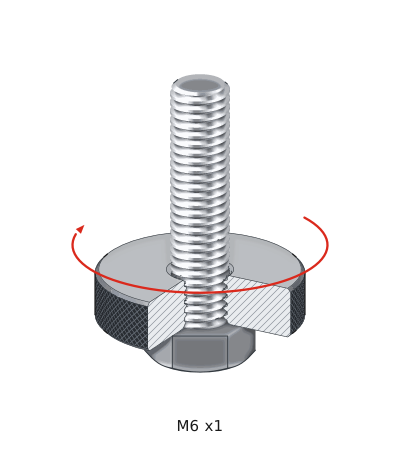
1
The GO ring gauge is screwed on by hand, without force, along the full thread of the M6 x1 bolt.
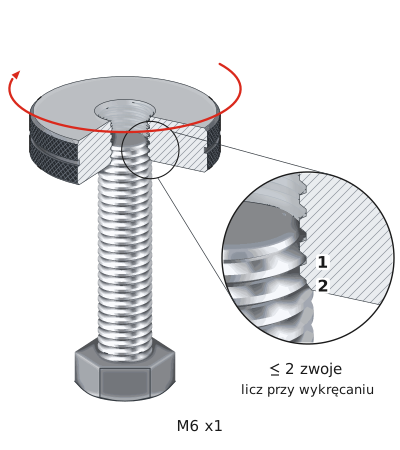
2
The NO-GO ring gauge stops after no more than 2 turns — turns are counted when unscrewing.
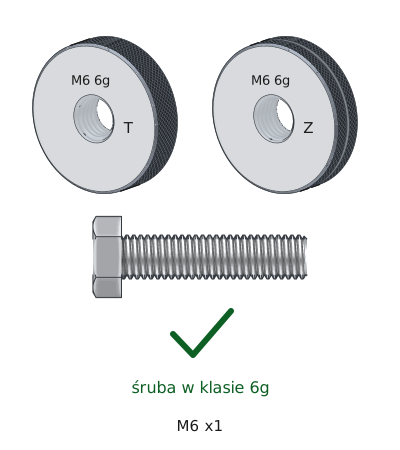
3
The GO ring gauge passed, NO-GO stopped — the bolt meets class 6g.
The ring gauge set M6 6g checks an external thread — on a bolt, stud or turned pin. The ring gauge GO must screw on by hand along the full thread length, while the ring gauge NO-GO may advance no more than 2 threads, counted when unscrewing. Only both results together confirm that the thread is neither oversized nor undersized.
This size range is typical for the production of machine bolts and studs. The ring gauge detects both a thread cut too deep and a thread deformed on a shaft — neither defect is visible to the naked eye. The 1 mm pitch is the coarse pitch for this diameter: the designation M6 without a specified pitch denotes this thread. For reference: the thread minor diameter M6 is 4.773 mm — this cross section determines the bolt's strength, while the gauge checks the pitch diameter.
The gauge GO has a full thread profile and checks the maximum material limit — pitch diameter, pitch and thread profile at the upper tolerance limit (for M6 6g: d2 max = 5.324 mm). It should screw freely onto the full length of the thread being inspected — without force or wrenches. The gauge NO-GO has a truncated profile with incomplete flanks and checks the minimum material limit (d2 min = 5.212 mm). According to ISO 1502 §7 it must not screw onto the thread more than 2 threads. Only meeting both conditions simultaneously confirms that the thread is within tolerance class 6g.
Thread inspection M6 × 1 — class 6g
1 GO gauge
screws on the full length: YES
2 NO-GO gauge
advances max. 2 turns: YES
✓ Conforming thread
class 6g confirmed
Inspection standard: ISO 1502 · Tolerances: ISO 965-1 · Dimensions: ISO 724 / DIN 13-1
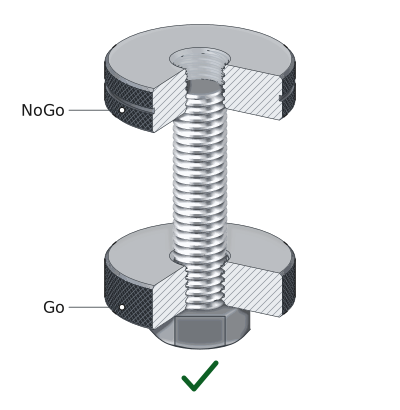
✓ Thread acceptable — GO screws onto the full thread, NO-GO stops.
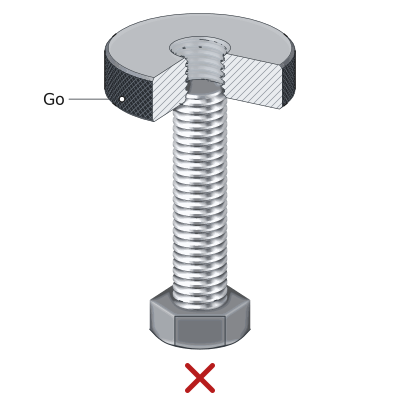
✗ Thread oversized — GO does not screw onto the bolt.
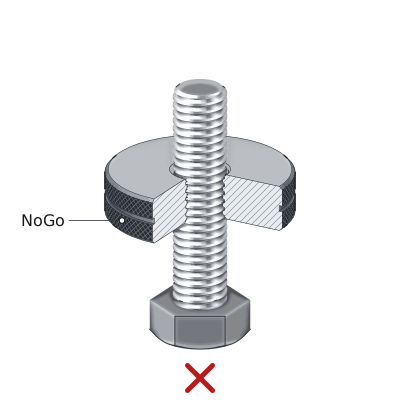
✗ Thread undersized — NO-GO screws on more than 2 turns.
Tolerance classes for an M6 × 1 external thread
Comparison according to ISO 965-1 for M6 × 1
Comparison of classes 4g, 6g, 6e and 8g
Basic pitch diameter d2 for the thread M6 is 5.350 mm. The deviations in the table are measured downward from this value.
| Class | d2 nominal [mm] | d2 permissible [mm] | Tolerance zone | Application | Status |
|---|---|---|---|---|---|
| 4g | 5.350 mm | 5.253 – 5.324 mm | 0.071 mm | Precision fit | |
| 6g | 5.350 mm | 5.212 – 5.324 mm | 0.112 mm | Standard fit — bolts, fasteners | THIS PRODUCT |
| 6e | 5.350 mm | 5.178 – 5.290 mm | 0.112 mm | Clearance fit — for electroplating | |
| 8g | 5.350 mm | 5.144 – 5.324 mm | 0.180 mm | Coarse fit — hot-rolled threads |
The full range of class 6g for the thread M6 is 0.112 mm: from 5.212 to 5.324 mm. Class 6g is the standard for general-purpose bolts — it mates with 6H nuts. Classes 4g and 5g reduce clearance in guiding joints, while 6e and 8g leave room for electroplating. The values in the table are pitch diameter d2, measured at half the profile height, not the thread major diameter.
Proper use and calibration
Maintaining gauge accuracy
Usage rules according to ISO 1502
Before measurement, the thread is cleaned of chips, burrs, oil and contaminants. The gauge is screwed on by hand only, without wrenches or externally applied torque (which increases wear and distorts the result). Reference inspection temperature: 20 °C. Gauges are stored in a dry place, protected with rust-preventive oil. The calibration interval is determined by the user based on usage intensity — ISO 1502 (clause 7.2.1) requires periodic gauge measurement but specifies neither the interval nor the number of measurements. ISO 1502 specifies thread ring gauge wear limits (wear limits); once these are exceeded, the gauge must be removed from service.
Varel set contents
Included in the set:
| ✓ | 1 × GO thread ring gauge — GO, full thread profile, checks the maximum material limit |
| ✓ | 1 × NO-GO thread ring gauge — NO-GO, truncated profile (max. 2 turns of engagement according to ISO 1502) |
| ✓ | Tool steel hardened to 58–62 HRC — high wear resistance |
| ✓ | Ground thread profiles — high measurement repeatability |
| ✓ | Compliance with ISO 1502 / DIN 2285 + DIN 2299 (gauges) and ISO 965-1 / DIN 13-1 (thread) |
Frequently asked questions
The principle of limit gauging requires verification of both the maximum and minimum material limits. The GO gauge confirms that the thread is not oversized (it screws on the full length), while the NO-GO gauge confirms that it is not undersized (it does not advance more than 2 turns according to ISO 1502). Using only one gauge leaves the other limit unchecked — the part may be outside tolerance class 6g despite passing a partial inspection.
The gauge GO has a full thread profile and represents the maximum material limit of the external thread being inspected (for M6 6g: d2 max = 5.324 mm). The gauge NO-GO has a profile that is truncated with incomplete flanks — it checks only the pitch diameter at the lower limit (d2 min = 5.212 mm) and has a shorter threaded length (usually 3 full turns). The design of both types is defined by ISO 1502 table 2.
The thread is nonconforming, if either condition occurs: the GO gauge does not screw on the full length (thread oversized — d2 above 5.324 mm) or the NO-GO gauge advances more than 2 turns (thread undersized — d2 below 5.212 mm). In either case, the part must be rejected or reworked. Reference standard: ISO 965-1 (tolerances), ISO 1502 (inspection procedure).
Product accessories


Fanar's M6 HSSE INOX 6g DIN 22 568 tooling
Reference: 0000007078 In stock < 10 items
€11.84
€14.57 brutto
Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you


This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.