 Polski






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot

Internal Micrometer 50-75 mm 0.01 mm MMWd
€71.21 tax inc.
Net price: €57.89
Description
Inside micrometer 50-75 mm – 0.01 mm resolution
Technical data and instrument construction
| Technical data | |
|---|---|
| Measuring range | 50-75 mm |
| Resolution | 0.01 mm |
| Micrometer screw pitch | 0.5 mm per revolution |
| Ratchet measuring force | 1-6 N |
| Measuring faces | cemented carbide, ground |
| Reading lock | locking screw |
| Included | adjusting wrench |
READOUT0.01 mm
FACEScemented carbide
MEASURING FORCE1-6 N
LOCKlocking screw
MMWd caliper-type micrometer – construction and applications
Applications for an instrument with this measuring range
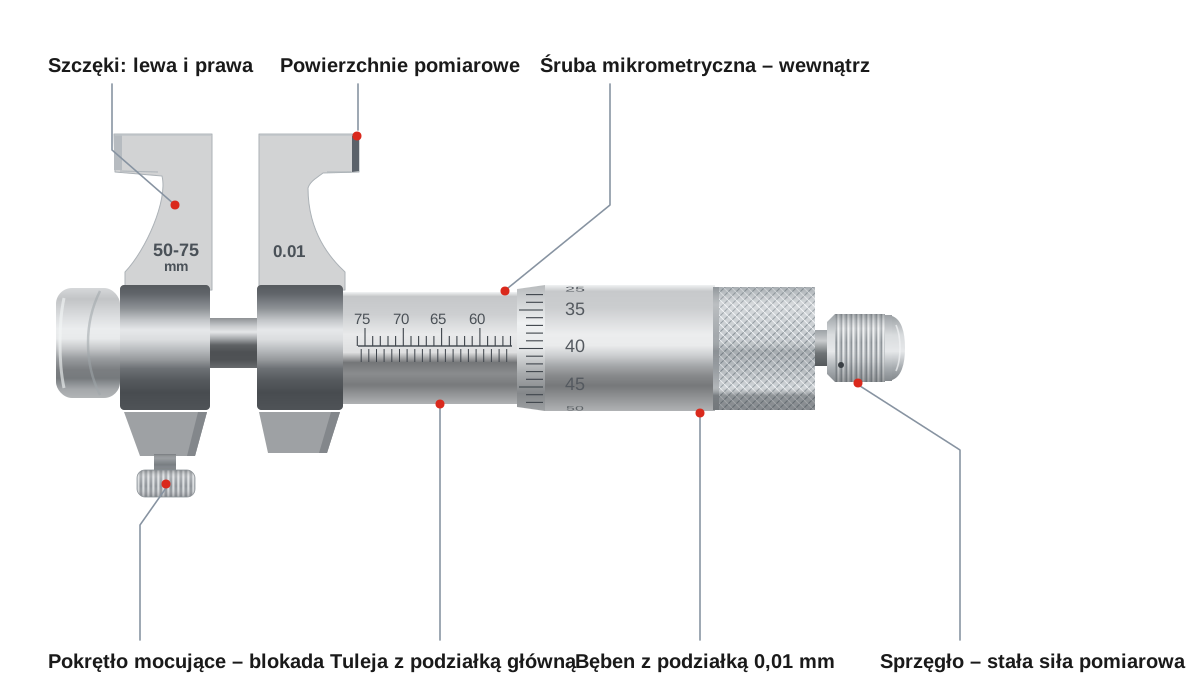
Inside micrometer 50-75 mm is an analog jaw-type instrument for measuring the diameters of bores, bushings, and bearing seats with a readability of 0.01 mm. The result is read directly from the scale, as on an outside micrometer, except that the jaws expand inside the bore. The micrometer screw has a pitch of 0.5 mm, providing 50 divisions of 0.01 mm per thimble revolution.
The ground cemented carbide measuring faces resist wear. The ratchet maintains a measuring force of 1-6 N for repeatable jaw contact, while the locking screw holds the indication during reading. The jaws reach approximately 10 mm into the bore, so measurements are taken near the edge — diameters deeper inside a bore are measured with a bore micrometer.
Typical applications:
- measuring bore and bearing seat diameters within the 50-75 mm range,
- inspecting cylinder liners and guides after boring and reaming,
- measuring wide grooves and recesses in machine housings,
- maintenance, toolrooms, and quality control stations.
How to read the measurement
Sleeve and thimble scales step by step
Sleeve
62.50
+
Thimble
0.32
=
Measurement result
62.82 mm
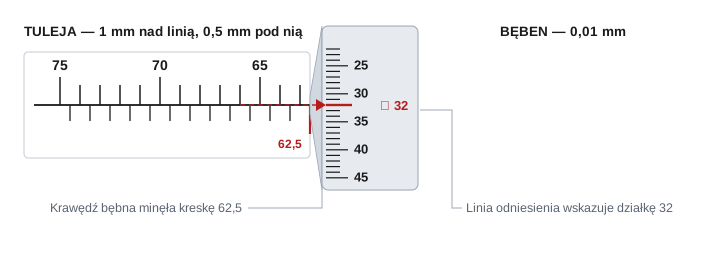
The result consists of two readings. Whole and half millimeters are read on the sleeve — the whole-millimeter marks are above the reference line, and the 0.5 mm marks are below it. The sleeve numbering runs in the opposite direction to an outside micrometer because the dimension increases as the jaws expand. Hundredths of a millimeter are read on the thimble at the reference line. In the illustrated example, the thimble edge has passed the 62.5 mark, and the reference line indicates division 32, giving a result of 62.82 mm.
Steel expands by approximately 11.5 µm per meter for a temperature change of 1°C. A bore with a diameter of 75 mm that is 10°C warmer than the instrument is approximately 0.009 mm larger — almost a full scale division. The larger the diameter, the more important it is to equalize the temperatures of the workpiece and instrument before measuring.
Find the maximum reading and do not force the ratchet
Measuring along a chord gives a reading that is too low — gently rock the instrument across the bore cross section; the correct diameter is the maximum reading in the plane perpendicular to the axis. Expand the jaws only with the ratchet until it starts to slip — excessive force distorts the result and accelerates wear of the measuring faces.
Zero setting and accessories
Preparing for the first measurement
INCLUDED:
| ✓ | adjusting wrench for sleeve adjustment during zero setting |
The set includes an adjustment wrench, but no standard. Check the zero point using a setting ring or another standard with a known dimension within the 50-75 mm range, and correct any deviation by turning the sleeve with the wrench. Perform the check at a temperature close to 20°C and repeat it whenever the instrument is dropped.
The 50-75 mm inside micrometer combines 0.01 mm readability with constant ratchet force and a reading lock. The carbide measuring faces withstand years of daily use at the machine tool. This tool is intended for all tasks where bore diameter measurement a caliper is no longer sufficient.
Frequently asked questions
No — the jaws reach approximately 10 mm into the bore, so the instrument measures the diameter near the edge. To inspect deeper sections, for example in a long cylinder liner, use a bore micrometer that can be inserted to any depth in the bore.
Check the zero point using a setting ring or another standard with a known, marked dimension within the 50-75 mm range. Open the jaws inside the standard using the ratchet, compare the reading with the standard's dimension, and correct the difference by turning the sleeve with the adjustment wrench. Perform the check at a temperature close to 20°C.
The result is read directly from the scale, without setting before measurement. A three-point bore micrometer centers itself in the bore and can be more accurate, but covers a narrow range and requires a setting ring; a two-point model must be rocked in the bore. A jaw-type instrument is faster for in-process inspection.
Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you


This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.