







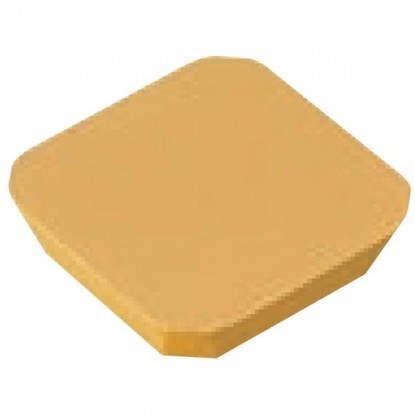


Net price: €5.26
Description
| Technical data | |
|---|---|
| Side length l | 12 mm |
| Insert thickness s | 3.18 mm |
| Shape | square (S), 4 edges |
| Entering angle κ | 45° |
| AFTN code | 25° chamfer, chamfered edge, symmetrical |
| Mounting | without a hole, top clamp |
| ANSI code | SEKN 42AFTN |
| Manufacturer | YG-1 |
face milling with a 45° milling head — ISO P and M groups, conservative values
| Material | Vc [m/min] | Feed fz [mm/tooth] | ap [mm] | ae [% D] |
|---|---|---|---|---|
| PStructural steel | 150–220 | 0.10–0.22 | 0.5–3.0 | 60–80 |
| MStainless steel | 80–140 | 0.08–0.18 | 0.3–2.0 | 50–70 |
square without a hole, with a chamfered edge for 45° face milling
Milling insert SEKN 1203 AFTN from YG-1 is a square cemented carbide indexable insert designed for face milling steel and stainless steel. Shape S, a square with four equal sides, provides 4 cutting edges and symmetrical cutting action in the milling head. AFTN is the manufacturer's geometry code; the meaning of its letters requires the YG-1 data sheet. The insert has no mounting hole, so it is secured with a top clamp or wedge in a suitable milling head pocket.
The insert is suitable for face milling end surfaces, machining flanges and face milling structural steel housings and stainless steel components. Calculate the milling head speed using n = 1000 × vc / (π × D), where vc is the cutting speed. For a milling head with a diameter of 63 mm and five inserts at a cutting speed of 180 m/min, the result is approximately 910 rpm. With a feed per tooth (fz) of 0.15 mm, the table feed rate is vf = fz × z × n, or approximately 683 mm/min. For stainless steels, reduce the cutting speed to 80–140 m/min and maintain a constant feed to limit work hardening of the layer being cut.
The chamfered edge at the corner requires stable insert seating and parameters within the conservative table for 45° face milling. Climb milling produces less friction and longer edge life, so it is preferred on CNC machines with no table backlash. Select a depth of cut ap of a few millimeters per pass and apply a continuous coolant stream to stabilize the temperature during interrupted cutting. Four edges and symmetrical N geometry reduce the cost per machined surface because one insert can be used in heads with either direction of rotation.
The insert has no mounting hole — it fits only face mills with a top clamp or wedge and a pocket for SEKN / SEKN 42. It cannot be installed in a central screw pocket for inserts with a hole (APKT, SEKT). The YG-1 carbide grade is not specified in the data — for hardened materials above 45 HRC confirm the selection in the manufacturer's data sheet.
how to read the SEKN 1203 AFTN code — positions 1–10 of the designation
Designation SEKN 1203 AFTN according to the standard ISO 1832: 4 letters describe the geometry and construction, 2 numeric codes describe the dimensions, and the suffix AFTN — the wiper edge geometry. Each field has a number, an icon and a brief description.
ISO 1832 designation decoder — how to read the code
Positions 1–3 · ISO code
1SShape
Square 90°
4 corners of 90° per side
2EClearance angle
α = 20°
positive, single-sided
3KTolerance
Class K (precision)
ground thickness ±0.025 mm
Positions 4–6
4NType
Without hole or chip breaker
clamp or wedge mounting
512Size
l = 12 mm
IC = 12 mm (square: IC = l)
603Thickness
s = 3.18 mm
between rake faces
AFTN suffix · wiper edge
7AEntering angle
κ = 45°
45° angle milling cutters and milling heads
8FWiper land
α′ = 25°
wiper land clearance angle
9TEdge condition
Chamfered (T-land)
the chamfer strengthens the edge during roughing
10NHand
Right-hand and left-hand
symmetrical design
✓ 4 corners × 1 side = 4 cutting edges
pocket for SEKN / SEKN 42 — clamping without a hole
| Compatibility | Applications and clamping |
|---|---|
| ✔ | 45° face mills with a pocket for SEKN / SEKN 42 |
| ✔ | Top clamp or wedge clamping — insert without a hole |
| ✔ | Face milling and end-face milling of steel (ISO P) and stainless steel (ISO M) |
| ✔ | Use in right-hand and left-hand cutting heads — symmetrical N geometry |
| ✗ | Central screw pockets for inserts with a hole (APKT, SEKT) |
| ✗ | 90° shoulder milling heads (APKT/TPKN) and 75° face mills (SPKN) — different entering angle |
| ✗ | Slot milling at full axial engagement — face milling insert, not for plunging |
edges, AFTN designation, materials and clamping
Four — the square S shape has 4 corners, and the symmetrical N geometry allows the insert to be used in right-hand and left-hand cutting heads. When a corner is worn, index the insert in the milling head pocket to the next edge without replacing the holder.
AFTN is the manufacturer's geometry code. The meaning of each letter must be checked in the YG-1 data sheet; it is not decoded using the designation decoder for another insert family.
For structural steels (ISO P) at a cutting speed of 150–220 m/min and for stainless steel (ISO M) at 80–140 m/min. The insert is designed for face milling with a 45° milling head, not for axial plunging.
No — type N indicates an insert without a hole or chip breaker. It is secured with a top clamp or wedge in a face mill with a pocket for SEKN / SEKN 42; it does not fit central screw pockets.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


