







Description
Tool specifications and replaceable inserts
| TECHNICAL DATA | |
|---|---|
| Tool type | Indexable T-slot cutter |
| Standard | – |
| Cutting diameter D | Ø25 mm |
| Cutting section width b | 11 mm |
| Neck diameter d1 | Ø12 mm |
| Shank diameter d | Ø25.0 mm |
| Overall length L | 100 mm |
| Number of inserts z | 4 |
| Interchangeable inserts | CCMT 0602rr |
| Material | steel body, carbide inserts |
| T-slot | 14 mm per DIN 650 |

Body, inserts and clamping
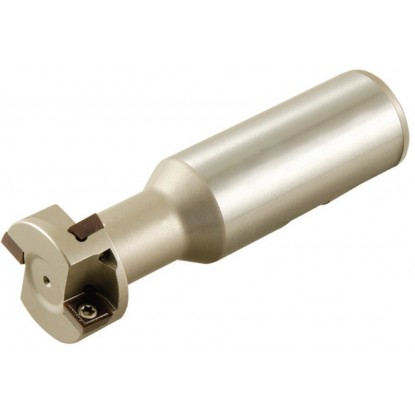
The 25x11 mm indexable T-slot cutter uses 4 carbide inserts in size CCMT 0602rr. The body with its Ø25.0 mm shank lasts for years – only worn inserts are replaced, with no resharpening or loss of disc dimensions. The Ø25 mm disc, 11 mm thick, forms the T-profile of the slot.
Each CCMT 0602rr insert is held by its own screw. The last two digits of the designation (rr) indicate the corner radius – specify the required value when ordering, e.g., 04 for r = 0.4 mm. Before installation, remove chips from the insert pocket – a particle beneath the insert raises it by hundredths of a millimeter, compromises the slot dimensions and causes the cutting edge to fracture under load. Tighten the screw to the torque specified in the manufacturer's data sheet: overtightening shears off the head, while a loose screw allows the insert to fall out into the slot. Carbide withstands speeds many times higher than HSS but requires rigid clamping and a constant feed.
Machining allowances and tool entry
The disc dimensions match a 14 mm T-slot per DIN 650 – the lower section of the slot is 23–25 mm wide and 9–11 mm high. The cutter removes 4.50 mm from each side of the straight slot previously machined with an end mill. The tool enters the material only along the existing slot; the Ø12 mm neck has no cutting edges and does not cut axially.
Clamping: Ø25.0 mm straight shank – a holder with a bore of this diameter is required, as the ER-32 collet range ends at Ø20 mm. The cutting speed is selected according to the insert grade, not the body – values are provided in the insert manufacturer's grade data sheet. Do not use HSS cutter settings: carbide settings are several times higher and require a rigid machine when cutting with the full disc width.
Spindle speed, feed and selection by insert grade
| Workpiece material | vc [m/min] | fz [mm/tooth] | n [rpm] | vf [mm/min] |
|---|---|---|---|---|
| P Structural and alloy steel | 130–200 | 0.07–0.14 | 1655–2546 | 463–1426 |
| M Stainless steel 304 / 316 | 70–100 | 0.07–0.14 | 891–1273 | 249–713 |
| K Gray cast iron GG20–GG30 | 150–250 | 0.07–0.14 | 1910–3183 | 535–1782 |
| N Aluminum, brass | 200–350 | 0.07–0.14 | 2546–4456 | 713–2495 |
Spindle speed is calculated in the same way as for HSS tools, but with a higher cutting speed. For vc = 130 m/min and a diameter of 25 mm, the result is n = 1000 × 130 / (π × 25) ≈ 1655 rpm, and the feed rate with 4 inserts and fz = 0.07 mm is vf ≈ 463 mm/min. For stainless steel, reduce to vc = 70–100 m/min as shown in the table above.
Inserts, clamping and slot
Carbide inserts in size CCMT 0602rr, 4 pcs per tool. The grade is selected according to the workpiece material – the same body accepts inserts for steel and cast iron.
In a holder with a Ø25.0 mm bore. An ER-32 collet does not accommodate this diameter – its range ends at Ø20 mm.
A slot 14 mm per DIN 650: the lower section of the slot is 23–25 mm wide and 9–11 mm high. The cutter removes 4.50 mm from each side.
No. Like any T-slot cutter, it must travel along a previously machined straight slot – the Ø12 mm neck has no cutting edges. Machine the straight slot to full depth with an end mill.

Reference: 0000006504 In stock > 10 items
€3.88 brutto

Reference: 0000005754 In stock > 10 items
€3.88 brutto
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


