





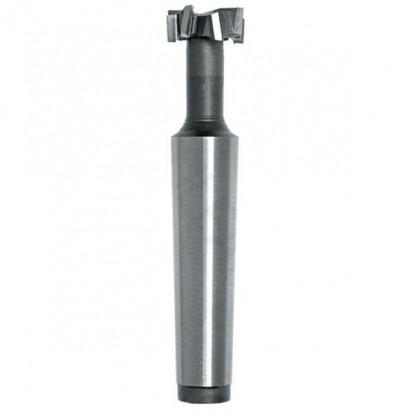

Description
Tool specifications and Morse taper
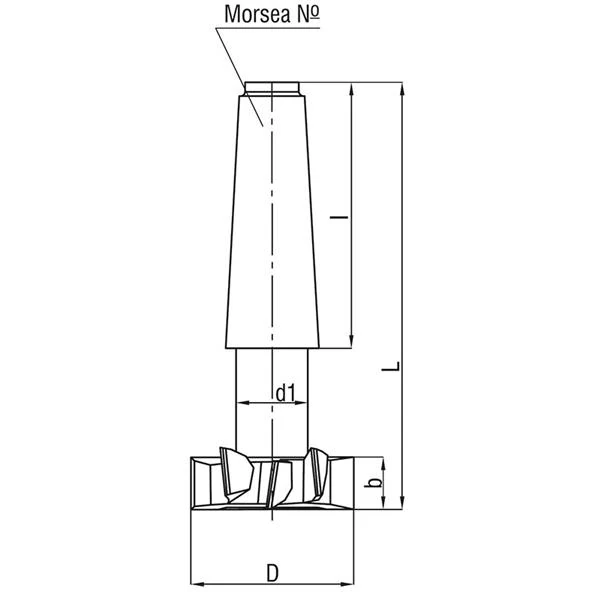
| TECHNICAL DATA | |
|---|---|
| Tool type | T-slot cutter NFRg |
| Standard | DIN 851 BN |
| Cutting diameter D | Ø72 mm |
| Cutting section width b | 35 mm |
| Neck diameter d1 | Ø36 mm |
| Shank | Morse taper MT5 |
| Shank length l | 136 mm |
| Overall length L | 248 mm |
| Number of cutting edges z | 12, straight teeth |
| Material | HSS |
| T-slot | 42 mm per DIN 650 |
Disc, neck and clamping
T-slot cutter NFRg 72x35 mm per DIN 851 BN is a tool for large T-slots in milling machine tables and fixture plates. The Ø72 mm disc, 35 mm thick, cuts with 12 cutting edges, and torque is transmitted by Morse taper MT5 with a drawbar thread – not a collet.
Allowances and machine requirements
The disc dimensions match a 42 mm T-slot per DIN 650: the lower portion of the slot is 68–72 mm wide and 32–35 mm high, with an overall depth of 74–85 mm. The cutter removes 13 mm of material from each side of the straight slot previously machined with an end mill. With a diameter of 72 mm and a Ø36 mm neck, the tool requires a rigid milling machine – torque at the disc is several times higher than with small T-slot cutters.
At a diameter of 72 mm, spindle speed is low: for vc = 25 m/min, it is approximately 111 rpm, and the feed rate with 12 cutting edges and fz = 0.035 mm is approximately 47 mm/min. Operation at such low speeds requires a machine with a rigid spindle and table – vibration with a disc this size chips the cutting edges faster than excessive feed loading. The taper and socket must be clean, as tool runout increases with overhang.
Clamping: Morse taper MT5 with a drawbar thread – the tool mounts directly in the milling machine spindle or in a reduction sleeve. The taper must be clean and dry – a chip between the taper and socket increases runout and damages both components. Guide the tool only through a previously machined straight slot; axial entry breaks the Ø36 mm neck. Uncoated HSS works in materials up to approximately 275 HB.
Conservative values by ISO 513 groups
| Workpiece material | vc [m/min] | fz [mm/tooth] | n [rpm] | vf [mm/min] |
|---|---|---|---|---|
| P Structural steel up to 275 HB | 20–30 | 0.025–0.050 | 88–133 | 26–80 |
| P Quenched and tempered alloy steel | 15–25 | 0.025–0.050 | 66–111 | 20–67 |
| M Stainless steel 304 / 316 | 9–18 | 0.025–0.048 | 40–80 | 12–46 |
| K Gray cast iron | 18–30 | 0.025–0.060 | 80–133 | 24–96 |
| N Aluminum, brass | 25–50 | 0.025–0.065 | 111–221 | 33–172 |
Use vc = 25 m/min. Spindle speed: n = 1000 × 25 / (π × 72) ≈ 111 rpm. Feed rate with 12 cutting edges and fz = 0.035 mm: vf = 111 × 0.035 × 12 ≈ 47 mm/min. The disc cuts across its full width in an enclosed channel, so supply plenty of coolant along the slot to flush out chips.
Clamping, slot and operation sequence
Directly in the milling machine spindle socket with an MT5 taper or in a reduction sleeve. The thread at the end of the taper is used to secure the tool with a drawbar – at this disc diameter, taper friction alone is insufficient.
A slot 42 mm per DIN 650 – the lower portion of the slot is 68–72 mm wide and 32–35 mm high. The cutter removes 13 mm from each side of the straight slot.
No. First machine a straight slot to the full depth of 74–85 mm with an end mill, then widen it with this cutter along the slot, and finish with a 45° chamfer at the opening.
12 – with a disc diameter of 72 mm, this provides a fine pitch and smooth operation, but always calculate the feed rate from the feed per tooth: vf = fz × z × n.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


