





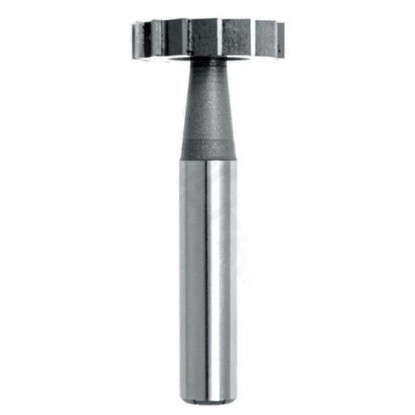

Description
Tool specifications
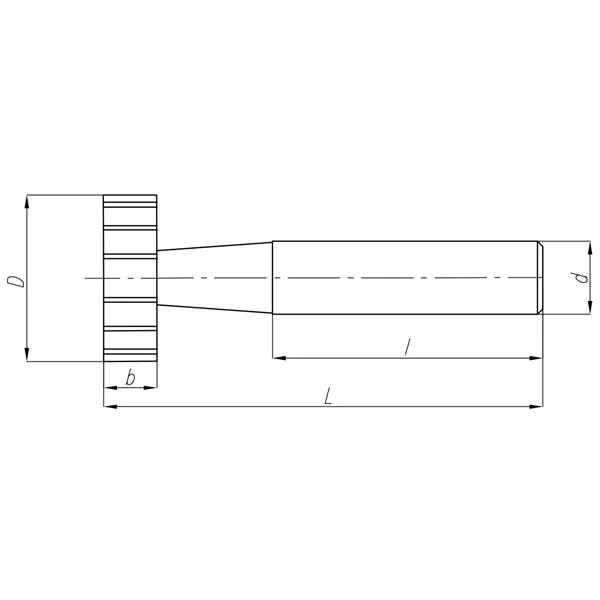
| TECHNICAL DATA | |
|---|---|
| Tool type | NFRh shank-type milling cutter |
| Standard | DIN 850 A |
| Cutting diameter D | Ø32.5 mm |
| Cutting section width b | 6.0 mm |
| Shank diameter d | Ø12.0 mm |
| Shank length l | 45 mm |
| Overall length L | 71.0 mm |
| Number of cutting edges z | 6, straight teeth |
| Material | HSS |
Tool construction and application limits
T-slot cutter 32.5x6.0 mm per DIN 850 A (type NFRh) cuts slots 6.0 mm wide in shafts and flat workpieces. The plunged Ø32.5 mm disc leaves a slot with an arcuate bottom and a radius of 16.25 mm.
The disc cuts with six straight cutting edges around its periphery and on its faces, so the slot width matches the 6.0 mm thickness. With no cutting edges on the neck, the tool cannot enter axially – attempting to plunge it like a drill breaks the neck.
The plunged disc leaves a slot with an arcuate bottom and a radius of 16.25 mm. Its length depends on depth: for t = 5 mm, the arc chord is l = 2√(t × (D − t)) ≈ 23.5 mm. The same cutter therefore produces slots of different lengths – controlled by plunge depth, not longitudinal feed.
Tool application range
The 6.0 mm width and Ø32.5 mm diameter do not match a Woodruff key size in DIN 6888 – this is a tool for grooves and slots: grooves for retaining rings and seals, lubrication grooves, slots for sheet metal and pins, and cutting through thin walls. Select the plunge depth to suit the required slot length, not the tool diameter – with the full disc width engaged, each additional millimeter of penetration increases cutting forces and neck loading.
Clamping: collet ER-32 with an insert for Ø12.0 mm. A drill chuck will not hold the tool with the disc fully engaged. Uncoated HSS works up to approximately 275 HB; above this, use the HSSE (HSS-Co5) version.
Conservative values by ISO 513 groups
| Workpiece material | vc [m/min] | fz [mm/tooth] | n [rpm] | vf [mm/min] |
|---|---|---|---|---|
| P Structural steel up to 275 HB | 20–30 | 0.025–0.050 | 196–294 | 29–88 |
| P Quenched and tempered alloy steel | 15–25 | 0.025–0.050 | 147–245 | 22–74 |
| M Stainless steel 304 / 316 | 9–18 | 0.025–0.048 | 88–176 | 13–51 |
| K Gray cast iron | 18–30 | 0.025–0.060 | 176–294 | 26–106 |
| N Aluminum, brass | 25–50 | 0.025–0.065 | 245–490 | 37–191 |
Use vc = 25 m/min. Spindle speed: n = 1000 × 25 / (π × 32.5) ≈ 245 rpm. Feed rate with 6 cutting edges and fz = 0.035 mm: vf = 245 × 0.035 × 6 ≈ 51 mm/min. The disc cuts across its full width in an enclosed channel, so supply plenty of coolant along the slot to flush out chips.
Applications, clamping and cutting data
For grooves and slots 6.0 mm wide – grooves for retaining rings and seals, lubrication grooves, recesses for sheet metal, and cutting through thin walls.
collet ER-32 with an insert for Ø12.0 mm. The plain straight shank has no clamping flat, so a drill chuck is unsuitable.
Apply plenty of emulsion along the slot to flush chips out. If pressurized coolant is unavailable, use short passes and retract the tool to remove chips.
Yes, and it runs fastest in this material: vc 25–50 m/min. Aluminum adheres to the cutting edge, so apply plenty of coolant and do not stop the feed in the slot – a built-up edge compromises slot size.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


