







Description
Tool specifications and slot size
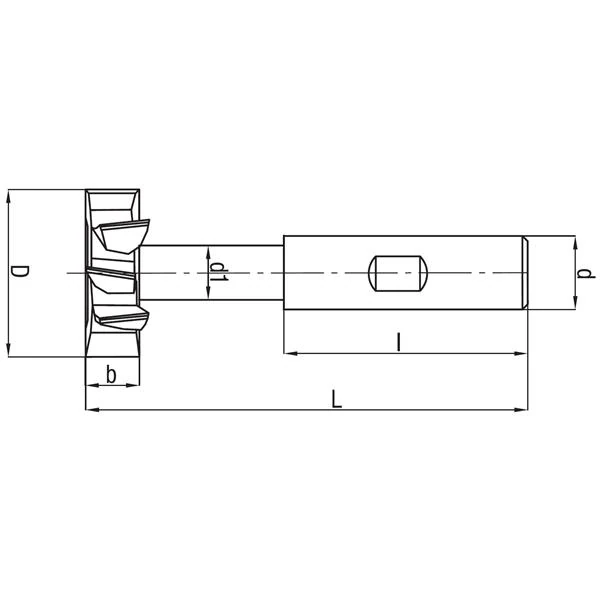
| TECHNICAL DATA | |
|---|---|
| Tool type | T-slot cutter NFRs |
| Standard | DIN 851 |
| Cutting diameter D | Ø12.5 mm |
| Cutting section width b | 6.0 mm |
| Neck diameter d1 | Ø5.5 mm |
| Shank diameter d | Ø12.0 mm |
| Shank length l | 40 mm |
| Overall length L | 57 mm |
| Number of cutting edges z | 6, straight teeth |
| Material | HSS |
| T-slot | 6 mm per DIN 650 |
Disc, neck and operating method
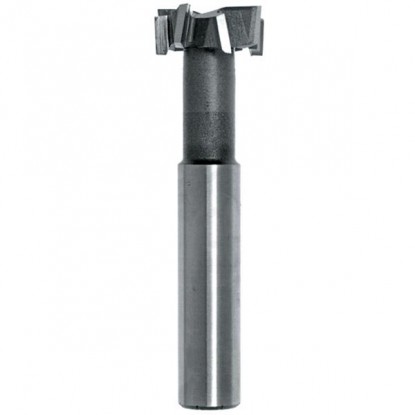
T-slot cutter NFRs 12.5x6.0 mm per DIN 851 widens the lower portion of the slot to a “T” profile in milling machine tables, fixture plates and pallets. The Ø12.5 mm disc, 6.0 mm thick, cuts with its periphery and both faces, while the narrower neck guides it through the previously machined slot.
The disc diameter determines the width of the lower portion of the slot, and the 6.0 mm thickness determines its height. The tool cuts with its periphery and both faces at once, so cutting forces increase with every millimeter of entry into the material. Maintain a constant feed without stopping in the slot: dwelling under load wears the cutting edge and leaves a polished mark on the wall. For vc = 25 m/min, the spindle speed is approximately 637 rpm.
Operation sequence and allowances
The dimensions of the NFRs 12.5x6.0 mm cutter match a 6 mm T-slot per DIN 650: the lower section of the slot is 11–12.5 mm wide and 5–6 mm high, with an overall depth of 11–13 mm.
A T-slot is produced in three operations. First, machine a straight slot to full depth with an end mill or slotting cutter per DIN 327. Then widen the lower portion with this cutter, feeding it along the existing slot. The cutter removes 2.50 mm of material from each side of the previously machined straight slot. Finally, a 45° chamfer at the slot entrance. A T-slot cutter does not cut axially – the neck has no cutting edges, so plunging into solid material breaks it off.
The tool works only in a previously machined guide slot; the neck, smaller in diameter than the disc, transmits all the cutting torque and is the weakest component. Clamping: collet ER-32 with an insert for Ø12.0 mm. Uncoated HSS machines materials up to approximately 275 HB – cast iron and structural steel tables fall within this range.
Conservative values by ISO 513 groups
| Workpiece material | vc [m/min] | fz [mm/tooth] | n [rpm] | vf [mm/min] |
|---|---|---|---|---|
| P Structural steel up to 275 HB | 20–30 | 0.015–0.030 | 509–764 | 46–138 |
| P Quenched and tempered alloy steel | 15–25 | 0.015–0.030 | 382–637 | 34–115 |
| M Stainless steel 304 / 316 | 9–18 | 0.015–0.038 | 229–458 | 21–104 |
| K Gray cast iron | 18–30 | 0.018–0.038 | 458–764 | 49–174 |
| N Aluminum, brass | 25–50 | 0.015–0.040 | 637–1273 | 57–306 |
Use vc = 25 m/min. Spindle speed: n = 1000 × 25 / (π × 12.5) ≈ 637 rpm. Feed rate with 6 cutting edges and fz = 0.022 mm: vf = 637 × 0.022 × 6 ≈ 84 mm/min. The disc cuts across its full width in an enclosed channel, so supply plenty of coolant along the slot to flush out chips.
Slot selection, operation sequence, clamping
The dimensions of the NFRs 12.5x6.0 mm cutter match a 6 mm T-slot per DIN 650: the lower section of the slot is 11–12.5 mm wide and 5–6 mm high, with an overall depth of 11–13 mm.
No. The neck between the disc and the shank has no cutting edges, so the tool must travel along a previously machined straight slot. Axial plunging breaks off the neck.
An end mill or slotting cutter per DIN 327 – to the full slot depth and the width of its upper opening. Only then is the T-slot cutter used.
collet ER-32 with an insert for Ø12.0 mm.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


