






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot
Description
FIRST GROOVE · D min–D maxØ24–36 mm
INSERT WIDTH3 mm
AXIAL DEPTH T MAX17 mm
SHANK h × B25 × 25 mm
Face grooving tool – BDAT-R Smoxh
Type A · right-hand version · MGM. 3C insert seat
| Technical data | |
|---|---|
| Catalog designation | BDAT-R 2525 K3C (Ø24–36) T17 |
| Manufacturer's code | SM10543 |
| Operation | face grooving |
| Design | type A |
| Hand | right-handed |
| Shank h × B | 25 × 25 mm |
| Length L | 150 mm |
| Head dimension S | 26.5 mm |
| First plunge diameter D min | 24 mm |
| First plunge diameter D max | 36 mm |
| Axial depth T max | 17 mm |
| Insert width b | 3 mm |
| Insert pocket | MGM. 3C / MGMN 300 |
| Clamp screw | BKTV M8×1×25-9232 |
| Wrench | SAK-AA4-9903 |

Illustration of the type A family; the variant designation in the photo is for reference only.
Face grooving tool BDAT-R 2525 K3C (Ø24–36) T17 cuts annular grooves in the workpiece face. Select this type A variant for a first plunge within the Ø24–36 mm range. Clamp the 25 × 25 mm shank in a holder that allows it to be aligned parallel to the spindle axis.
Face grooving – type A setup
Shank position, spindle axis and cutting edge plunge direction
In type A, the working section is aligned along the shank. The plunge feed runs parallel to the spindle axis. Correct holder orientation provides access to the face and clearance for the curved working section between the groove walls.
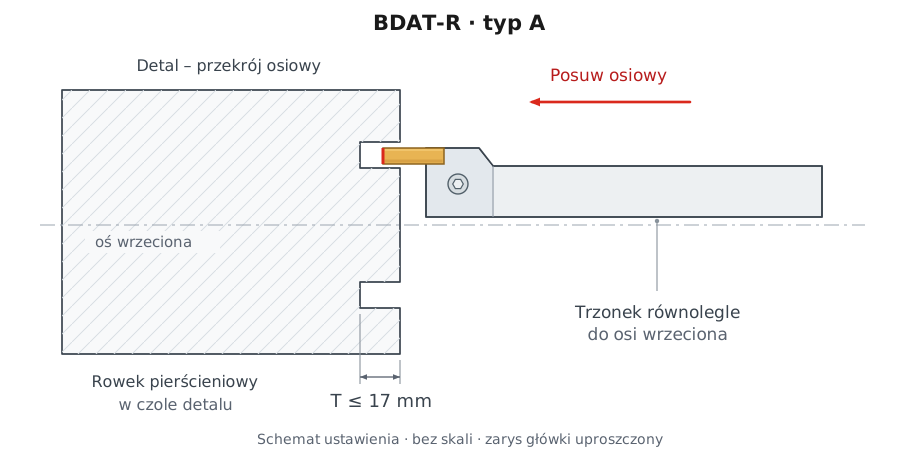
Typical applications include face seal seats in covers, sleeves and housings. Match the groove width, corner radius and depth to the workpiece documentation. The 3 mm insert determines the nominal width of a single plunge; the machining tolerance also depends on the insert and machining conditions.

Screw clamp
The seat locates the insert, and the clamp holds it during cutting.

Double-edged insert
When one end is worn, rotate the insert by 180° and use the other end.
First groove diameter and holder dimensions
Diameter selection range, width b and axial depth T
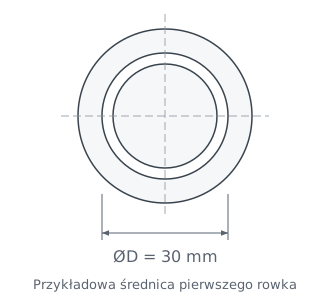
D min = 24 mm and D max = 36 mm define the first plunge diameter range of Ø24–36 mm. This is neither the outside diameter of the entire workpiece nor the width of the finished groove. When widening the groove, check the permitted insert movements and head clearance; the difference D max − D min does not define the machining width.
Front view
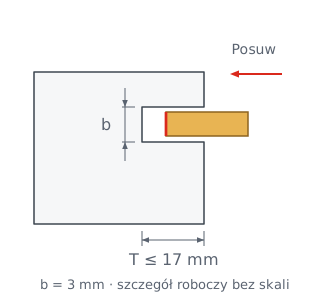
Depth and width
DIAMETER D min24 mm
DIAMETER D max36 mm
AXIAL DEPTH T max17 mm
Depth T is measured from the workpiece face along the spindle axis. For this variant, the maximum is 17 mm. Dimension S = 26.5 mm describes the head in the catalog view and does not replace the T value.
Designation decoder – variant selection
Five parts of the Smoxh catalog code
Designation: BDAT-R 2525 K3C (Ø24–36) T17
BDAT-R
Design
Type A · right-hand
Type A holder, right-hand version. The left-hand equivalent in the catalog has code SM63044.
2525
Shank
25 × 25 mm
The first 25 indicates the shank height h, and the second 25 is the shank width B.
K3C
Insert pocket
MGM. 3C
Korloy MGMN 300 system insert with a width of 3 mm. Select the geometry and grade for the operation.
24–36
Diameter range
Ø24–36 mm
Selection range for the first plunge diameter. It is not the groove width.
T17
Depth
T max 17 mm
Maximum axial reach specified in the catalog, measured from the workpiece face.
Smoxh designation convention · dimensions in millimeters
Tool setup and cutting data selection
Speed and feed depend on the insert, material and operating conditions
Select the carbide grade and chip breaker for the material and face grooving operation. Use the cutting speed vc and feed per revolution fn recommended for the specific insert in this operation. Check the cutting edge height, minimize overhang and ensure chip evacuation from the groove.
| Parameter | How to determine it |
|---|---|
| Speed vc [m/min] | Based on the insert grade, material and face grooving recommendations. |
| Feed fn [mm/rev] | Based on the chip breaker, insert width and clamping stability. |
| Spindle speed n [rpm] | From the grooving diameter D: n = 1000 × vc / (π × D). |
| Axial depth | According to the workpiece drawing, observing T max = 17 mm. |
Calculation example: assuming vc = 100 m/min and a grooving diameter of Ø30 mm, n = (1000 × 100) / (π × 30) ≈ 1061 rpm. The vc value is a calculation assumption, not a recommended setting for every insert.
▲ Limits: select the first plunge within the Ø24–36 mm range and limit the axial depth to 17 mm. Check the working section clearance before cutting. Widening the groove requires suitable insert geometry and a check for head interference.
Clamping the insert in 3 steps
1Clean
Remove chips from the seat and support surfaces.
2Seat
Slide in a compatible insert and check that it seats properly.
3Clamp
Close the clamp according to the holder instructions. Check that the insert is secure.
Questions about the BDAT-R tool
Applications, handedness, diameter range and insert selection
It cuts an annular groove in the face of a rotating workpiece. The cutting edge plunges parallel to the spindle axis, with the shank aligned along that axis.
No. LT indicates a type L design; the BDAT-LT 2525 K3C (36–48) T17 and (48–70) T17 variants are right-hand in the catalog. In the type A family, handedness is indicated by BDAT-R or BDAT-L.
Ø24–36 mm is the selection range for the first plunge diameter. T17 indicates a maximum axial depth of 17 mm; neither value defines the width of the finished groove.
The MGM. 3C seat is designed for the Korloy MGMN 300 system with a width of 3 mm. Check the complete insert designation, seat compatibility and geometry intended for the operation.
Product accessories


Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you


Viewed products
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.