 Polski






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot
Description
Diameter D Ø3 mm
Tolerance H73.000–3.010 mm
Shank StraightØ3 mm
Material Solid carbide (VHM)
Machine reamer Ø3 H7 solid carbide (VHM) — technical data
Solid carbide (VHM) finishing reamer, solid carbide (VHM) straight shank
| Technical Data | |
|---|---|
| Cutting diameter D | Ø3 H7 (3.000–3.010 mm) |
| Shank diameter (d9) | 3 mm |
| Flute length l | 25 mm |
| Overall length L | 50 mm |
| Number of teeth Z | 4 |
| Type | Solid carbide (VHM) finishing reamer, straight shank |
| Material | Solid carbide (VHM, cemented carbide) |
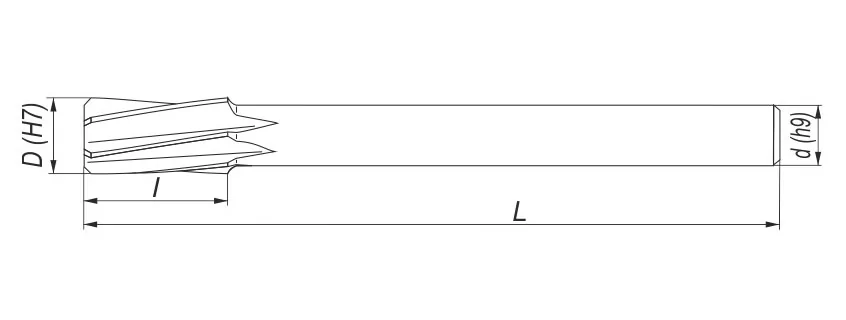
What H7 tolerance means for a diameter of 3 mm
| Class | Deviations [mm] | Dimension [mm] | |
|---|---|---|---|
| H6 | +0.006 / 0 | 3.000 – 3.006 | |
| H7 | +0.010 / 0 | 3.000 – 3.010 | SELECTED |
| H8 | +0.014 / 0 | 3.000 – 3.014 | |
| H9 | +0.025 / 0 | 3.000 – 3.025 |
The reamed hole falls within the tolerance zone 3.000–3.010 mm (ISO 286-2) — an accuracy level typical of dowel pin holes and sliding fits, among other applications.
Cutting data for the Ø3 H7 solid carbide (VHM) machine reamer
Indicative values Ø3 mm Z = 4
| Material group (ISO 513) | Vc [m/min] | fz [mm/tooth] | n [rpm] Ø3 | f [mm/min] Z=4 |
|---|---|---|---|---|
| PStructural and carbon steel | 8–10 | 0.08 | 849 | 272 |
| MStainless steel | 2–3 | 0.08 | 212 | 68 |
| KCast iron | 3–5 | 0.10 | 318 | 127 |
| NAluminum and light alloys | 12–16 | 0.12 | 1273 | 611 |
Vc — cutting speed, fz — feed per tooth (catalog values for HSS, selected for a diameter of Ø3 mm). Spindle speeds were calculated for the lower end of the range: n = (Vc × 1000) ÷ (π × D), feed rate per minute f = fz × Z × n for Z = 4. Start with the lower values and adjust according to the material and clamping rigidity. For a cemented carbide (VHM) reamer, the cutting speed can be increased relative to HSS values after trials.
You may also need: Cutting parameters calculator
Applications of the Ø3 H7 solid carbide (VHM) machine reamer for metal
Hole finishing to H7 tolerance
Machine reamer fi 3 H7 VHM — solid finishing reamer made of cemented carbide (VHM) with a straight shank, designed for precision hole finishing to tolerance H7. Carbide provides high wear resistance and dimensional stability even at higher cutting speeds and in series production. The tool face has a lead-in chamfer of ~45° for centered entry, while the guide margins on the cutting edges keep the tool aligned with the hole axis.
The Ø3 H7 carbide machine reamer removes the stock left after drilling and brings the hole to its final size within the tolerance zone H7 (3.000–3.010 mm). The tool aligns the hole axis, improves roundness and cylindricity, and reduces surface roughness to approx. Ra 0.4–1.6 µm. 4 unequally spaced cutting edges reduce vibration and machining marks. Diameters in this range are most commonly used for locating pins, guide holes in fixtures, and small precision mechanisms. Suitable for reaming steel, cast iron, and nonferrous metals — cemented carbide retains its hardness and cutting edge sharpness much longer than high-speed steel (HSS).
Workpiece materials
✓Structural and carbon steel
✓Gray cast iron
✓Aluminum and nonferrous alloys
▲Stainless steels — reduced cutting speed, generous coolant supply
✗Hardened steels above 45 HRC
Guidelines for correct reaming
- Pre-drilled hole Ø2.8 mm — stock allowance of 0.2 mm on the diameter.
- Drill the initial hole perpendicular to the surface and with minimal runout — a finishing reamer follows the existing hole and will not correct its misalignment.
- Use coolant (emulsion or cutting oil); cast iron can be machined dry.
- Withdraw the tool without reversing its rotation — reverse rotation damages the cutting edges.
Frequently asked questions — Ø3 H7 reamer
Drill a hole Ø2.8 mm — stock allowance of approx. 0.2 mm on the diameter. Too little allowance causes the material to be compressed rather than cut; too much overloads the cutting edges and reduces hole accuracy.
Cemented carbide (VHM) is harder and more rigid than high-speed steel — it maintains its size and edge sharpness much longer and also permits higher cutting speeds. It is the first-choice tool for series production; HSS remains economical for one-off jobs.
The hole falls within the tolerance zone 3.000–3.010 mm, and surface roughness is approx. Ra 0.4–1.6 µm — this accuracy is sufficient for sliding fits and dowel pin holes.
Product accessories

Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you





This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.