 Polski






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot

Description
MATERIALHSS-E
THREADM8 x1.25
HEX SHANK1/4" Hex
HOLE6.8 mm
M8 Hex combination drill tap – 1/4-inch shank for a drill driver
Technical data and operating range of the tool
| Technical data | |
|---|---|
| Thread | M8 |
| Pitch | 1.25 mm |
| Drilling diameter | 6.8 mm |
| Overall length | 50 mm |
| Max. rpm | 600 rpm |
| Shank | hexagonal 1/4" (DIN 3126) |
| Material | HSS-E (HSS-Co5) |
| Thread tolerance | 6H |
| Hole type | through hole, material thickness 2.5-8 mm |
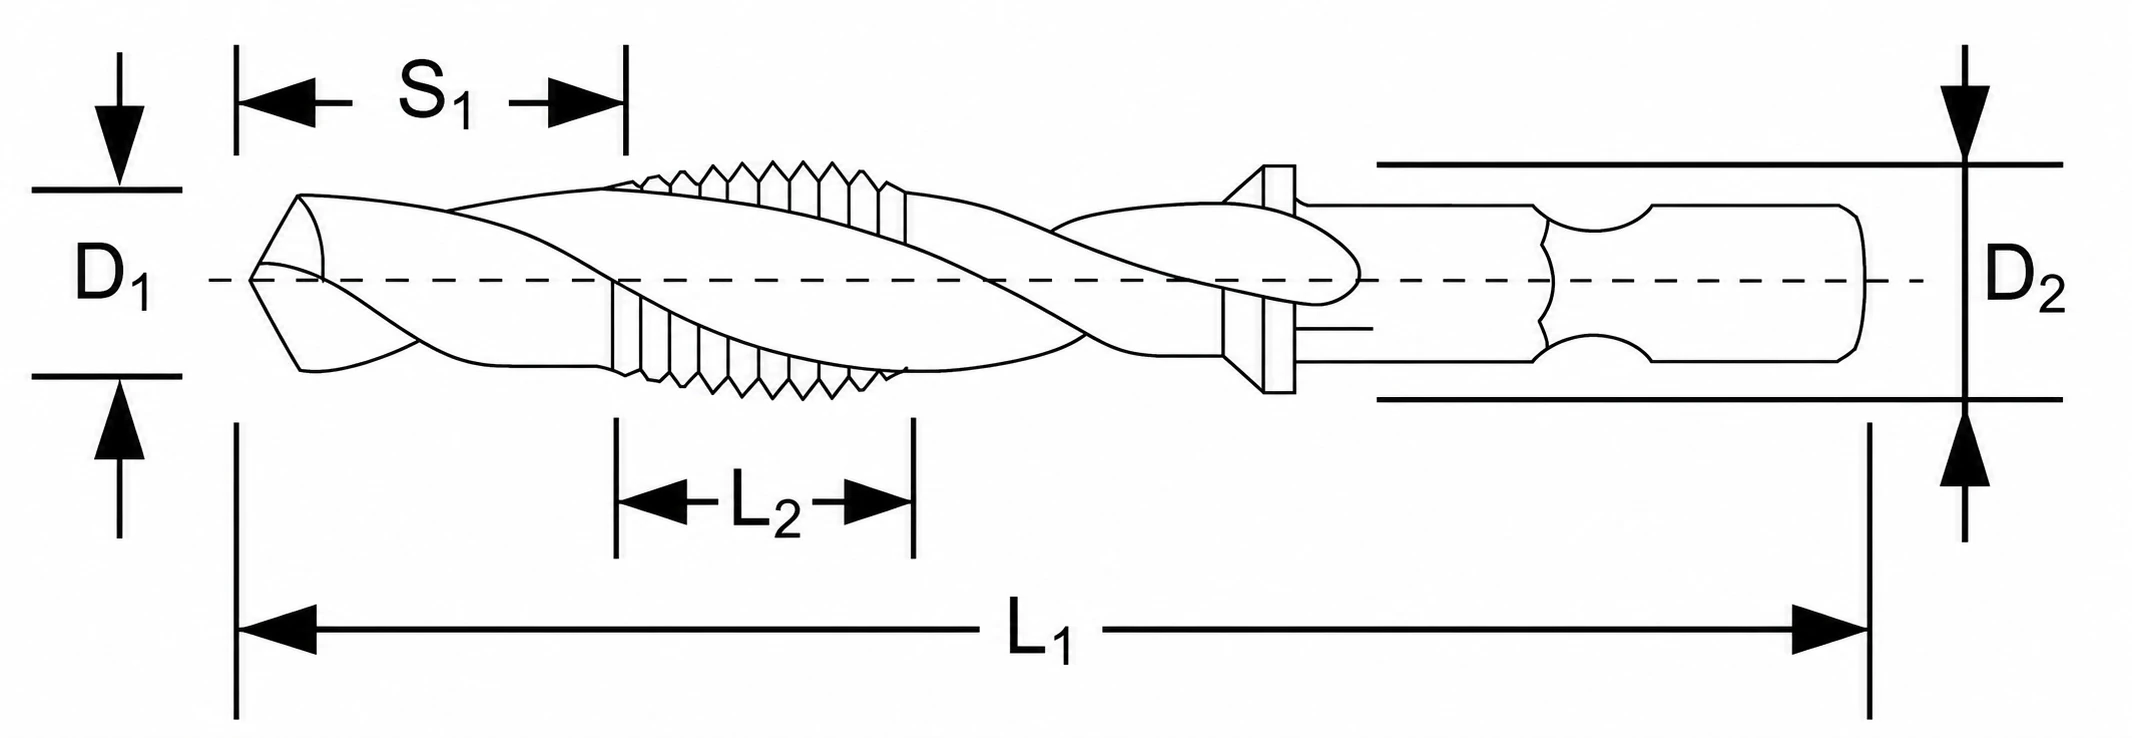
Drilling, tapping and deburring in a single pass
Tool design, hex shank and operating range
M8 Hex combination drill tap combines a 6.8 mm drill, an M8 tap and a deburring chamfer in a single body made of HSS-E high-speed steel. The drilling section produces the hole, the tapping section cuts an M8 x1.25 thread to tolerance 6H, and the tapered transition removes the burr from the entry edge – the burr on the exit side remains. The tip has a split point, so the tool centers itself and requires no center punching.
1/4-inch hex shank – combination drill tap for a cordless drill
The shank measures 6.35 mm and has a profile in accordance with DIN 3126, the same as screwdriver bits. The tool fits directly into a cordless drill's quick-release holder, a magnetic holder or a bit extension. The drill must have reverse rotation – after tapping, the tool is backed out in reverse. M8 is the largest thread in this series and requires the highest torque, so use a drill with a clutch and side handle. A jammed tool transfers the full force to your wrist.
- Three operations with one tool – a 6.8 mm hole, an M8 thread, and a chamfered edge without changing tools in the drill
- 1/4-inch shank in accordance with DIN 3126 – fits cordless drills, extensions, and magnetic holders
- Split point cutting tip – the tool centers itself; no center punch or center drill is needed
- Thread to tolerance 6H – an M8 screw threads in without reworking with a tap
- HSS-E steel (HSS-Co5) – the addition of cobalt increases the cutting edge's resistance to operating temperatures
- Material range: structural steels up to 600 N/mm², cast iron, aluminum, and brass
Where the M8 combination drill tap is used
M8 is a structural thread: flat bars, channels, gusset plates, machine frames, guard mountings and bracket attachments. The tool works only in through holes, in material from 2.5 to 8 mm thick. This is the best-matched size in the series – a typical 6-8 mm wall provides full joint load capacity. Above 8 mm, both sections cut simultaneously: their torques add up, and drilling and tapping chips meet in the same flute, resulting in tool breakage.
Operating parameters – rotational speed, cooling, and material selection
Cutting speeds for steel, cast iron, and nonferrous metals
Tapping is a low-speed operation. For steel, use a cutting speed of 6 m/min and convert it to rotational speed using the formula n = 1000 x vc / (3.14 x D): n = 1000 x 6 / (3.14 x 8) = approximately 240 rpm, corresponding to the drill's first gear. The manufacturer limits the M8 tool to 600 rpm, and in steel you will not use even half of this range. Lubricate with tapping paste containing EP additives.
| Workpiece material | vc [m/min] | n [rpm] | Lubrication |
|---|---|---|---|
| P Structural steel up to 600 N/mm² | 5-8 | 200-320 | EP tapping paste |
| M Austenitic stainless steel | 5 | up to 200 | EP paste, occasional use |
| K Gray cast iron | 8-12 | 320-480 | dry, air blast for chip removal |
| N Aluminum, brass | 15-20 | up to 600 | kerosene or oil, dry for brass |
M8 drilling and tapping step by step
Operating procedure and tool limitations
Operation step by step
1Positioning
Split point: without a center punch
2Drilling
Hole: 6.8 mm
3Tapping
Rotational speed: 240 rpm
✓Thread and chamfer
Tolerance: 6H
Parameters for structural steel up to 600 N/mm² with tapping paste lubrication
▲
Application limitations
The tool is intended exclusively for through holes in material 2.5-8 mm – in a blind hole, the thread ends before the bottom. Do not use hammer mode or work in steels hardened above 45 HRC. Work without gloves: a ribbon chip wraps around the shank and can pull your hand in.
Customer questions about the M8 combination drill tap
Selection, tap drill hole, and operating parameters
Frequently asked questions
No. The tool drills a 6.8 mm hole itself, exactly the size required for the M8 x1.25 thread (rule: nominal diameter minus pitch). Center punching is also unnecessary – the split point centers on the surface without wandering.
8 mm, equal to one nominal thread diameter. Thicker material engages both sections at once – their torques add up and chips jam in the flute. The tool then breaks at the reduced section between the drilling section and the thread core.
Yes, manufacturers specify it as a requirement, not a recommendation. Tapping paste with EP additives adheres to the tool at low speeds better than oil. Without lubricant, a built-up edge forms in steel and the cutting edge dulls after a few holes, while in aluminum the flutes become clogged with chips.
The M8 Hex combination drill tap made of HSS-E steel produces a 6.8 mm hole, an M8 x1.25 thread and an entry chamfer in a single operation. The 1/4-inch hex shank fits the quick-release holder of a cordless drill. At 240 rpm with EP paste, the tool maintains the thread profile throughout the operating cycle.
Product accessories


Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you




Viewed products


This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.