







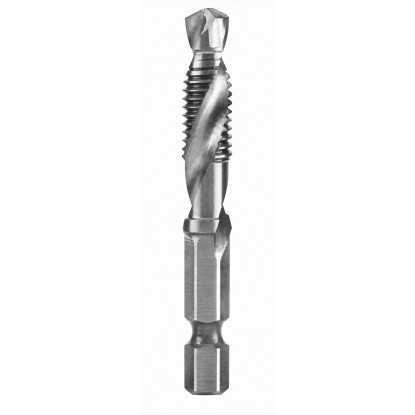

Description
Technical data and operating range of the tool
| Technical data | |
|---|---|
| Thread | M4 |
| Pitch | 0.7 mm |
| Drilling diameter | 3.3 mm |
| Overall length | 39 mm |
| Max. rpm | 1200 rpm |
| Shank | hexagonal 1/4" (DIN 3126) |
| Material | HSS-E (HSS-Co5) |
| Thread tolerance | 6H |
| Hole type | through hole, material thickness 1.4-4 mm |
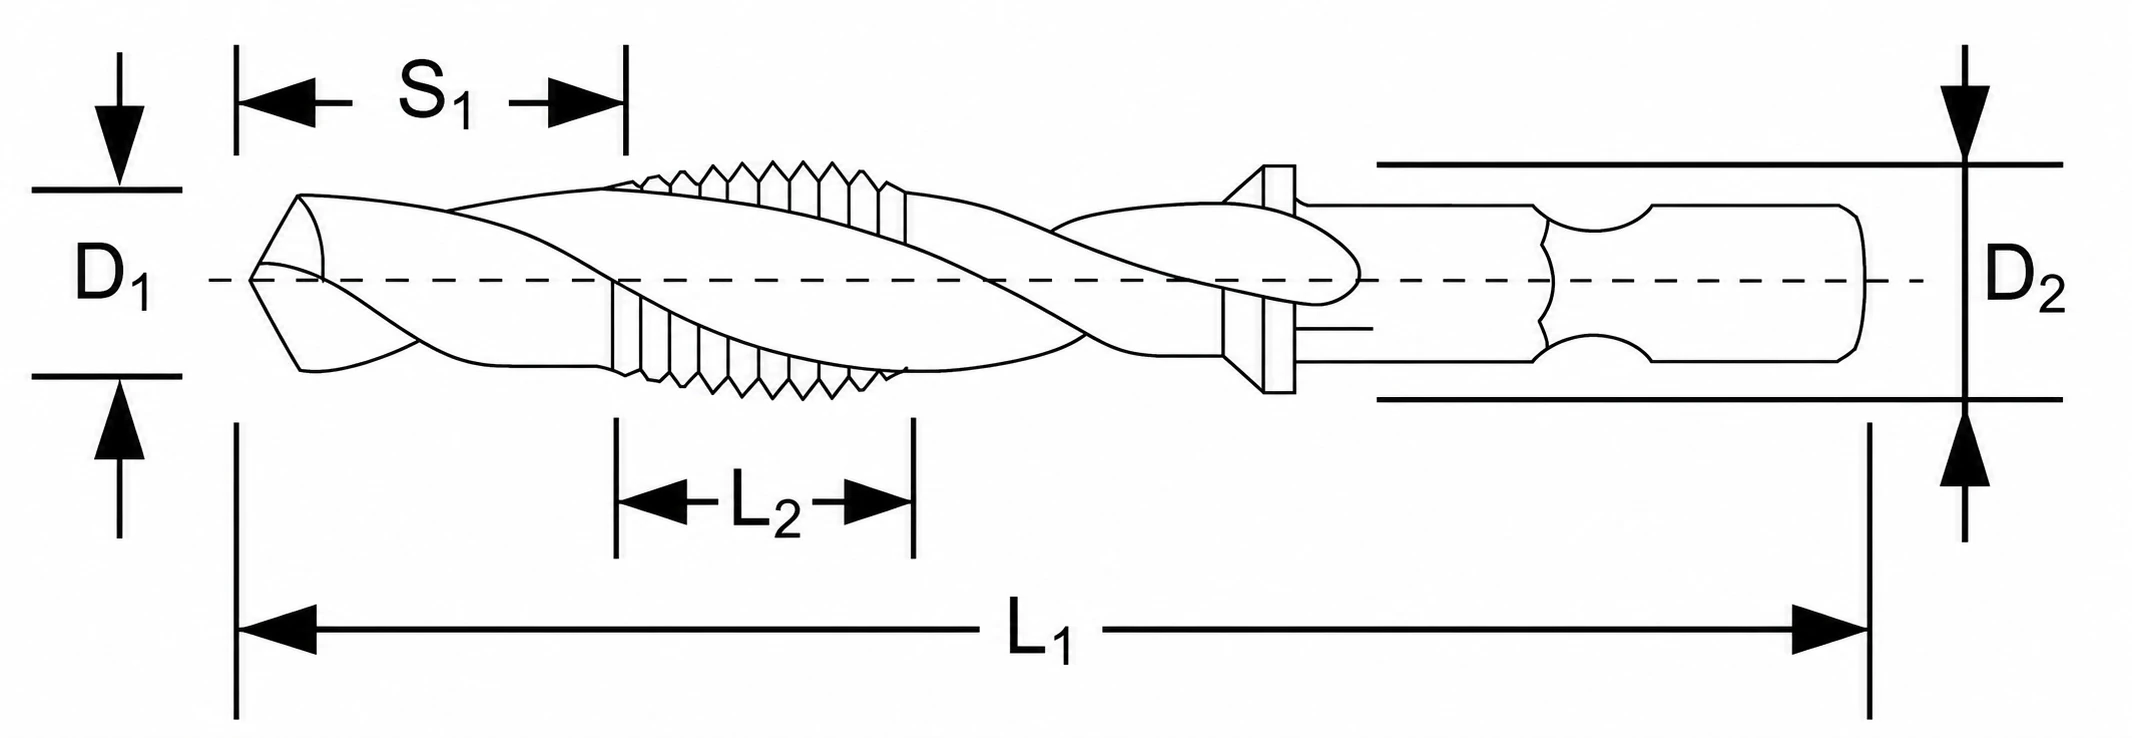
Tool design, hex shank and operating range
M4 Hex combination drill tap combines a 3.3 mm drill, an M4 tap and a deburring chamfer in a single body made of HSS-E high-speed steel. The drilling section produces the hole, the tapping section cuts an M4 x0.7 thread to tolerance 6H, and the tapered transition removes the burr from the entry edge – the burr on the exit side remains. The tip has a split point, so the tool centers itself and requires no center punching.
The shank measures 6.35 mm and has a profile in accordance with DIN 3126, the same as screwdriver bits. The tool fits directly into a cordless drill's quick-release holder, a magnetic holder or a bit extension. The drill must have reverse rotation – after tapping, the tool is backed out in reverse. The 39 mm body is short and rigid, keeping runout low during handheld operation. However, the hex shank has clearance in the socket – the tool axis must be controlled by hand throughout the pass.
M4 is a typical thread for mounting plates in electrical cabinets: brackets, terminal strips, cable glands and equipment guide rails. The tool works only in through holes, in material from 1.4 to 4 mm thick. A 4 mm wall provides full joint load capacity; at 1.4 mm, two load-bearing thread turns remain, sufficient for lightweight equipment. Remove the mounting plate before drilling – a steel chip in an electrical cabinet conducts electricity and poses a short-circuit risk.
Cutting speeds for steel, cast iron, and nonferrous metals
Tapping is a low-speed operation. For steel, use a cutting speed of 6 m/min and convert it to rotational speed using the formula n = 1000 x vc / (3.14 x D): n = 1000 x 6 / (3.14 x 4) = approximately 480 rpm. The manufacturer limits the M4 tool to 1200 rpm – this ceiling applies to nonferrous metals; work at lower speeds in steel. Lubricate with tapping paste containing EP additives.
| Workpiece material | vc [m/min] | n [rpm] | Lubrication |
|---|---|---|---|
| P Structural steel up to 600 N/mm² | 5-8 | 400-640 | EP tapping paste |
| M Austenitic stainless steel | 5 | up to 400 | EP paste, occasional use |
| K Gray cast iron | 8-12 | 640-960 | dry, air blast for chip removal |
| N Aluminum, brass | 15-20 | up to 1200 | kerosene or oil, dry for brass |
Operating procedure and tool limitations
Split point: without a center punch
Hole: 3.3 mm
Rotational speed: 480 rpm
Tolerance: 6H
Parameters for structural steel up to 600 N/mm² with tapping paste lubrication
The tool is intended exclusively for through holes in material 1.4-4 mm – in a blind hole, the thread ends before the bottom. Do not use hammer mode or work in steels hardened above 45 HRC. Work without gloves: a ribbon chip wraps around the shank and can pull your hand in.
Selection, tap drill hole, and operating parameters
No. The tool drills a 3.3 mm hole itself, exactly the size required for the M4 x0.7 thread (rule: nominal diameter minus pitch). Center punching is also unnecessary – the split point centers on the surface without wandering.
No. The drilling section is at the front and must break through the material before the tapping section starts cutting. In a blind hole, the drill reaches the bottom before usable threads are formed. Blind holes require a separate 3.3 mm drill and M4 tap.
Structural steels up to 600 N/mm², gray cast iron, aluminum and brass. Austenitic stainless steel only occasionally, at 5 m/min with EP paste – it work-hardens under the cutting edge. Hardened steels above 45 HRC are beyond the range of high-speed steel.
The M4 Hex combination drill tap made of HSS-E steel produces a 3.3 mm hole, an M4 x0.7 thread and an entry chamfer in a single operation. The 1/4-inch hex shank fits the quick-release holder of a cordless drill. At 480 rpm with EP paste, the tool maintains the thread profile throughout the operating cycle.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


