









Net price: €6.05
Description
| Technical data | |
|---|---|
| Insert shape | Round (R) |
| Diameter / edge length | 12.00 mm |
| Insert thickness s | 4.76 mm |
| Clearance angle | 15° (D) |
| Tolerance class | H (precision) |
| Design type | W — hole without a chip breaker |
| Carbide grade | PH6125 |
| Brand | Palbit (Portugal) |
grade PH6125 for ISO groups P and M — face milling and copy milling
| Workpiece material | Vc [m/min] | Feed fz [mm/tooth] | ap [mm] |
|---|---|---|---|
| PStructural steel | 150-220 | 0.10-0.22 | 0.5-3.0 |
| MStainless steel | 80-140 | 0.08-0.18 | 0.3-2.0 |
single-sided, full radius, type W without a grooved chip breaker
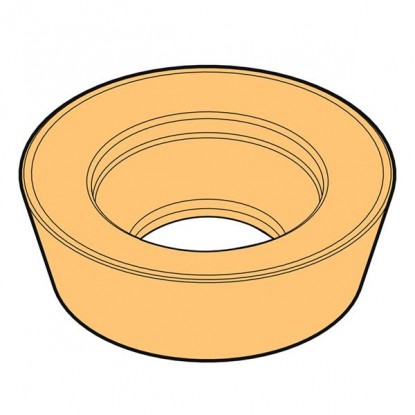
The RDHW 1204 milling insert is a round, single-sided indexable insert made of cemented carbide in grade PH6125 from the Portuguese company Palbit. The R shape, a full circle with a diameter of 12.00 mm, forms a continuous cutting edge with no corner that could chip. The fifteen° clearance angle (designation D) provides positive geometry — smoother edge entry and lower cutting forces. Tolerance class H ensures highly precise, repeatable height across all inserts in a multi-insert milling head. Design type W indicates a mounting hole without a grooved chip breaker; the characteristics of the MOT geometry should be confirmed in the product data sheet. The insert thickness is 4.76 mm, providing a robust cross section for interrupted cutting.
The RDHW 1204 round insert (also written as rdhw1204) performs well in copy and profile milling, mold machining, and productive face milling. Calculate spindle speed using n = 1000·Vc/(π·D): for a milling head with a diameter of 50 mm at a cutting speed of Vc = 180 m/min, the result is approximately 1146 rpm. The round edge has a variable entering angle — at shallow depths of cut, chips are thin and forces are low, so the insert operates reliably at increased feeds and speeds. Use climb milling on CNC machining centers to reduce friction and extend cutting edge life.
Grade PH6125 covers structural steel (ISO group P) and stainless steel (ISO group M), combining resistance to abrasive wear with resistance to mechanical impact. In stainless steels, maintain a constant feed per tooth (fz) and continuous emulsion cooling to limit work hardening of the layer being cut. Select the depth of cut ap so that it does not exceed the radius of the round edge; remove larger machining allowances in several shallower passes. With no chip breaker, increasing the feed in soft, ductile steels helps ensure reliable chip breaking.
The round insert RDHW 1204 cannot machine a vertical wall at 90° — the edge entering angle varies with depth. For straight frames and 90° pockets, use a rectangular insert APKT in a shoulder milling head. Do not set the depth of cut ap above the edge radius (approx. 6 mm).
how to read the RDHW 1204 code — positions 1–6 of the designation
Designation RDHW 1204 according to the standard ISO 1832: 4 letters describe geometry and construction, 2 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
ISO 1832 designation decoder — how to read the code
Positions 1–3 · ISO code
1RShape
Round
peripheral edge without corners
2DClearance angle
α = 15°
positive, single-sided
3HTolerance
Class H (high precision)
ground insert — highest dimensional accuracy
Positions 4–6
4WType
Countersunk hole, no chip breaker
40–60° countersink, smooth rake face
512Diameter
d = 12 mm
round insert — full radius
604Thickness
s = 4.76 mm
between rake faces
✓ Peripheral edge — full circle, no corners
round-insert milling heads and indexable milling cutters — face milling, copy milling, mold machining
Applications of the RDHW 1204 MOT PH6125 round insert:
| ✔ | Copy and profile milling (copy / contour milling) on CNC machining centers |
| ✔ | Plunge milling and machining of molds and 3D surfaces |
| ✔ | Productive face milling and heavy stock removal (heavy roughing) |
| ✔ | Structural steel (ISO P) and stainless steel (ISO M) — grade PH6125 |
| ✔ | Interrupted cutting — carbide resistant to mechanical and thermal shock |
| ✗ | Cannot machine a vertical 90° wall — variable edge angle; use an APKT insert |
| ✗ | Deep pockets in a single pass — ap limited to the edge radius |
edges, materials, design type, and depth of cut
The round R shape forms one continuous edge around the entire circumference, without corners. The insert is single-sided (clearance angle 15°), so it cuts only with its top face. Once one section wears out, rotate the insert in its pocket to a fresh section of the circumference, making use of the entire circle with a diameter of 12.00 mm.
Grade PH6125 covers structural steel (group ISO P) and stainless steel (group ISO M). For steel, maintain a cutting speed of 150–220 m/min, for stainless steel 80–140 m/min with constant feed and continuous cooling. The carbide combines resistance to abrasive wear with impact resistance.
The letter W in the fourth position indicates a mounting hole without a grooved chip breaker for chips — the rake face is smooth. Type T has an additional single-sided chip breaker. MOT is a manufacturer suffix; the characteristics of this geometry should be confirmed in the product data sheet.
Do not exceed the edge radius, which is approximately 6 mm. At low ap, the entering angle of the round edge is small, chips are thin, and forces are low — allowing increased feeds and speeds. Remove larger machining allowances in several shallower passes instead of one deep pass.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


