






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot

Description
THREAD1 1/4"-12 UNF
TOLERANCE2B
STANDARDASME B1.1
MATERIALTool steel
UNF 1.1/4-12 thread plug gauge — port inspection
Class 2B internal thread per ASME B1.1
| TECHNICAL DATA | |
|---|---|
| Thread type | Unified inch fine thread UNF |
| Thread size | 1.1/4-12 |
| Threads per inch | 12 TPI |
| Thread pitch | 2.117 mm |
| Nominal diameter | 31.750 mm |
| Tolerance class | 2B |
| Pitch diameter D2 | 30.376 – 30.579 mm |
| Hole minor diameter D1 | 29.459 – 29.919 mm |
| Gauge type | Double-ended: GO + NO-GO |
| Material | Tool steel, hardened |
| Hardness | 58-62 HRC |
| Standard | ASME B1.1 / ASME B1.2 |
| Manufacturer | Varel |
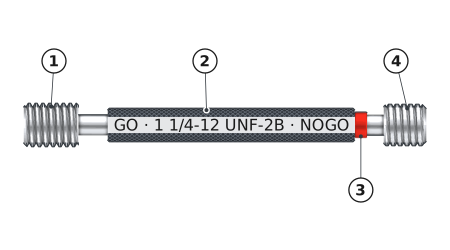
1
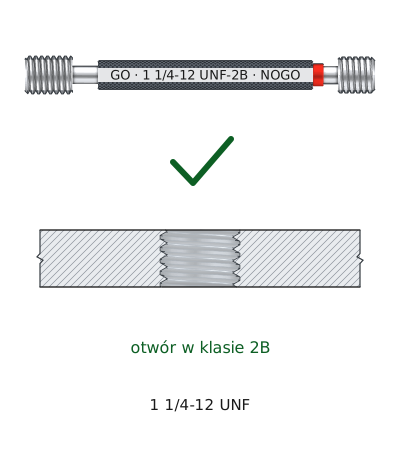
GO end — longer thread with a full profile. It is screwed in by hand through the full length of the hole.
2
Handle engraved with 1 1/4-12 UNF-2B — size and tolerance class of the hole being inspected.
3
Red ring — identifies the NO-GO end.
4
NO-GO end — shorter thread with a truncated profile. It checks only the pitch diameter, so it may engage no more than 3 turns.
UNF 1.1/4-12 thread plug gauge checks an internal thread — a port or a tapped hole in a body. The GO end must screw in by hand to the full thread depth; the NO-GO end may enter no more than three full turns per ASME B1.2.
This size is a typical end thread for a hydraulic cylinder piston rod approximately one inch in diameter, and a thread used in mounting clevises and eyes on cylinders built to the NFPA standard. The 1 1/4-12 internal thread is therefore found in an eye, a spherical joint, or a locknut — components assembled and disassembled whenever the cylinder is rebuilt.
Pre-drilled hole for 1.1/4-12 thread
Drill selection based on the D1 range
| HOLE BEFORE TAPPING | |||
|---|---|---|---|
| Size | Value | Source | Note |
| Inch drill bit | 1 11/64 = 29.766 mm | inch drill chart | difficult to obtain in Poland |
| Metric drill bit | 29.800 mm | selected to fit the D1 range | recommended |
| Class 2B minor diameter D1 | 29.459 – 29.919 mm | ASME B1.1 | the hole must fall within this range |
The entire family from one inch to one and a half inches has the same pitch 2.117 mm and differs only in diameter. A thread pitch gauge will show the same reading for each of these five sizes. Only a diameter measurement distinguishes them: 31.750 mm is 1 1/4 inches, 28.575 mm is 1 1/8, and 34.925 mm is 1 3/8.
The pitch is derived from the designation: 12 threads per inch means 25.4 divided by 12, or 2.117 mm. The basic pitch diameter is 31.750 − 0.6495 × 2.117 = 30.375 mm. This value is also the lower limit for class 2B, because an internal thread has no allowance.
Classes 1B, 2B, and 3B — size 1.1/4-12
Which class to use for each application
Comparison of internal thread classes
All three classes start at the same point — the basic pitch diameter of 30.376 mm. They differ only in the upper limit, because an internal thread has no allowance.
| Class | D2 min [mm] | D2 max [mm] | Tolerance zone | Application | Status |
|---|---|---|---|---|---|
| 1B | 30.376 | 30.681 | 0.305 mm | Field assembly, threads exposed to contamination | |
| 2B | 30.376 | 30.579 | 0.203 mm | Commercial standard — nuts and tapped holes | THIS PRODUCT |
| 3B | 30.376 | 30.528 | 0.152 mm | Joints requiring repeatability |
A class 2B hole mates with class 1A, 2A, and 3A bolts — mixing classes is permitted. Class 2B is the default: unless the drawing specifies otherwise, this is the intended class.
Port inspection in three steps
Internal thread acceptance criterion according to ASME B1.2
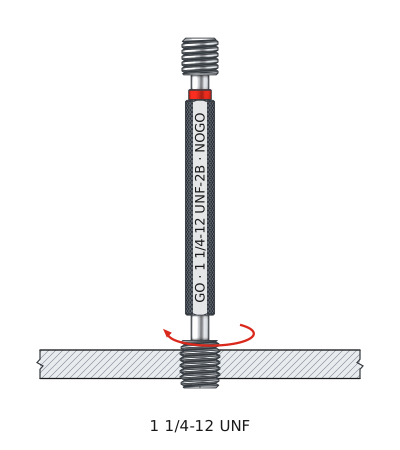
1
The GO end is screwed in by hand, without force, through the full length of the 1 1/4-12 UNF thread.
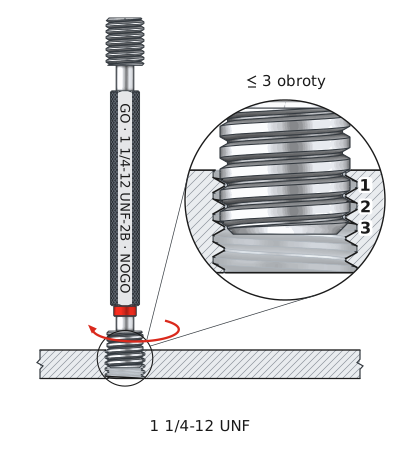
2
The NO-GO end stops within 3 full turns, without forcing.
3
The GO end passed and the NO-GO end stopped — the hole meets class 2B.
Thread inspection in 3 steps
1 GO end (passing)
Screwed in by hand — enters to the full depth
2 NO-GO end
Screwed in by hand — no more than 3 full turns
✓ Acceptable thread
Class 2B confirmed
At a pitch of 2.117 mm, the three permitted turns correspond to a depth of 6.351 mm — in a shallow port, that is already the entire thread.
GO end (passing)
Represents the maximum material condition of the port — the smallest permissible pitch diameter of 30.376 mm. In a port, it most often stops at the first thread rolled over by a cross-threaded component.
NO-GO end
Represents the minimum material condition — the largest permissible pitch diameter of 30.579 mm. Detects a port with stripped threads in which the mating component cannot be fully tightened. The body may be stamped HI.
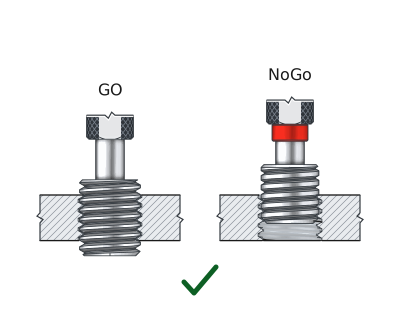
✓ Thread acceptable — GO enters the full length, NO-GO stops.
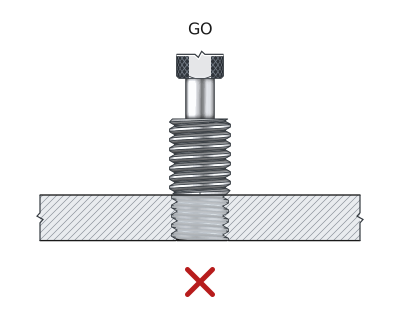
✗ Thread too tight — GO does not enter the hole.
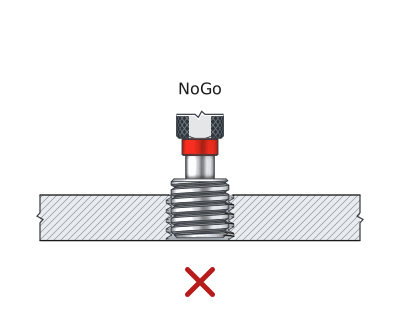
✗ Thread too loose — the NO-GO end enters more than 3 turns.
▲
The piston rod thread is subject to fatigue loading
The piston rod end transmits the full cylinder force in a push-pull cycle, so its thread wears differently from that of a bolt tightened once. Thread stripping starts at the first threads near the transition to the shank and remains invisible to the naked eye for a long time. The NO-GO end detects it earlier than any visual inspection.
Inspection scope and storage
What the gauge confirms and what it cannot measure
THE GAUGE CONFIRMS:
| ▸ | Confirms hole pitch diameter within 30.376 – 30.579 mm |
| ▸ | Checks profile and pitch together, using the GO end |
| ▸ | Detects an oversized thread, using the NO-GO end |
WHAT IT CANNOT MEASURE:
| ▸ | Hole minor diameter — this requires a separate plain plug gauge |
| ▸ | Thread depth in a blind hole |
| ▸ | Thread perpendicularity to the end face |
Frequently asked questions
Yes, it is one of the typical piston rod end and clevis threads in NFPA-standard cylinders with a piston rod approximately one inch in diameter. Eyes and spherical joints mounted on the piston rod use the same thread. However, this size is not used in hydraulic connections — ORB and JIC skip it.
Only by diameter, because the pitch is identical for all of them at 2.117 mm. A caliper measurement distinguishes them: 1 1/8 inches is 28.575 mm, 1 1/4 is 31.750 mm, and 1 3/8 is 34.925 mm. A thread pitch gauge is useless within this family.
No, only the thread. It does not assess the face, recess, or blind hole depth — yet these features determine leak tightness just as often as the thread itself. A good thread with a damaged face still means the connection needs repair.
These are two different standards: inch threads are governed by ASME B1.2, metric threads by ISO 1502. The inch criterion is more lenient on paper, but with a fine pitch, three turns still amount to only a few millimeters of depth.
Product accessories


Thread ring gauge UNF 1.1/4-12 2A GO NO-GO
Reference: 15422 In stock < 10 items
€92.11
€113.29 brutto
Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you


This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.