






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot

Description
Tap and die set from M3 to M12 — 44 pieces
Varel M3–M12 tap and die set provides a comprehensive range of equipment for professional machine shops and maintenance departments. It includes a full set of tools for cutting internal and external threads, along with tap drills and five die stocks of different sizes. It ensures dimensional repeatability and maintains tolerances in accordance with ISO standards.
The set includes
| ▸ | M3–M12 hand taps — 3-piece HSS sets with 6H tolerance (roughing + intermediate + finishing) |
| ▸ | M3–M12 round dies — HSS steel, DIN 223 / ISO 22568 standard, various diameters |
| ▸ | Tap wrenches — 2 pcs: No. 1 (range M1–M10) + No. 2 (range M4–M12) |
| ▸ | Die stocks — 5 pcs: 20×5, 20×7, 25×9, 30×11, 38×14 mm |
| ▸ | NWKa metal drill bits — 6 pcs, DIN 338, for M3–M10 threads |
| ▸ | Thread pitch gauge — 12-leaf, for metric and inch threads |
| ▸ | Screwdriver — for adjusting die stocks |
Total in the set
44 pieces
DIN 352 HSS hand taps
M3-M12 hand taps from this set are used for manually cutting internal threads. Each size includes three tools — roughing (No. 1), intermediate (No. 2), and finishing (No. 3) — so the thread is cut in stages without excessive stress on the material.
The cutting edges are made of high-speed steel (HSS) with a hardness of 64 HRC, allowing machining of structural steels with a tensile strength up to 800 MPa. DIN 352 and a 6H tolerance ensure dimensional accuracy and proper screw fit. Using three taps distributes the cutting forces over three stages — protecting the tool from breakage and producing a smooth thread profile. The square shank fits the No. 1.1/2 tap wrench included in the set, and the straight flutes facilitate chip removal during manual operation.

| Thread | Pitch P [mm] | Overall length l₁ [mm] | Flute length l₂ [mm] | Shank ∅ d₂ [mm] | Square a [mm] | Hole ∅ [mm] |
|---|---|---|---|---|---|---|
| M3 | 0.50 | 40.0 | 11.0 | 3.5 | 2.70 | 2.5 |
| M4 | 0.70 | 45.0 | 13.0 | 4.5 | 3.40 | 3.3 |
| M5 | 0.80 | 52.0 | 16.0 | 6.0 | 4.90 | 4.2 |
| M6 | 1.00 | 56.0 | 18.0 | 6.0 | 4.90 | 5.0 |
| M8 | 1.25 | 63.0 | 20.0 | 6.0 | 4.90 | 6.8 |
| M10 | 1.50 | 70.0 | 22.0 | 7.0 | 5.50 | 8.5 |
| M12 | 1.75 | 80.0 | 24.0 | 9.0 | 7.00 | 10.2 |
| 3-piece set: roughing (No. 1) + intermediate (No. 2) + finishing (No. 3) | 7 sets | |||||
Thread tolerance: 6H (ISO) | Material: HSS (high-speed steel) | Standard: DIN 352
DIN 223 HSS round dies
M3-M12 round dies extend the capabilities of the set to cutting external threads on rods and studs. They are made of high-speed steel (HSS), with dimensions and tolerances conforming to DIN 223 / ISO 22568.
The dies in this set have different diameters — from 20 mm for M3 to 38 mm for M12 — so 5 die stocks are included to cover the full range. HSS steel provides abrasion resistance when machining steel, aluminum, brass, and cast iron. The flutes evacuate chips and allow lubricant to reach the cutting zone, while the tapered chamfer makes it easier to start threading without tearing the material.
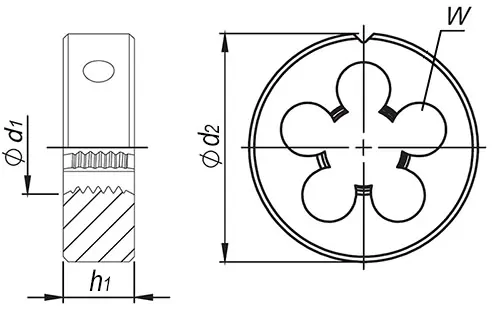
| Thread | Pitch P [mm] | Die ∅ d₂ [mm] | Thickness h₁ [mm] | Holder [mm] | Shaft ∅ [mm] |
|---|---|---|---|---|---|
| M3 | 0.50 | 20 | 5 | 20×5 | 2.9 |
| M4 | 0.70 | 20 | 7 | 20×7 | 3.9 |
| M5 | 0.80 | 20 | 7 | 20×7 | 4.9 |
| M6 | 1.00 | 25 | 9 | 25×9 | 5.9 |
| M8 | 1.25 | 25 | 9 | 25×9 | 7.9 |
| M10 | 1.50 | 30 | 11 | 30×11 | 9.9 |
| M12 | 1.75 | 38 | 14 | 38×14 | 11.9 |
| Dies + die stocks in the set: | 7 + 5 pcs | ||||
Material: HSS (high-speed steel) | Standard: DIN 223 / ISO 22568
NWKa DIN 338 metal drill bits
NWKa twist drills included in the set are selected to match the hole diameters required before tapping. Made of high-speed steel (HSS) in accordance with DIN 338, they have a standard 118° point angle and a straight shank. The set includes 6 drills with diameters corresponding to M3–M10 threads. The drill for an M12 thread (∅10.2 mm) must be purchased separately.

| Drill ∅ [mm] | Overall length L [mm] | Flute length l [mm] | For thread |
|---|---|---|---|
| 2.5 | 57 | 30 | M3 |
| 3.3 | 65 | 36 | M4 |
| 4.2 | 75 | 43 | M5 |
| 5.0 | 86 | 52 | M6 |
| 6.8 | 109 | 69 | M8 |
| 8.5 | 117 | 75 | M10 |
| Drill bits in the set: | 6 pcs | ||
Material: HSS (high-speed steel) | Standard: DIN 338 | Point angle: 118°
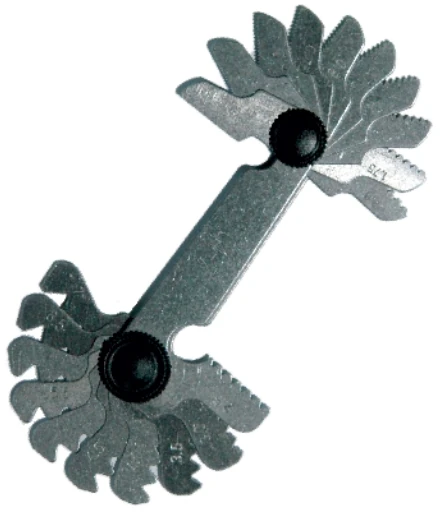
12-leaf thread pitch gauge
Thread pitch gauge enables quick identification of metric thread pitch (in mm) and Whitworth 55° inch thread pitch (in TPI — threads per inch). Essential for selecting the correct tap or die to match an existing thread.
| Metric thread pitches | |
|---|---|
| 0.50 mm | 0.90 mm |
| 0.60 mm | 1.00 mm |
| 0.70 mm | 1.25 mm |
| 0.75 mm | 1.50 mm |
| 0.80 mm | 1.75 mm |
| 55° inch threads (Whitworth) | |
| 28 TPI | 27 TPI |
| 12 leaves | |
Frequently asked questions
Drill a hole using the drill size specified in the chart — for example, 6.8 mm for M8. Drill perpendicular to the surface. Insert the taper tap (No. 1) into the tap wrench and align it vertically in the hole. Turn half a turn forward, then a quarter turn back — this breaks chips and prevents jamming. Next, use the plug tap (No. 2), followed by the bottoming tap (No. 3). Apply tapping oil throughout the operation.
Select a rod smaller than the nominal diameter — for example, 7.9 mm for M8. Chamfering the end of the rod at 45° over 1-2 mm makes starting easier. Insert the die into the die stock with the marked side facing the material. Turn steadily with both hands — half a turn forward, then a quarter turn back. Apply tapping oil generously.
Place each gauge leaf against the surface of the external or internal thread. The correct leaf fits perfectly into the grooves without any gaps. Read the pitch value stamped on the leaf — millimeters for metric threads, TPI for inch threads. The included 12-leaf gauge covers pitches of 0.5-1.75 mm.
External thread (screw, rod): Place the caliper jaws around the widest point of the thread and record the measurement, for example, 8 mm. Then try the gauge leaves against the grooves — when you find a perfect match, read the pitch, for example, 1.25 mm. Result: M8×1.25.
Internal thread (hole, nut): Open the inside jaws of a caliper against the hole walls and record the measurement. Add 1-1.5 mm to obtain the nominal diameter. Check the pitch by inserting a gauge leaf into the hole. Example: a 6.8 mm hole + a 1.25 mm pitch indicates an M8×1.25 thread.
Drill selection depends on the thread size. For metric coarse threads, use: M3 — 2.5 mm, M4 — 3.3 mm, M5 — 4.2 mm, M6 — 5.0 mm, M8 — 6.8 mm, M10 — 8.5 mm, M12 — 10.2 mm. A hole that is too small risks tap breakage; one that is too large produces a shallow thread with low load capacity. Always check the chart before drilling.
Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you



This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.