 Polski






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot

Description
THREAD1"-8 UNC
TOLERANCE2B
STANDARDASME B1.1
MATERIALTool steel
UNC 1-8 thread plug gauge — hole inspection
From tap drill to gauge
| TECHNICAL DATA | |
|---|---|
| Thread type | Unified inch thread UNC |
| Thread size | 1-8 |
| Threads per inch | 8 TPI |
| Thread pitch | 3.175 mm |
| Nominal diameter | 25.400 mm |
| Tolerance class | 2B |
| Pitch diameter D2 | 23.338 – 23.561 mm |
| Hole minor diameter D1 | 21.963 – 22.598 mm |
| Gauge type | Double-ended: GO + NO-GO |
| Material | Tool steel, hardened |
| Hardness | 58-62 HRC |
| Standard | ASME B1.1 / ASME B1.2 |
| Manufacturer | Varel |
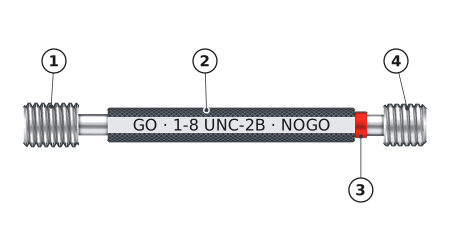
1
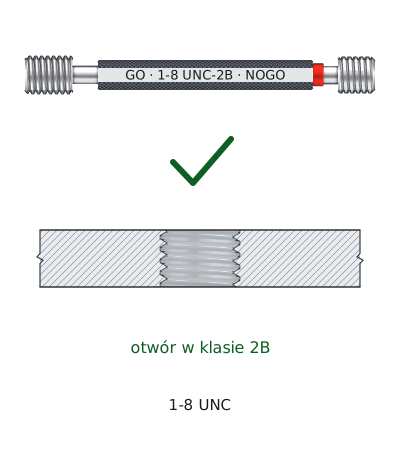
GO end — longer thread with a full profile. It is screwed in by hand through the full length of the hole.
2
Handle engraved with 1-8 UNC-2B — size and tolerance class of the hole being inspected.
3
Red ring — identifies the NO-GO end.
4
NO-GO end — shorter thread with a truncated profile. It checks only the pitch diameter, so it may engage no more than 3 turns.
UNC 1-8 thread plug gauge checks the internal thread after tapping. The GO end must screw in by hand to the full depth, and the NO-GO end no more than three full turns — as specified by ASME B1.2 for inch threads, unlike metric ISO 1502, which limits engagement to two turns.
One inch with a coarse pitch is a size covered by ASTM F3125, which specifies heavy hex structural bolts for butt connections in steel structures. The 1-8 internal thread is therefore found in structural nuts, anchor sleeves, and tapped holes in load-bearing components — wherever the load capacity of a joint depends on a single connection.
Hole before tapping — size 1-8
Standard-based criterion instead of percentage of thread height
| HOLE BEFORE TAPPING | |||
|---|---|---|---|
| Size | Value | Source | Note |
| Inch drill bit | 7/8 = 22.225 mm | inch drill chart | difficult to obtain in Poland |
| Metric drill bit | 22.250 mm | selected to fit the D1 range | recommended |
| Class 2B minor diameter D1 | 21.963 – 22.598 mm | ASME B1.1 | the hole must fall within this range |
One inch is 25.400 mm, so the thread lies between metric M24, with a diameter of 24.000 mm, and M27, with a diameter of 27.000 mm — it fits neither. Its pitch of 3.175 mm is close to the metric pitch of 3.000 mm in both sizes, so a thread pitch gauge is inconclusive. Diameter measurement is decisive.
The pitch is derived from the designation: 8 threads per inch means 25.4 divided by 8, or 3.175 mm. The basic pitch diameter is 25.400 − 0.6495 × 3.175 = 23.338 mm. This value is also the lower limit for class 2B, because an internal thread has no allowance.
Thread inspection after tapping
Three steps and the acceptance criterion per ASME B1.2
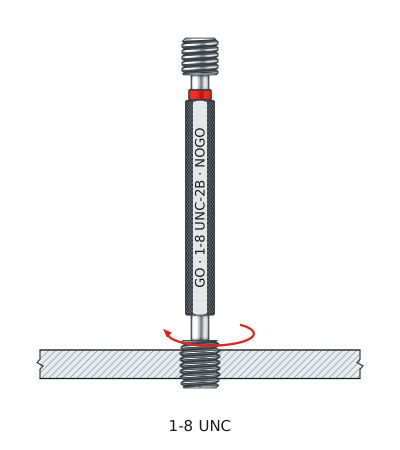
1
The GO end is screwed in by hand, without force, along the full length of the 1-8 UNC thread.
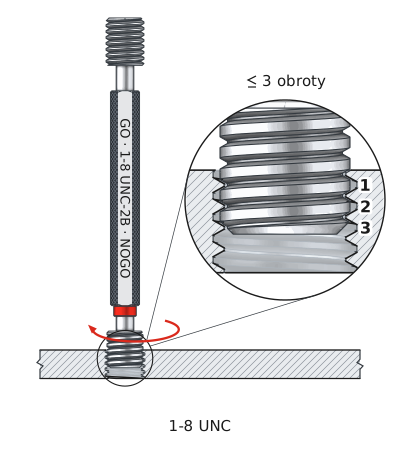
2
The NO-GO end stops within 3 full turns, without forcing.
3
The GO end passed and the NO-GO end stopped — the hole meets class 2B.
Thread inspection in 3 steps
1 GO end (passing)
Screwed in by hand — enters to the full depth
2 NO-GO end
Screwed in by hand — no more than 3 full turns
✓ Acceptable thread
Class 2B confirmed
At a pitch of 3.175 mm, three turns of the NO-GO end equal a depth of 9.525 mm. For a thin nut, the limit is reduced by agreement between the parties.
GO end (passing)
Enters only a hole correctly produced along its entire length — it corresponds to the minimum permissible pitch diameter of 23.338 mm. Resistance during insertion indicates a thread that is too tight or not tapped to full depth.
NO-GO end
Stops in a correctly produced hole — it corresponds to the maximum permissible pitch diameter of 23.561 mm. If it enters more than three turns, the thread is too loose. The body may be stamped HI.
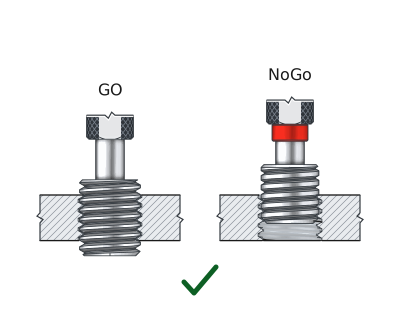
✓ Thread acceptable — GO enters the full length, NO-GO stops.
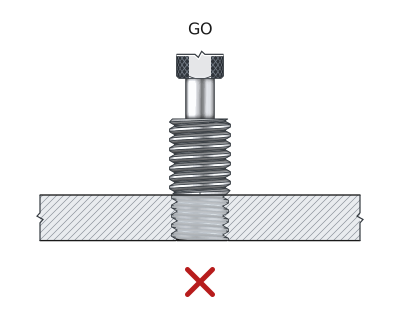
✗ Thread too tight — GO does not enter the hole.
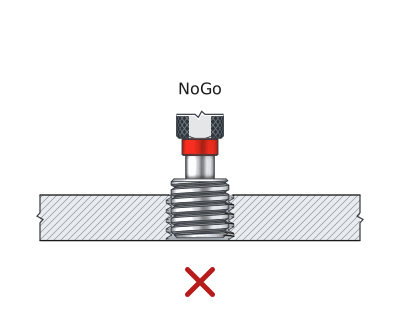
✗ Thread too loose — the NO-GO end enters more than 3 turns.
Three internal thread classes — 1-8
How 1B, 2B, and 3B differ
Comparison of internal thread classes
All three classes start at the same point — the basic pitch diameter of 23.338 mm. They differ only in the upper limit, because an internal thread has no allowance.
| Class | D2 min [mm] | D2 max [mm] | Tolerance zone | Application | Status |
|---|---|---|---|---|---|
| 1B | 23.338 | 23.673 | 0.335 mm | Field assembly, threads exposed to contamination | |
| 2B | 23.338 | 23.561 | 0.224 mm | Commercial standard — nuts and tapped holes | THIS PRODUCT |
| 3B | 23.338 | 23.505 | 0.168 mm | Joints requiring repeatability |
A class 2B hole mates with class 1A, 2A, and 3A bolts — mixing classes is permitted. Class 2B is the default: unless the drawing specifies otherwise, this is the intended class.
▲
Hot-dip galvanizing changes the thread
One-inch structural nuts are usually hot-dip galvanized, and the coating can be several dozen micrometers thick. After coating, the internal thread becomes tighter, not looser, so the GO end may not enter even if the thread was produced correctly. Galvanized nuts are inspected with an oversize gauge or tapped after coating.
Inspection scope and storage
What the gauge confirms and what it cannot measure
THE GAUGE CONFIRMS:
| ▸ | Confirms hole pitch diameter within 23.338 – 23.561 mm |
| ▸ | Checks profile and pitch together, using the GO end |
| ▸ | Detects an oversized thread, using the NO-GO end |
WHAT IT CANNOT MEASURE:
| ▸ | Hole minor diameter — this requires a separate plain plug gauge |
| ▸ | Thread depth in a blind hole |
| ▸ | Thread perpendicularity to the end face |
Frequently asked questions
No. One inch is 25.400 mm, so the thread lies between them and fits neither. The pitch is 3.175 mm versus 3.000 mm in both metric sizes — the difference is small enough that a thread pitch gauge is inconclusive. The diameter is measured with a caliper.
A 22.250 mm drill bit. The hole, including oversize caused by drilling, must fall between 21.963 and 22.598 mm — the allowable range here is 0.635 mm, the widest in the entire shipment, making drill selection straightforward. American tables specify a fractional 7/8-inch drill bit with a diameter of 22.225 mm, which is practically identical.
No, ASME B1.1 eliminated this criterion. A different requirement applies: the drilled hole, including any oversize caused by drilling, must fall between the lower and upper minor diameter limits for the class. Percentage of thread height depends on the reference used and means different things in different sources.
ASME B1.2, section 4.2.1, specifies this for inch threads. Metric ISO 1502 permits two turns — it is a different standard covering a different thread. In practice, gauge manufacturers recommend no more than one and a half turns for thin walls and ductile materials.
Product accessories


Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you


This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.