






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot
Description
Diameter D Ø55.2 mm
Tolerance h855.154–55.200 mm
Mounting Hole Ø27 mmtaper 1:30
Material HSS
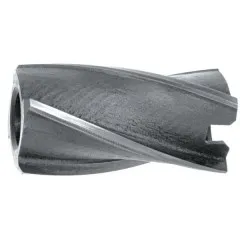
Shell roughing reamer Ø55.2 for metal — technical data
NRNa — shell roughing reamer, HSS DIN 222
| Technical Data | |
|---|---|
| Cutting diameter D (h8) | Ø55.2 mm (55.154–55.200 mm) |
| Mounting bore diameter d (taper 1:30) | 27 mm |
| Overall length L | 71 mm |
| Number of teeth Z | 4 |
| Type | NRNa — shell roughing reamer |
| Dimensional standard | DIN 222 |
| Material | HSS (high-speed steel) |
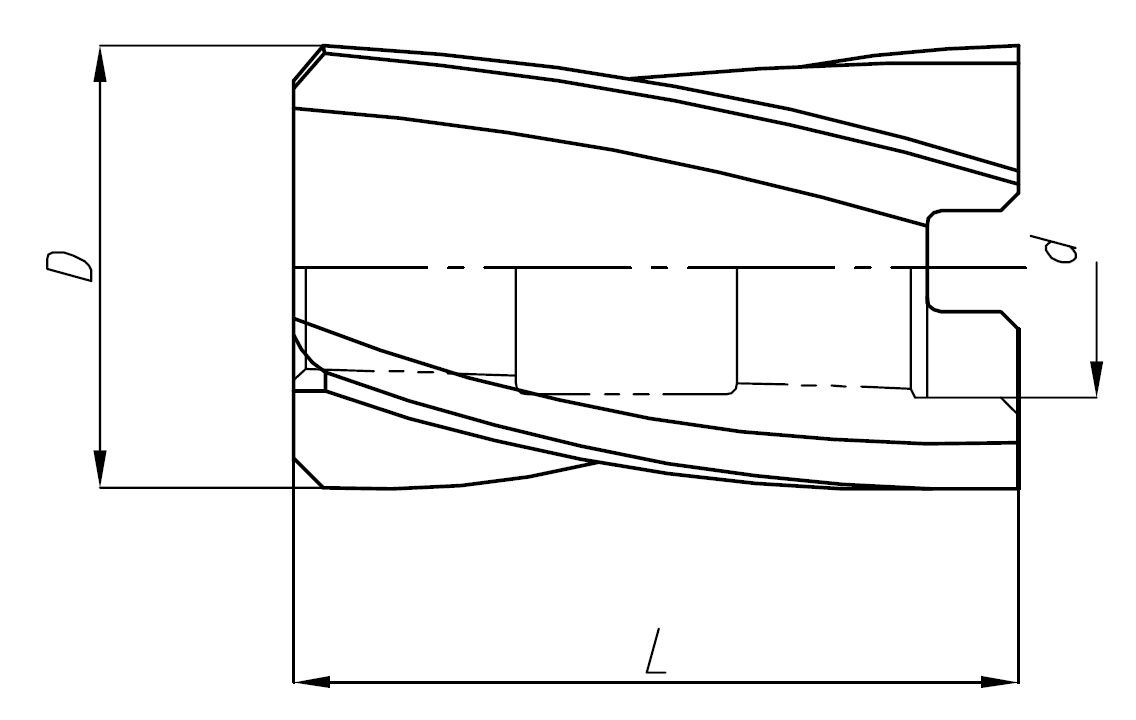
Manufacturing tolerance h8 for a diameter of 55.2 mm
| Class | Deviations [mm] | Dimension [mm] | |
|---|---|---|---|
| h8 | 0 / −0.046 | 55.154 – 55.200 | VERSION |
Cutting diameter 55.2 mm prepares the hole for a finishing reamer Ø55.5 H7 — the roughing reamer leaves an allowance of approx. 0.3 mm on the diameter for finish reaming.
Cutting data for the Ø55.2 shell roughing reamer
Indicative values Ø55.2 mm Z = 4
| Material group (ISO 513) | Vc [m/min] | fz [mm/tooth] | n [rpm] Ø55.2 | f [mm/min] Z=4 |
|---|---|---|---|---|
| PStructural and carbon steel | 8–10 | 0.28–0.40 | 46 | 52 |
| MStainless steel | 2–3 | 0.28–0.40 | 12 | 13 |
| KCast iron | 3–5 | 0.28–0.40 | 17 | 19 |
| NAluminum and light alloys | 12–16 | 0.32–0.40 | 69 | 88 |
Vc — cutting speed, fz — feed per tooth (catalog values for HSS, selected for a diameter of Ø55.2 mm). Spindle speeds were calculated for the lower end of the range: n = (Vc × 1000) ÷ (π × D), feed rate per minute f = fz × Z × n for Z = 4. Start with the lower values and adjust according to the material and clamping rigidity.
You may also need: Cutting parameters calculator
Applications of the Ø55.2 shell roughing reamer (preliminary reamer) for metal
Rough machining of holes before finish reaming
Shell roughing reamer Ø55.2 for metal — NRNa shell roughing reamer according to DIN 222 made of high-speed steel (HSS) HSS, mounted on an arbor through a tapered mounting bore Ø27 mm (1:30). The shell design allows economical machining of larger-diameter holes — one arbor accommodates multiple heads. The tool has a ~45° lead-in chamfer at the tip for centered entry, while the guiding margins on the cutting edges keep the tool aligned with the hole axis.
The Ø55.2 roughing reamer for metal straightens the hole after drilling: it corrects form errors, aligns the hole axis, and leaves a uniform stock allowance for finishing. Diameter 55.2 mm corresponds to a finished hole of Ø55.5 H7 (allowance of approx. 0.3 mm on the diameter). 4 cutting edges with large flutes evacuate chips efficiently when removing larger stock allowances, while HSS withstands demanding cutting conditions. Larger diameters are used for bearing and bushing seats and holes in machine housings, where consistent dimensions along the entire length are essential.
Workpiece materials
✓Structural and carbon steel
✓Gray cast iron
✓Aluminum and nonferrous alloys
▲Stainless steels — reduced cutting speed, generous coolant supply
✗Hardened steels above 45 HRC
Guidelines for correct reaming
- After rough reaming, ream to final size with a finishing reamer Ø55.5 H7 — stock allowance of 0.3 mm on the diameter.
- Use coolant (emulsion or cutting oil); cast iron can be machined dry.
- Withdraw the tool without reversing its rotation — reverse rotation damages the cutting edges.
Frequently asked questions — roughing reamer Ø55.2
A roughing reamer removes a large allowance after drilling, straightens the axis, and improves hole shape, but does not provide H7 tolerance. The hole is brought to final size with a finishing reamer.
The 55.2 mm diameter is selected for a finished hole of Ø55.5 H7 — after rough reaming, an allowance of approx. 0.3 mm remains on the diameter for the finishing reamer.
At larger diameters, a shell head is less expensive and lighter than a shank-type tool, and one arbor accommodates multiple diameters — an economical solution for workshops and maintenance.
Product accessories


Finishing shell reamer 55 H7 NRNb DIN 219A HSS
Reference: 2656 In stock > 10 items
€60.53
€74.45 brutto

Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you





This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.