







Description
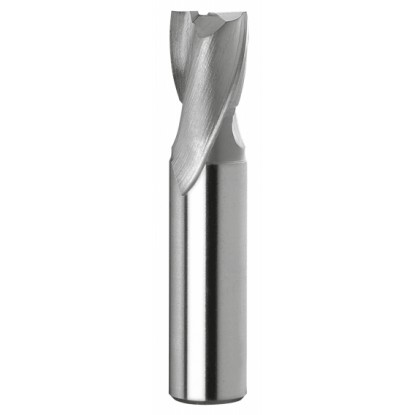
- diameter of the working part D - 15 mm,
- diameter of the shank part d - 12.0 mm,
- length of the working part l - 16.0 mm,
- length of shank part l1 - 45.0 mm,
- overall length L - 73.0 mm,
- number of blades Z - 2
| ISO symbol | Material | Cutting speed Vc [m/min] | Feed per tooth fz [mm] | Spindle speed n [rpm] | Total feed rate [mm/min] |
|---|---|---|---|---|---|
| P | Steel | 24 | 0.050 | 509 | 51 |
| M | Stainless steel | 14 | 0.045 | 297 | 27 |
| K | Cast iron | 16 | 0.060÷0.080 | 340 | 41 |
| N | Aluminum | 48 | 0.040÷0.060 | 1019 | 82 |
Calculate spindle speed using n = 1000 × Vc / (π × D). For structural steel: n = 1000 × 24 / (3.14 × 15) ≈ 509 rpm, and feed rate Vf = fz × Z × n = 0.050 × 2 × 509 ≈ 51 mm/min — use these settings on the milling machine. The total feed rate in the table is given for the lower fz value.
Two-flute end mill 15 for keyways, two-flute, type NFPg, right-hand cutting, with a cutting diameter of 15 mm. Manufactured to dimensional standard DIN 327, designed for milling keyways and narrow slots. One of the two cutting edges extends across the tool axis, allowing the end mill to plunge axially into the material without predrilling a hole. Suitable for roughing and semi-finishing. NFPg end mills have a short flute length (l = 16.0 mm) and a short straight shank with a diameter of 12.0 mm — this design provides high rigidity and limits vibration when working with a short overhang. Two-flute end mills 15 available in our store are made of high-speed steel HSS (High Speed Steel). This is a conventional tool steel with high impact toughness — the end mill withstands uneven cutting conditions and vibration typical of older milling machines, and dull cutting edges can be resharpened repeatedly. HSS without added cobalt operates at lower cutting speeds than HSSE (HSS-Co5), so the values in the table above are approximately one-fifth lower than those for cobalt end mills. The tool performs well in structural steels in classes P1.2 – P1.3, gray cast iron, and nonferrous metals. Its application limit is a workpiece hardness of approximately 275 HB (≈ 28 HRC) — above this level, the cutting edge loses hot hardness and an HSSE or carbide end mill is required. In a closed slot, chips exit through the same opening through which coolant enters, so apply plenty of emulsion along the slot; without pressurized coolant, use short passes and retract the tool between passes.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


