 Polski






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot

Description
Technical data for the M50x2 die
| Technical data | |
|---|---|
| Thread size D1 | M50x2 |
| Thread Pitch P | 2 mm |
| Outside Diameter D2 | 90 mm |
| Thickness H1 | 22 mm |
| Number of Chip Holes | 8 |
| Required Shaft Diameter | 49.82 mm |
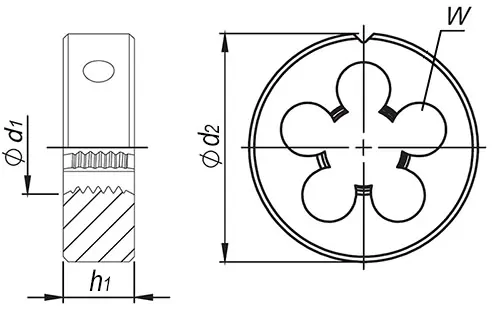
Die M50x2 WS DIN 22 568 – threading tool for medium-to-large structures
The professional M50x2 round die made of WS tool steel provides precise cutting of external metric threads with a diameter of 50 mm and a standard pitch of 2 mm. This tool combines medium-to-large dimensions with a conventional pitch, making it a versatile solution for workshops servicing industrial structures, construction machinery, and hydraulic equipment. Compliance with DIN 22 568 and a tolerance of 6g guarantee proper mating with 6H nuts in typical industrial applications. The WS designation (Werkzeugstahl - tool steel) indicates a material characterized by high hardness and wear resistance. The diameter of 50 mm places the tool in the category for medium-to-large components.
Why choose the M50x2 WS die
- Diameter of 50 mm for industrial structures – a size commonly found in industrial transmissions, hydraulic cylinders, and structural rods in medium-sized and large machinery
- Conventional pitch of 2 mm – a versatile pitch providing an optimal balance between cutting speed and mechanical strength for most structural applications
- WS tool steel – a material characterized by high hardness and wear resistance during extended operation in structural steels up to 800 MPa
- 6g/6H fit – a standard tolerance class with normal clearance that allows repeated assembly and disassembly without excessive surface wear
- Solid round design – the one-piece design provides the structural rigidity needed for threading medium-to-large diameters
The M50x2 die is a practical tool for industrial workshops, maintenance departments, and manufacturing plants serving the machinery, construction, and hydraulics industries. It is ideal for cutting threads on shafts, structural rods, hydraulic pins, and fastening components in medium-to-large machines and equipment. Use with cooling and lubricating fluids and die stocks with sufficient rigidity for a diameter of 50 mm is recommended.
Frequently asked questions
Chamfer the end of the rod (diameter 49.5-49.6 mm) at approximately 45° and clamp it very securely to eliminate vibration. Position the die perpendicular to the axis and follow this cycle: two full turns in the cutting direction, then back off half a turn to remove chips. At a diameter of 50 mm, use a die stock with handles at least 500 mm long to obtain sufficient torque.
Use threading oils or cooling and lubricating emulsions applied generously before starting and every 3-4 turns during operation. At a diameter of 50 mm, substantial cutting forces are generated – intensive lubrication is required to reduce resistance and temperature. Standard machine oil is sufficient for structural steels.
Binding at a diameter of 50 mm can be dangerous for the operator. Stop the process immediately, back the die off completely, and clean the flutes with a brass brush or compressed air. Use a micrometer to check that the rod diameter is correct. Resume with more generous lubrication and more frequent backing off – every 1.5 turn instead of every 2.
Product accessories


Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you


This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.