







Description
| Technical data | |
|---|---|
| Side length l | 12.7 mm |
| Insert thickness s | 4.76 mm |
| Hole diameter d1 | 5.16 mm |
| Corner radius rε | 1.2 mm |
| ANSI code | SNMM 433 |
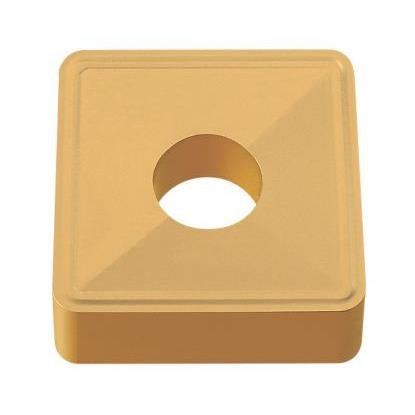
double-sided 90° square with a hole and chip breaker
The SNMM 120412 turning insert is a square indexable insert made of NT35 grade cemented carbide by the Polish manufacturer Baildonit, designed for turning steel and cast steel. Shape S, a square with a 90° corner angle, forms a substantial, strong cutting wedge that withstands demanding machining conditions. The negative geometry with a 0° clearance angle is double-sided — the square has four corners per side, providing up to eight cutting edges when the insert is indexed. The nose radius rε 1.2 mm and full thickness of 4.76 mm make this indexable insert suitable for semi-finishing and roughing at greater depths of cut. The mounting hole d1 5.16 mm ensures secure clamping of the insert in the tool holder pocket.
The SNMM 120412 insert (also written without spaces as snmm120412) is suitable for rough turning and semi-finishing shafts, bushings, and forgings made of structural steels and cast steel. Calculate spindle speed using n = 1000·Vc/(π·D): for a shaft with a diameter of 80 mm at an example cutting speed of Vc = 180 m/min, the result is approximately 716 rpm. The large nose radius of 1.2 mm and full thickness of 4.76 mm allow more stock to be removed in a single pass, making this a robust insert for turning tools operating under demanding conditions.
The square shape with a 90° corner angle increases edge rigidity and reduces chipping during interrupted cutting and when machining casting skin. The single-sided chip breaker forms and breaks thick chips, making chip evacuation easier at high feeds and depths of cut. Maintain a constant feed and a generous coolant supply during machining to reduce thermal loads on the cutting edge. The insert cross section of 12.7 mm and tolerance class M facilitate repeatable corner positioning after each indexing in the pocket. Turning inserts in this grade are supplied by the Polish manufacturer Baildonit; before selecting cutting parameters, check the intended applications of the grade against the manufacturer's current data sheet.
Source data for grade NT35 differ regarding the range of ISO groups and coating type, so confirm the cutting data in the current Baildonit manufacturer's data sheet before selecting speed and feed. For hardened steels above 45 HRC choose a cubic boron nitride (CBN) insert.
how to read the SNMM 120412 code — positions 1–7 of the designation
Designation SNMM 120412 according to the standard ISO 1832: 4 letters describe geometry and construction, 3 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
number of cutting edges, materials, and turning parameters
The square has 4 corners per side, and the negative, double-sided geometry (0° clearance angle) allows the use of up to 8 edges for cutting. Once a corner becomes dull, simply index the insert in its pocket, and once one side is worn, turn it over.
Grade NT35 is designed for turning steel and cast steel, mainly in semi-finishing and roughing operations. Confirm the exact range of ISO groups and coating type in the current Baildonit manufacturer's data sheet, as source data for this grade may differ.
The last two digits of the code (12) indicate the nose radius rε 1.2 mm — a large radius strengthens the corner and allows operation at high feeds, which is why this version is selected for roughing. Inserts from the same family with a smaller radius (e.g., 0.8 mm) are suitable for lighter, more precise cutting.
Yes — the 90° square corner, single-sided chip breaker, and full thickness 4.76 mm provide strong geometry for removing large machining allowances. Maintain a constant feed and a generous coolant supply to reduce thermal loads on the cutting edge when rough turning steel and cast steel.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


