






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot

Description
Technical data for the UNC 7/8-9 hand tap
| Technical data | ||
|---|---|---|
| Nominal Diameter d1 Inches/mm/Decimal | UNC 7/8-9 | |
| Thread Pitch P in Inches and mm | 9 threads per inch | 2.82 mm |
| Thread Diameter d1 mm / Decimal | 22.22 mm / 0.8750 in | |
| Thread angle G | 60° | |
| Thread Standard | UNC ANSI B-1.1 | |
| Overall Length l1 | 100 mm | |
| Flute Length l2 | 32 mm | |
| Shank Diameter d2 | 18 mm | |
| Square Drive Width Across Flats a | 14.5 mm | |
| Tap Drill Hole | 19.5 mm | |

Roughing, intermediate, and finishing taps – how much material each removes
Division of work in the 1–2–3 set
The UNC 7/8-9 thread is cut into the wall of a 19.5 mm diameter hole. The thread groove extends 1.36 mm into the wall. A single tap would have to cut the entire groove at once – by hand, this means high resistance and a risk of breakage. The set divides this work into three layers.
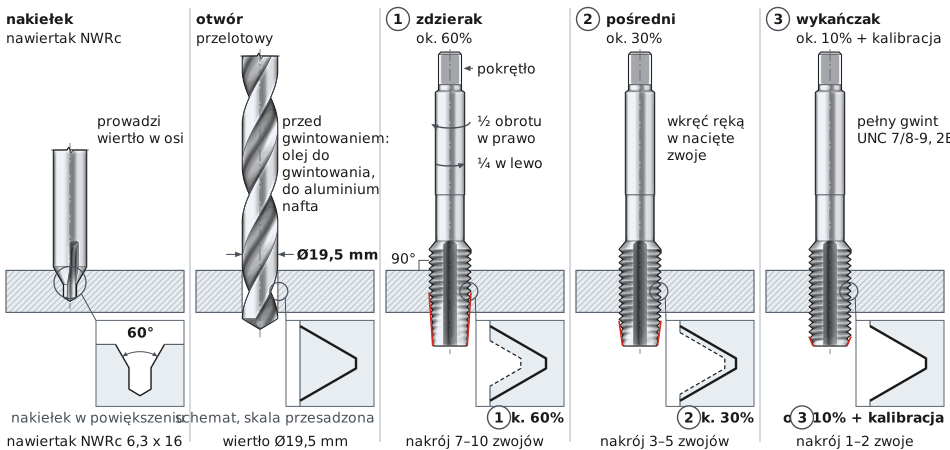
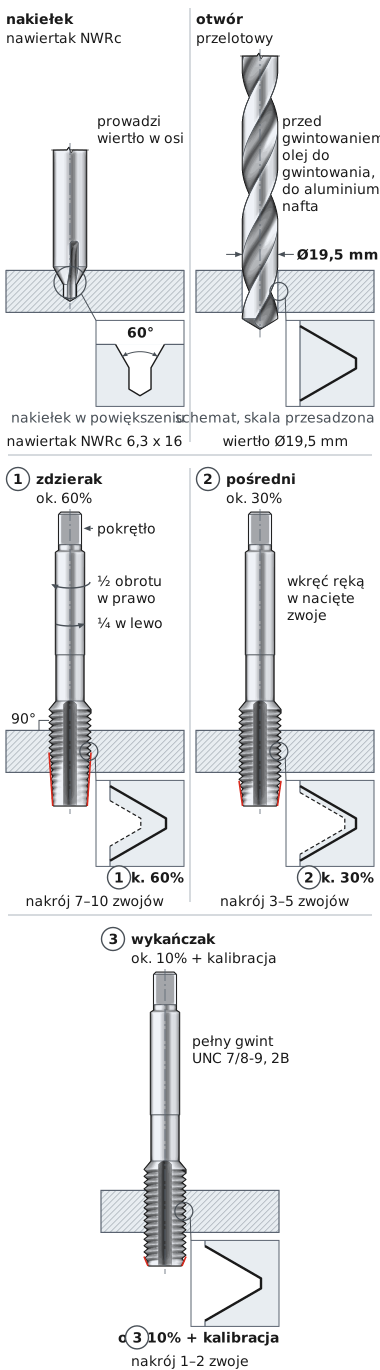
The drawing shows the entire set in operation. All three taps have the same shank and the same length. They differ in chamfer length: No. 1 has a taper spanning 7–10 threads, while No. 3 spans only 1–2 threads. The detail views at the hole wall show how the thread groove deepens after each tap.
| Tap | Chamfer | Material removed | How it works in the hole |
|---|---|---|---|
| No. 1 – roughing tap | long, 7–10 threads | approx. 60% | enters smoothly and establishes thread alignment |
| No. 2 – intermediate | medium, 3–5 threads | approx. 30% | screws into the previously cut threads and starts cutting only deeper in the hole |
| No. 3 – finishing tap | short, 1–2 threads | approx. 10% + sizing | turns easily and produces the full 2B profile |
How to identify the tap numbers in the set
The chamfer is the tapered end of the tap. No. 1 has the longest chamfer and No. 3 the shortest – the difference is immediately visible when they are placed side by side. No. 1 and No. 2 have shallower thread profiles; only No. 3 has the full profile. Keep the set together and always start with the roughing tap.
How to tap a UNC 7/8-9 hole – sequence 1, 2, 3
Hand tapping step by step
Thread UNC 7/8-9 in five steps
ØDrilling
Drill bit 19.5 mm
1Roughing tap
Removes approx. 60%
2Intermediate
Removes approx. 30%
3Finishing tap
Removes approx. 10%
✓Finished thread
Tolerance 2B
Turning sequence: half a turn clockwise, a quarter turn counterclockwise | Between taps: remove chips from the hole
Start with the hole. For inch threads, pitch is specified in threads per inch, so first convert it to millimeters: an inch equals 25.4 mm, and 25.4 : 9 threads ≈ 2.82 mm. The diameter of the UNC 7/8-9 thread is 7/8 inch, or 22.22 mm. The diameter of 22.22 mm minus the pitch of 2.82 mm gives 19.4 mm. The table specifies a 19.5 mm drill bit: tolerance 2B permits a hole from 19.18 to 19.76 mm, and this drill bit falls within that range. An undersized hole is a common cause of taps twisting off in the workpiece.
Through hole or blind hole – how deep to drill
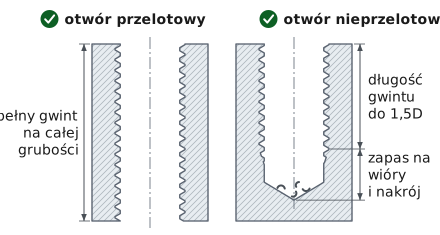
The set taps both types of holes. In a through hole, the thread extends through the full material thickness. In a blind hole, cut the thread to 33.3 mm, or 1.5 times the thread diameter (1.5 x 22.22 mm, shown as 1.5D in the drawing). Drill the hole deeper than the thread. The clearance below the thread accommodates chips and the finishing tap chamfer.
No. 1 – the roughing tap establishes thread alignment
Fit the roughing tap in the tap wrench and position it perpendicular to the surface. Check the angle from two sides, for example with a square. Turn half a turn clockwise, then a quarter turn counterclockwise. Reversing breaks the chip into short pieces – a slight crunch is normal. The first threads determine whether the thread will be straight.
No. 2 and No. 3 – deepening and full profile
Back out the roughing tap and remove the chips from the hole. Screw the intermediate tap into the cut threads by hand – it should engage them naturally. It turns easily at first and starts cutting only deeper in the hole. The finishing tap enters with almost no resistance and cuts the final portion of the profile only at the end. When it screws in smoothly all the way, the thread is complete – check it with a UNC 7/8-9 screw.
UNC 7/8-9 hand tap – set of 3 pcs for large American inch threads
UNC 7/8-9 hand tap is a three-piece set of professional tools for cutting large-diameter internal threads to the Unified National Coarse – UNC standard. The set consists of roughing, intermediate, and finishing taps made of HSS in accordance with DIN 352.
Characteristics of the UNC 7/8-9 tap
- Class 2B tolerance – general-purpose accuracy for industrial and structural joints
- Large diameter of 7/8 inch (22.23 mm) – designed for heavy-duty bolted joints carrying substantial loads
- 9 threads per inch (2.82 mm pitch) – coarse thread profile for fast assembly
- Three-stage tapping – distributing cutting across three tools prevents overload and breakage
- HSS high-speed steel – machining structural steels, cast iron, and aluminum up to 800 MPa
The UNC 7/8-9 size is used in American-made heavy construction equipment, steel structures, and mining machinery. The UNC 7/8-9 inch tap is chosen by workshops servicing Caterpillar and Komatsu machinery and other equipment imported from the USA.
Frequently asked questions
Calculate the hole size using the formula: d = D - P. For UNC 7/8-9: d = 22.23 mm - 2.82 mm = 19.41 mm. Use a 19.5 mm drill bit before tapping.
Large diameters and pitches require substantial material removal. Dividing the process into three stages (roughing, intermediate, and finishing taps) reduces the load on each tool and eliminates the risk of tap breakage.
You need a caliper and a thread pitch gauge. External thread (on a shaft): measure the outside diameter; it should be 22.23 mm (7/8 in). Internal thread (in a hole): measure the hole diameter; it should be approximately 19.5 mm. Then place the thread pitch gauge against the threads; the 9 TPI leaf fits this thread. The 60° thread angle confirms the American standard.
Product accessories


19.5 mm HSS DIN 338 fluted metal drill bit
Reference: 0000004467 In stock > 10 items
€8.42
€10.36 brutto


Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you


Viewed products
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.