







- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot

Description
Turning tool for internal threads SIR S25 22 Varel
Right-hand SNR-0025R22 boring bar for 22 IR indexable inserts
| Technical data | |
|---|---|
| Manufacturer designation | SNR-0025R22 |
| Machining operation | Internal threading |
| Design | Right-hand (R) |
| Shank diameter | Ø25 mm |
| Overall length | 200 mm |
| Distance from cutting edge to shank axis | 18.1 mm |
| Minimum bore diameter | Ø29 mm |
| Insert family | 22 IR |
| Thread types with the appropriate insert | Metric M – 60° Whitworth BSW – 55° Unified UN – 60° Trapezoidal Tr – 30° |
| Metric pitch range | 3.5–6.0 mm Depending on the selected 22 IR insert |
| Trapezoidal thread pitch range | 4–5 mm |

The illustrative photo shows one of the boring bars in this family.
The insert shown in the photo is not included with the turning tool.
SNR-0025R22 – internal thread turning in practice
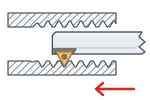
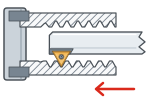
The workpiece with a bore rotates while the boring bar moves along the bore axis
Turning tool for internal threads SIR S25 22 Varel is a right-hand boring bar for threading bores in bushings, nuts, and housings. The Ø25 mm shank is clamped in a sleeve or boring bar holder. With a suitable 22 IR insert, you can cut metric M and inch UN threads with a 60° profile, as well as inch Whitworth BSW threads with a 55° profile.
The metric pitch range is 3.5–6.0 mm, depending on the selected insert. Example: an M33 x3.5 thread has a pitch of 3.5 mm, so it requires a 22 IR 3.5 ISO insert. For inch BSW and UN threads, match the insert to the profile and threads per inch (TPI). This is an indexable turning tool: when the cutting edge wears out, only the insert is replaced, while the body is retained.
The smallest bore the boring bar can enter is Ø29 mm. This allows metric threads starting at M33 x3.5 to be cut. Larger threads can be cut with the same boring bar because the thread diameter is determined by the bore in the part.
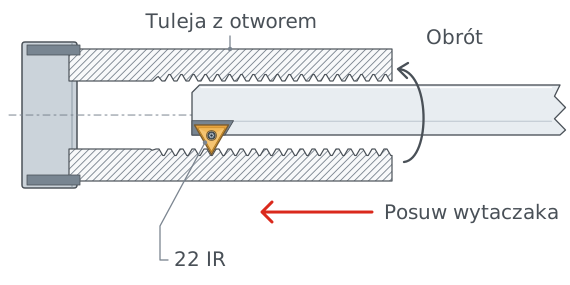
Schematic diagram. Right-hand boring bar in a sleeve bore, feeding toward the chuck.
How does an internal threading tool work?
The insert deepens the same profile with each successive pass. The feed remains synchronized with spindle rotation. For a single-start thread, boring bar travel per revolution equals the thread pitch.
In a typical setup, a right-hand boring bar cuts from the bore opening toward the lathe chuck. The R symbol itself identifies the holder design. The hand of the resulting thread also depends on the tool setup, spindle rotation and feed direction.
22 IR inserts – selecting the thread profile and pitch
One holder, different tasks with the appropriate insert
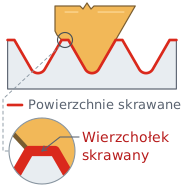
Full profile 22 IR ISO
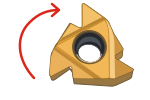
A full-profile insert, such as 22 IR 4 ISO, is designed for a specific pitch. It machines the thread flanks, root and crest. A different pitch requires the appropriate insert version.
Example: metric profile, 4 mm pitch.
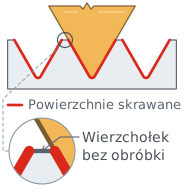
Partial profile 22 IR N60
A partial-profile insert, such as 22 IR N60, covers pitches of 3.5–5 mm (7–5 threads per inch). It does not finish the thread crests. The bore diameter must be prepared beforehand with a suitable tool.
Selection: profile, pitch range and insert grade.
Choose a full-profile insert for production runs of the same thread. The crest is formed together with the flanks, without a separate operation, ensuring a repeatable profile. An N60 insert with a 60° profile or an N55 insert with a 55° profile covers several pitches, making it useful for short runs and one-off parts. The crest then depends on the previously turned diameter, so profile control is less precise. With a 22 IR TR insert, you can cut a Tr trapezoidal thread with a pitch of 4–5 mm.

The final “22” indicates the insert size, not the diameter of the thread being cut. The thread profile and pitch depend on the selected 22 IR insert. 16 IR and 22 ER inserts are not direct substitutes for each other.
Threading with a boring bar on a lathe – setup and feed
Short overhang, correct cutting edge height and synchronized motion
Set the cutting tip at spindle center height. Check the alignment of the insert profile relative to the bore axis. A steel boring bar operates stably with an overhang of up to approximately 4 shank diameters, or approximately 100 mm. Remove chips from the pocket and support surfaces before mounting.
Select the cutting speed and number of passes according to the insert, material and clamping rigidity. The SIR body alone does not determine cutting data for steel, stainless steel or aluminum.
The SIR S25 22 Varel internal threading turning tool requires a sleeve or tool post for a Ø25 mm shank. It fits bores from Ø29 mm, so check the bore diameter before threading. The overall length of 200 mm describes the body, not the permissible working overhang. Check the final thread dimensions against the requirements on the part drawing.
Feed for a 4 mm pitch
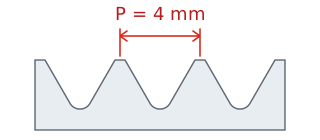
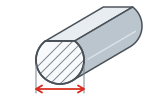
Pitch P is measured along the axis between corresponding points on adjacent thread turns.
For a single-start thread, the tool moves axially by 4 mm for each spindle revolution.
Feed per revolution:
fn = P = 4 mm/rev.
Example: spindle speed n = 150 rpm
vf = n × P = 150 × 4
600 mm/min
Feed rate
150 rpm is a calculation example, not recommended cutting data. The threading cycle requires the feed to be synchronized with the spindle.
Internal thread turning with a boring bar – approach, cutting pass and retraction
Each pass uses the same four movements, going slightly deeper each time
The internal thread is formed in several passes. In each pass, the boring bar follows the same cycle of four movements, and the 22 IR insert cuts slightly deeper into the bore wall each time until the profile reaches full depth. The diagram shows one pass of a right-hand SIR boring bar.
Single-pass cycle
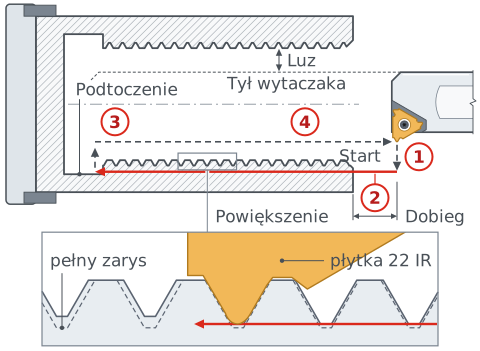
Schematic diagram, sleeve cross section. Red line – cutting movement, the insert is cutting. Dashed lines – rapid movements without cutting.
1
Approach
The boring bar moves from the starting point in front of the sleeve end face and feeds outward from the axis toward the wall to the depth of this pass. This is a rapid movement without cutting.
2
Cutting pass
The insert cuts while moving deeper into the bore toward the chuck. For each spindle revolution, the boring bar advances by the thread pitch P, for example 4 mm.
3
Retraction
At the end of the thread, in the relief groove near the bottom, the boring bar retracts from the wall toward the axis. The retraction distance is short because the back of the boring bar must not touch the opposite wall.
4
Return
The retracted boring bar rapidly exits the bore and returns to the starting point. It begins the next pass with a slightly deeper infeed.
Set the starting point in front of the sleeve end face so the insert enters the material with the feed already equal to the pitch. The total insert infeed depth for an internal thread is approximately 0.58 × P, or approximately 2.31 mm for a pitch of 4 mm. In a blind hole, machine a thread relief groove near the bottom at least 1.05 × P wide, or approximately 4.2 mm, and at least as deep as the infeed depth. Chips remain in the bore, so for small diameters, direct coolant precisely into the cutting zone.
Boring bar infeed and number of passes in thread turning
The infeed direction determines which insert edge cuts
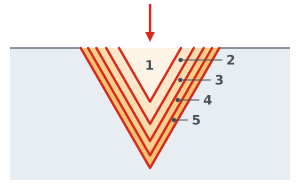
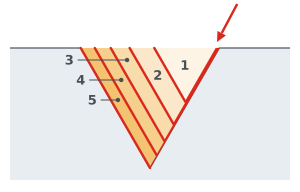
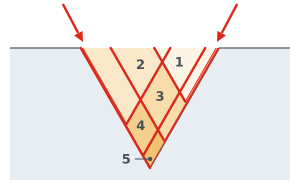
Infeed is the movement that takes the insert deeper into the bore wall on the next pass. Its direction determines which insert edge cuts and how the chip flows. In the diagrams, the bore wall is at the bottom and the boring bar approaches from the axis. Red lines show successive positions of the insert tip, and the arrow shows the infeed direction. The numbers 1–5 and progressively darker bands indicate successive passes. The bold line shows the insert edge that is cutting.
Radial infeed
The insert feeds straight into the wall, perpendicular to the axis, and cuts with both edges. This is the simplest method. It works well for fine pitches, short-chipping materials and hardened materials.
Modified flank infeed
The boring bar moves diagonally along the flank, or side of the profile, at an angle a few degrees less than 30°. One edge does most of the cutting, while the other does not rub against the thread flank. Manufacturers recommend this method as the first choice for most threads.
Alternating flank infeed
The boring bar alternately moves along each flank of the profile, so both edges wear evenly. This method helps with coarse pitches and long-chipping materials. It requires a program that is not available on every lathe.
Select the number of passes according to the pitch, material and thread type – insert manufacturers' catalogs list internal threading as a separate selection factor. For a pitch of 4 mm, they specify 10–20 or 11–18 passes; harder materials require more passes. The first pass is the deepest, and each subsequent pass is shallower. The final pass should not be shallower than approximately 0.05 mm, or the edge will start rubbing instead of cutting.
SIR S25 22 – selection and application questions
Key information before selecting a boring bar
The boring bar accepts right-hand internal threading inserts from the 22 IR family. These include full-profile inserts, such as 22 IR 4 ISO or 22 IR 6 W, and partial-profile inserts, such as 22 IR N60 and 22 IR N55. Select the profile, pitch, and grade suitable for the application.
No. The final 22 indicates the insert size. The shank diameter is 25 mm, and the boring bar length is 200 mm. The bore in the workpiece determines the thread diameter.
The boring bar enters bores starting at Ø29 mm. This range includes the bore for M33 x3.5 (thread minor diameter 29.21 mm). Larger threads can be cut with the same boring bar by selecting a suitable 22 IR insert.
Coarse threads from M33 x3.5 (pre-thread bore diameter 29.21 mm) to M64 x6. For example, M33 x3.5 requires a 22 IR 3.5 ISO insert, and M64 x6 requires an 22 IR 6 ISO insert.
Up to 6 mm with a 22 IR 6 ISO full-profile insert, for example M64 x6. The 22 IR N60 and 22 IR N55 inserts cover pitches of 3.5–5 mm, or 7–5 threads per inch.
Product accessories


Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you


Viewed products
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.