






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot
Description
DIAMETER Ø8 mm
LENGTH 100 mm
INSERT CCMT 0602rr
ANGLE κr 95°
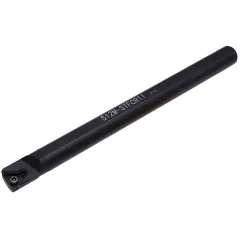
Technical specifications of the S08 SCLCR 06 boring bar
| Technical data | |
|---|---|
| ISO designation | S08 SCLCR 06 |
| Shank diameter (d) | Ø8 mm |
| Effective height (h) | 7 mm |
| Overall length (L) | 100 mm |
| Functional overhang (f) | 7 mm |
| Min. bore diameter (D_min) | Ø11 mm |
| Entering angle (κr) | 95° |
| Clearance angle | 7° (pos.) |
| Clamping system | ISO — center screw (S) |
| Insert type | CCMT 0602rr |
| Cutting direction | R — right-hand (L version available) |
| Shank material | Steel (S) |
| Manufacturer | Smoxh |
S08 SCLCR 06 boring bar – for internal turning and bore finishing
Internal turning tool for machining bores from Ø11 mm
Boring bar S08 SCLCR 06 is an indexable boring bar designed for longitudinal turning and bore finishing with diameters from 11 mm. The round steel shank with a diameter of Ø8 mm and a length of 100 mm provides cutting stability even with greater tool overhang. The geometry with an entering angle of 95° allows turning along the wall with simultaneous light facing.
In the central screw clamping system (S), the screw secures the CCMT 0602rr insert through its hole, so only one screw needs to be loosened for replacement. The positive geometry of the 80° diamond insert with 2 cutting edges is well suited to finishing, providing low cutting forces and a smooth machined surface. The boring bar is compatible with CCMT 06 inserts in various carbide grades — select the grade to match the workpiece material.
Decoding the SCLCR designation of the S08 SCLCR 06 boring bar
What the individual letters in the ISO designation mean
Decoding the designation SCLCR
S

CLAMPING
Center screw (S)
The screw secures the insert through its center hole
C
INSERT SHAPE
80° rhombus 80°
CCMT insert — positive, single-sided, 2 cutting edges
L
ENTERING ANGLE
κr = 95°
Longitudinal turning + facing
C
CLEARANCE ANGLE
α = 7° (pos.)
Positive geometry — low cutting forces, finishing and medium machining
R
DIRECTION
Right-hand (R)
Feed to the left — from the tailstock toward the spindle
Shank: ø8 mm (S08H, steel) · Insert: CCMT 0602rr
Typical applications of the S08 SCLCR 06 boring bar
Cutting operations:
| ▸ | Longitudinal boring — enlarging and finishing cylindrical bores from Ø11 mm |
| ▸ | Bore finishing — positive CCMT geometry provides low cutting forces and a smooth surface |
| ▸ | Internal taper turning — bearing seats, internal chamfers, Morse tapers |
| ▸ | Light facing — the 95° angle allows machining the face inside the bore |
| ▸ | CNC production runs — repeatable cutting edge positioning and quick insert replacement in the holder |
Included
S08 SCLCR 06 package contents
Package contents:
| ✓ | Boring bar body S08 SCLCR 06 | 1 pcs |
| ✓ | Center screw for clamping the insert | 1 pcs |
| ✓ | Hex key for insert replacement | 1 pcs |
| ✗ | CCMT 0602rr cutting insert (sold separately) | — |
Compatible CCMT 0602rr insert
CCMT 0602rr
The cutting insert is not included in the set — must be purchased separately. CCMT insert. Positive geometry means that the insert is single-sided and has 2 cutting edges, providing low cutting forces and good surface quality.
Select the insert grade to match the workpiece material: P (structural steels), M (stainless steel), K (cast iron), N (aluminum). You can find compatible inserts in the section "Related products" below.
Insert installation and replacement for the S08 SCLCR 06 boring bar
Instructions for the center screw clamping system (S)
Insert replacement procedure step by step
1 Unscrew the screw
Unscrew the center screw 2-3 turns
2 Clean the insert seat
Remove chips and debris
3 Install the insert
Position in the seat
4 Tighten the screw
Torque 0.6–1.2 Nm
Important: Do not exceed the recommended tightening torque — this may damage the thread in the seat or crack the insert.
Checks before starting work:
| ▸ | Tool overhang — do not exceed 4×d (32 mm) without support; use vibration damping for greater overhang |
| ▸ | Cutting edge height — set the cutting edge at spindle centerline height |
| ▸ | Insert seat condition — check that the contact surface is not damaged or worn |
| ▸ | Secure clamping — the insert must have no play in the seat |
| ▸ | Indexing — when an edge wears out, rotate the insert to a fresh edge (2 edges in total) |
Note: Use internal coolant (through the spindle) for boring whenever possible. When machining without coolant, reduce cutting parameters by 20–30%. Long tool overhang promotes vibration — if vibration occurs, reduce the depth of cut and increase the feed.
Frequently asked questions — S08 SCLCR 06
The minimum bore diameter is Ø11 mm. In smaller bores, the tool head interferes with the machined wall, preventing proper cutting.
For a steel shank of Ø8 mm, the recommended maximum overhang without damping is 4×d, or 32 mm. Above this value, vibration may occur — reduce the depth of cut or use a vibration-damped boring bar.
The CCMT insert has positive geometry (clearance angle 7°), which means it is single-sided with 2 cutting edges. When one edge wears out, rotate the insert to a fresh edge.
Product accessories

Carbide insert CCMT 060202 H6310 Horn
Reference: 0000006504 In stock > 10 items
€3.16
€3.88 brutto


Carbide insert CCMT 060204 H6310 Horn
Reference: 0000005754 In stock > 10 items
€3.16
€3.88 brutto
Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you







This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.