






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot
Description
Internal threading turning tool SIL S20P 16 Smoxh
Left-hand boring bar S20P SIL-16 for 16 IL indexable inserts
| Technical data | |
|---|---|
| Manufacturer designation | S20P SIL-16 |
| Machining operation | Internal threading |
| Design | Left-hand (L) |
| Shank diameter | Ø20 mm |
| Overall length | 170 mm |
| Distance from cutting edge to shank axis | 12.5 mm |
| Minimum bore diameter | Ø24 mm |
| Insert family | 16 IL (also 16 ER) |
| Thread types with the appropriate insert | Metric M – 60° Parallel pipe G – 55° Unified UN – 60° |
| Metric pitch range | 0.5–3.5 mm Depending on the selected 16 IL insert |

The photo shows a mirror image of the S25R SIR-16 boring bar.
The data in the table applies to the left-hand S20P SIL-16 boring bar.
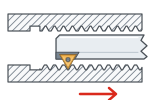
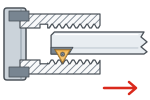
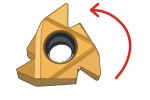
S20P SIL-16 – internal thread turning in practice
The workpiece with a bore rotates while the boring bar moves along the bore axis
Internal threading turning tool SIL S20P 16 Smoxh is a left-hand boring bar for threading bores in bushings, nuts, and housings. The Ø20 mm shank is clamped in a sleeve or boring bar holder. With a suitable 16 IL insert, you can cut metric M and inch UN threads with a 60° profile, as well as G parallel pipe threads with a 55° profile.
The metric pitch range is 0.5–3.5 mm, depending on the selected insert. Example: an M27x2 thread has a pitch of 2 mm, so it requires a 16 IL 2 ISO insert. For inch G and UN threads, match the insert to the profile and threads per inch (TPI). This is an indexable turning tool: when the cutting edge wears out, only the insert is replaced, while the body is retained.
The smallest bore the boring bar can enter is Ø24 mm. This allows metric threads starting at M27x2 and pipe threads starting at G 3/4 to be cut. Larger threads can be cut with the same boring bar because the thread diameter is determined by the bore in the part.
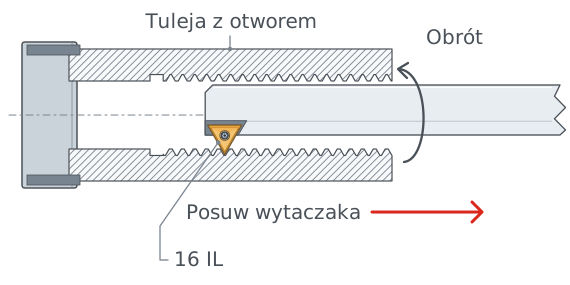
Illustrative diagram. Left-hand boring bar, left-hand thread, feed toward the tailstock.
How does an internal threading tool work?
The insert deepens the same profile with each successive pass. The feed remains synchronized with spindle rotation. For a single-start thread, boring bar travel per revolution equals the thread pitch.
The left-hand boring bar has a mirror-image design and uses 16 IL inserts. It is primarily intended for left-hand threads. The hand of the resulting thread also depends on tool orientation, spindle rotation, and feed direction.
16 IL inserts – selecting the thread profile and pitch
One holder, different tasks with the appropriate insert
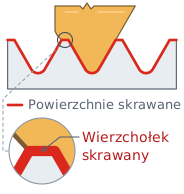
Full profile 16 IL ISO
A full-profile insert, such as 16 IL 1.5 ISO, is designed for a specific pitch. It machines the thread flanks, root, and crest. A different pitch requires the appropriate insert variant.
Example: metric profile, 1.5 mm pitch.
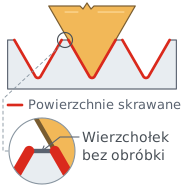
Partial profile 16 IL AG60
A partial-profile insert, such as 16 IL AG60, covers pitches of 0.5–3 mm (48–8 threads per inch). It does not finish the thread crests. The bore diameter must be prepared beforehand with a suitable tool.
Selection: profile, pitch range and insert grade.
Choose a full-profile insert for production runs of a single thread. The crest is formed together with the flanks, without a separate operation, and the profile is repeatable. An AG60 insert with a 60° profile or an AG55 insert with a 55° profile covers several pitches, making it useful for short runs and individual parts. The crest then depends on the previously bored diameter, so profile control is less precise. The left-hand boring bar also accepts 16 ER inserts, which have the same shape as 16 IL inserts.

The final “16” indicates the insert size, not the diameter of the thread being cut. The thread profile and pitch depend on the selected 16 IL insert. The 11 IL and 16 EL inserts are not used as direct replacements for each other. The full profile of a 16 ER insert corresponds to an external thread, so choose 16 IL inserts for internal threading.
Threading with a boring bar on a lathe – setup and feed
Short overhang, correct cutting edge height and synchronized motion
Set the cutting tip at spindle center height. Check the alignment of the insert profile relative to the bore axis. A steel boring bar operates stably with an overhang of up to approximately 4 shank diameters, or approximately 80 mm. Remove chips from the pocket and support surfaces before mounting.
Select the cutting speed and number of passes to suit the insert, material, and clamping rigidity. The SIL body alone does not determine cutting data for steel, stainless steel, or aluminum.
The SIL S20P 16 Smoxh internal threading turning tool requires a sleeve or tool post for a Ø20 mm shank. It fits holes from Ø24 mm, so check the hole diameter before threading. The overall length of 170 mm describes the body, not the permissible working overhang. Check the final thread dimensions against the requirements of the part drawing.
Feed for a 1.5 mm pitch
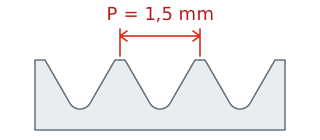
Pitch P is measured along the axis between corresponding points on adjacent thread turns.
For a single-start thread, the tool moves axially by 1.5 mm for each spindle revolution.
Feed per revolution:
fn = P = 1.5 mm/rev.
Example: spindle speed n = 400 rpm
vf = n × P = 400 × 1.5
600 mm/min
Feed rate
400 rpm is a calculation example, not recommended cutting data. The threading cycle requires the feed to be synchronized with the spindle.
Internal thread turning with a boring bar – approach, cutting pass and retraction
Each pass uses the same four movements, going slightly deeper each time
An internal thread is cut in several passes. In each pass, the boring bar repeats the same cycle of four movements, and the 16 IL insert cuts slightly deeper into the bore wall each time until the profile reaches full depth. The diagram shows one pass of a left-hand SIL boring bar cutting a left-hand thread, with feed toward the tailstock.
Single-pass cycle
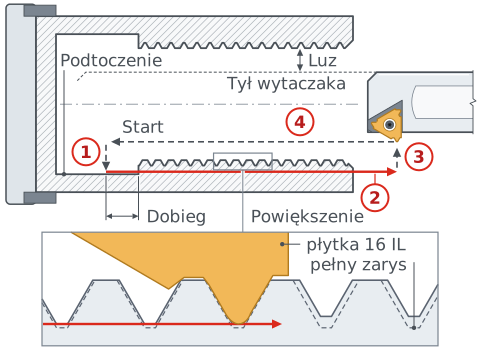
Schematic diagram, sleeve cross section. Red line – cutting movement, the insert is cutting. Dashed lines – rapid movements without cutting.
1
Approach
The boring bar enters the relief groove near the bottom of the bore and feeds outward from the axis toward the wall to the depth for this pass. This is a rapid movement without cutting.
2
Cutting pass
The insert cuts as it moves from the bottom toward the bore opening, toward the tailstock. For each spindle revolution, the boring bar advances by the thread pitch P, for example 1.5 mm.
3
Retraction
Beyond the bushing face, the insert exits the material and the boring bar rapidly retracts from the wall toward the axis. The retraction is short because the boring bar then returns into the bore, and its back must not touch the opposite wall.
4
Return
The retracted boring bar rapidly returns into the bore to the starting point in the relief groove. It starts the next pass with a slightly deeper infeed.
The left-hand boring bar starts threading at the bottom end, so the relief groove near the bottom is the starting point. It accommodates the insert tip and a short approach distance over which the feed synchronizes with the pitch before the insert enters the material. The total insert infeed depth for an internal thread is approximately 0.58 × P, or approximately 0.87 mm at a pitch of 1.5 mm. Make the relief groove deeper than the infeed depth and wider than 1.05 × P, or approximately 1.6 mm, because it accommodates both the insert and the approach distance. Chips remain in the bore, so for small diameters, direct coolant precisely into the cutting zone.
Boring bar infeed and number of passes in thread turning
The infeed direction determines which insert edge cuts
Infeed is the movement that takes the insert deeper into the bore wall on the next pass. Its direction determines which insert edge cuts and how the chip flows. In the diagrams, the bore wall is at the bottom and the boring bar approaches from the axis. Red lines show successive positions of the insert tip, and the arrow shows the infeed direction. The numbers 1–5 and progressively darker bands indicate successive passes. The bold line shows the insert edge that is cutting.
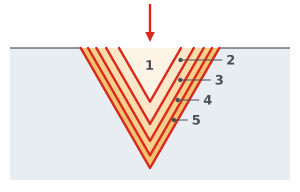
Radial infeed
The insert feeds straight into the wall, perpendicular to the axis, and cuts with both edges. This is the simplest method. It works well for fine pitches, short-chipping materials and hardened materials.
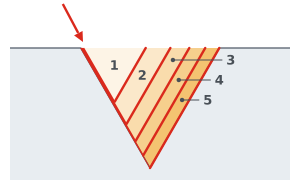
Modified flank infeed
The boring bar moves diagonally along the flank, or side of the profile, at an angle a few degrees less than 30°. One edge does most of the cutting, while the other does not rub against the thread flank. Manufacturers recommend this method as the first choice for most threads.
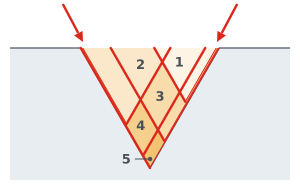
Alternating flank infeed
The boring bar alternately moves along each flank of the profile, so both edges wear evenly. This method helps with coarse pitches and long-chipping materials. It requires a program that is not available on every lathe.
Select the number of passes according to the pitch, material and thread type – insert manufacturers' catalogs list internal threading as a separate selection factor. For a pitch of 1.5 mm, they specify 5–11 or 6–10 passes; harder materials require more passes. The first pass is the deepest, and each subsequent pass is shallower. The final pass should not be shallower than approximately 0.05 mm, or the edge will start rubbing instead of cutting.
SIL S20P 16 – questions about selection and applications
Key information before selecting a boring bar
The boring bar accepts left-hand internal threading inserts from the 16 IL family, such as 16 IL AG60 and 16 IL AG55. It also accepts 16 ER inserts with the same shape, such as the 16 ER AG60 partial-profile insert. Select the profile, pitch, and grade suitable for the application.
The number 20 is the shank diameter in millimeters, and the letter P corresponds to a length of 170 mm in this model. The final 16 indicates the insert size, not the thread diameter. The thread diameter is determined by the bore in the part.
The boring bar fits holes from Ø24 mm. This includes the hole for M27x2 (thread minor diameter 24.83 mm) and the hole for G 3/4 (24.12 mm). You can cut larger threads with the same boring bar by selecting a suitable 16 IL insert.
For internal G pipe threads to ISO 228-1, from G 3/4 to G 6. G 3/4 has 14 threads per inch, so it requires an 16 IL 14 W insert. Sizes G 1 and larger have 11 threads per inch and use a 16 IL 11 W insert.
Yes, with a 16 ER/IL grooving insert installed. It fits size 16 left-hand SIL boring bars, so you can cut an internal groove without a separate tool. Match the insert width to the groove width on the part drawing and check the permissible depth in the insert data sheet.
Product accessories


Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you


This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.