







Description
| Technical Data | |
|---|---|
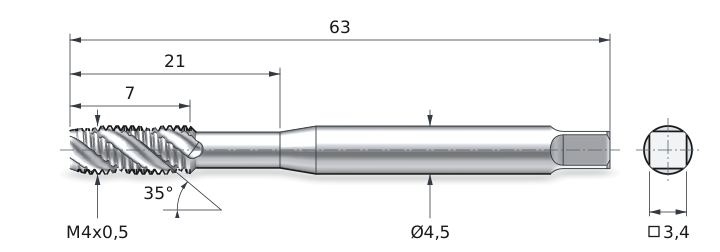
| Nominal Diameter d1 | M4x0.5 |
| Thread Pitch P | 0.5 mm |
| Helix Angle | 35° |
| Overall Length l1 | 63 mm |
| Flute Length l2 | 7 mm |
| Length l3 | 21 mm |
| Shank Diameter d2 | 4.5 mm |
| Square Drive Size a | 3.4 mm |
| Tap Drill Diameter | 3.5 mm |
| Chamfer | C (2÷3) P |
| Thread tolerance | 6H |
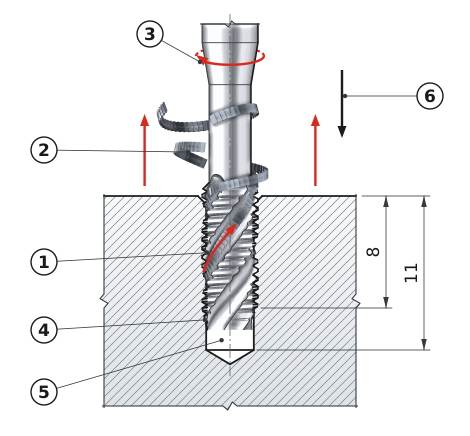
The 35° flute works like a screw conveyor
The flutes of this tap spiral to the right at an angle of 35° to the axis. The tap rotates clockwise and advances into the hole. A chip cut by the chamfer enters the flute, and the helix carries it upward like the auger in a meat grinder. The bottom of the hole remains clean, and the cutting edges do not encounter compacted chips. The M4x0.5 tap has a reinforced shank in accordance with DIN 371: diameter 4.5 mm, square size 3.4 mm.
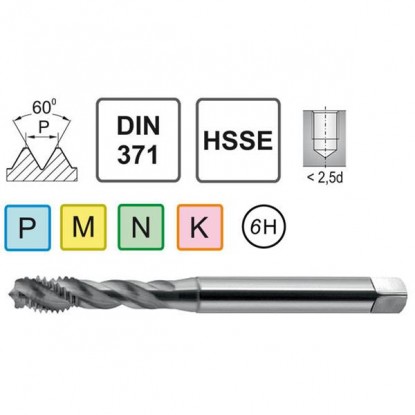
The M4x0.5 spiral flute machine tap with a fine pitch is designed for precise tapping of blind holes in precision engineering. Its HSSE steel construction with 5% added cobalt ensures a hardness of 65-67 HRC and long cutting edge life even when machining difficult materials. The 35° spiral flute design directs chips rearward, which is essential for blind hole tapping. The short shank in accordance with DIN 371 is suited to miniature machine tool holders. The 6H tolerance ensures the dimensional repeatability required in precision manufacturing.
The M4x0.5 spiral flute tap is used in precision engineering and electronics for producing components requiring leak-tight threaded connections. The fine pitch of 0.5 mm provides a larger contact area than the standard M4x0.7 thread. The tap drill diameter for an M4x0.5 thread is 3.5 mm in accordance with metric fine thread tables.
| Material | Cutting speed Vc [m/min] | Spindle speed n [rpm] | Feed f [mm/min] |
|---|---|---|---|
| PSteel | 5-20 | 398-1592 | 199-796 |
| MStainless steel | 5-10 | 398-796 | 199-398 |
| KCast iron | 5-15 | 398-1194 | 199-597 |
| NAluminum | 10-25 | 796-1989 | 398-994 |
NC spotting drill 90°
Ø 3.5 mm
M4x0.5
Tolerance 6H
Standard: DIN 371 | Chamfer: C (spiral flute) | Application: blind holes
| Class | Accuracy | Application | Status |
|---|---|---|---|
| 4H / 4g | High | Precision connections, hydraulics | — |
| 6H / 6g | Standard | Machine building, general-purpose | SELECTED |
| 7H / 8g | Low | Large clearance, easy assembly | — |
6H = internal thread (nut, hole) | 6g = external thread (screw)
The M4x0.5 HSSE metric fine thread machine tap performs well in structural steels with strengths up to 900 MPa, stainless steels, aluminum, and brass. The fine pitch of 0.5 mm provides improved sealing and vibration resistance in precision connections.
For the M4x0.5 metric fine thread in tolerance class 6H, the tap drill diameter should be 3.5 mm. The permissible hole tolerance range is 3.5-3.6 mm. A smaller hole increases cutting torque and the risk of tool breakage.
Yes, cooling with tapping oil or minimum quantity lubrication (MQL) is recommended due to the small diameter. The tool requires careful handling and low cutting speeds.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


