






Description
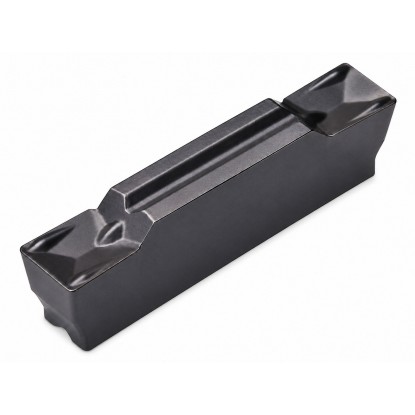
MGMN 300 insert in grade H5115 is a double-ended carbide insert from the Korean company Horn, designed for parting, grooving, and turning cast iron.
MGMN 300 H5115 dimensions and geometric parameters
| Technical data | |
|---|---|
| Cutting width b | 3 mm |
| Corner radius r | 0.4 mm |
| overall length l | 21 mm |
| width d | 3.3 mm |
| height t | 4.8 mm |
Turning operations in cast iron with the MGMN 300 H5115 insert
Speeds and feeds for 3 machining operations in cast iron
| Material | Parting | Facing | Grooving / turning | |||
|---|---|---|---|---|---|---|
| Vc [m/min] | fn [mm/rev] | Vc [m/min] | fn [mm/rev] | Vc [m/min] | fn [mm/rev] | |
| K Gray cast iron (GJL) | 100 – 160 | 0.10 – 0.28 | 120 – 180 | 0.12 – 0.32 | 110 – 170 | 0.10 – 0.25 |
| K Ductile cast iron (GJS) | 80 – 120 | 0.08 – 0.20 | 90 – 140 | 0.10 – 0.24 | 80 – 130 | 0.08 – 0.20 |
| K Malleable / hardened cast iron | 50 – 90 | 0.06 – 0.15 | 60 – 100 | 0.08 – 0.18 | 50 – 90 | 0.06 – 0.15 |
Grade H5115 with a CVD Al₂O₃ coating
The MGMN 300 H5115 Horn insert is a double-ended carbide insert with a cutting edge width of 3 mm, designed for parting larger-diameter cast iron shafts and cutting wider external grooves in cast iron on conventional and CNC lathes. The cemented carbide grade H5115 with a multilayer aluminum oxide (Al₂O₃)-based CVD coating covers the ISO K10-K30 application range, specializing in machining gray, ductile, and malleable cast iron, with the ability to part cast steel and hardened cast iron. The wide 3 mm cutting edge provides high rigidity and stability during deeper parting cuts and allows significantly higher feed rates than the 1.5 and 2 mm versions. The insert is compatible with MGMN-type indexable tools with a spring clamping system. Its 2-edge design allows the insert to be indexed after the first edge wears out and machining to continue without replacement.
The MGMN 300 cast iron parting insert is suitable for series production of larger-diameter cast iron shaft components, machining hydraulic housings, parting heavy workpieces, and cutting wide grooves. The recommended cutting speed Vc is 100-160 m/min for gray cast iron and 80-120 m/min for ductile cast iron at feed rates of 0.08-0.25 mm/rev. Dry machining is recommended for gray cast iron — cooling is unnecessary and may shorten coating life due to thermal shock; compressed air cooling is acceptable for ductile cast iron.
for the MGMN 300 insert (groove width 3 mm)
The MGMN 300 insert in grade H5115 is specialized for machining cast iron in the ISO K10-K30 range: gray (GJL), ductile (GJS), and malleable cast iron. It can also part cast steel and hardened cast iron. For structural and stainless steels, a general-purpose grade such as H6310 is a better choice.
No. Dry machining is recommended for gray cast iron — the graphite in the material structure acts as a natural lubricant, while emulsion cooling can cause thermal shock and cracking of the CVD coating. For ductile cast iron, compressed air cooling is acceptable for chip removal.
With a cutting edge width of 3 mm and standard mounting in the holder, the MGMN 300 insert can part cast iron shafts up to 26 mm in diameter. For smaller diameters and less material loss, choose MGMN 200 (2 mm), and for larger diameters, use MGMN 400 (4 mm) or a BDKT parting blade with extended overhang.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


