







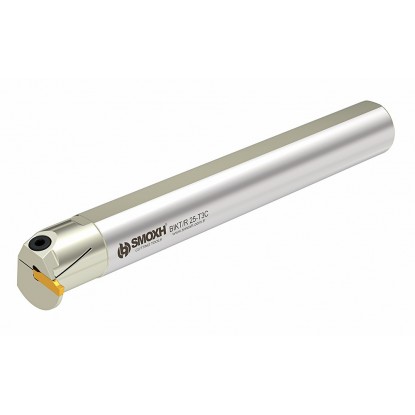

Description
Technical data for the boring bar for Korloy MGMN 400 inserts
| Technical data | |
|---|---|
| Designation | BIKT R 20 K4C T6 |
| Manufacturer's code | SM11229 |
| Shank diameter d | Ø20 mm |
| Height to flat h | 18 mm |
| Overall length L | 170 mm |
| Head length l | 33 mm |
| Dimension f (centerline – cutting edge) | 15.75 mm |
| Groove depth T max | 6 mm |
| Minimum bore diameter D min | Ø26 mm |
| Insert pocket | MGM. 4C (MGMN 400, width 4 mm) |
| Hand | R – right-hand (left-hand version: SM11366) |
Round shank with a flat, screw clamp, and double-ended insert
Grooving boring bar 4 mm BIKT-R 20 K4C T6 is a Smoxh tool for cutting internal grooves in bores from Ø26 mm. The MGMN 400 carbide insert is held by a screw clamp: the BKTV M5x17 screw draws the head's flexible lip against the insert. Changing the insert takes a dozen or so seconds without removing the tool from the holder.
The shank is a Ø20 mm bar, 170 mm long, with a flat machined to a height of h = 18 mm. The flat locates the cutting edge in the reduction sleeve or V-block tool holder, so the insert edge returns to the same height each time it is clamped.
The 33 mm long head carries an insert pointing radially outward. The cutting edge projects 6 mm beyond the shank profile, which is the groove depth T max. This sets the limit: the Ø20 mm shank plus the 6 mm cutting edge projection gives a minimum bore diameter D min = Ø26 mm.
The MGMN 400 insert is double-ended. When one edge becomes dull, rotate it 180° and use the other end.
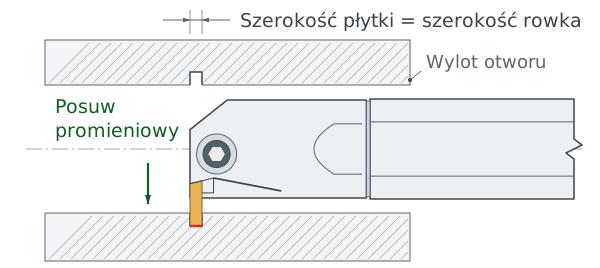
Internal groove in a single pass
A 4 mm groove for a retaining ring, seal, or undercut in a bore, up to 6 mm deep. The insert feeds radially into the wall to the specified depth.
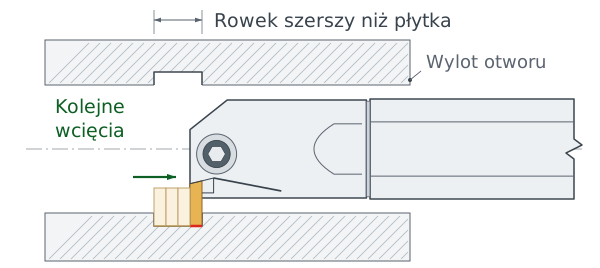
Groove wider than the insert
Two adjacent passes, with side turning between them at a depth of up to 0.8 × 4 mm = 3.2 mm. The -M or -T geometry allows side cutting.

Screw clamp
The BKTV M5x17 screw draws the head's flexible lip against the insert. The insert can be changed without removing the tool from the holder.

Double-edged insert
MGMN 400 has a cutting edge at both ends. One edge dull? Rotate the insert by 180° and use the other.

Bores from Ø26 mm
The Ø20 mm shank and 6 mm cutting edge projection must fit in the bore together: D min = 20 + 6 = Ø26 mm. In a smaller bore, the shank will contact the wall.
Top view, enlarged head detail, and end view in a D min bore
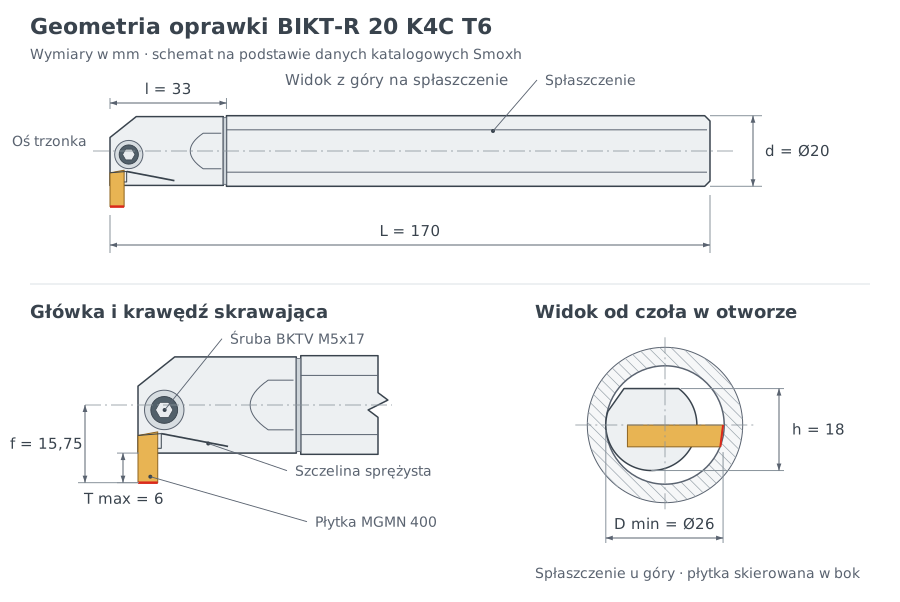

DIAMETER d
Ø20 mm

HEIGHT h
18 mm

LENGTH L
170 mm

DIMENSION f
15.75 mm
Dimension f = 15.75 mm is the distance from the shank centerline to the cutting edge. Dimension T max = 6 mm indicates the catalog grooving reach; the enlarged detail shows it from the head profile to the cutting edge. The end view shows the tool in a Ø26 mm bore: the cutting edge reaches the wall, with only working clearance remaining on the opposite side of the shank.
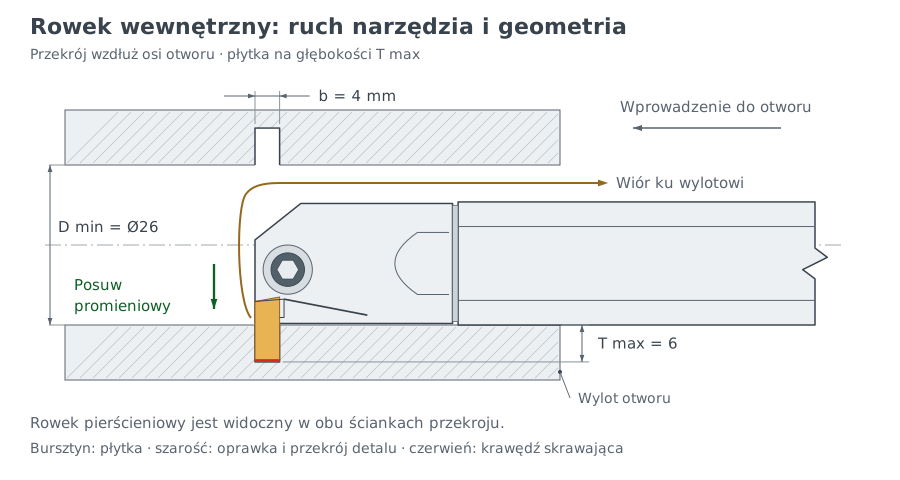
The tool enters through the bore opening, and the insert cuts radially into the wall to the groove depth. Chips have little room inside the bore, so direct coolant onto the insert and retract it every few millimeters. Set the cutting edge at the bore centerline height within ±0.1 mm.
Five elements of the Smoxh code, read from the left
Starting values with coolant; refer to the insert grade data sheet for definitive data
Values apply to coated MGMN 400 inserts when machining with coolant. Chips have less room inside a bore than outside, so start in the lower half of the feed range and keep tool overhang as short as possible.
| Workpiece material | Vc [m/min] | fn [mm/rev] |
|---|---|---|
| PCarbon steel | 120–200 | 0.07–0.15 |
| PAlloy steel | 130–180 | 0.07–0.15 |
| PHardened steel | 70–130 | 0.07–0.12 |
| MStainless steel | 120–160 | 0.07–0.15 |
| KCast iron | 130–210 | 0.07–0.15 |
Calculate spindle speed from the bore diameter, not the shank diameter: n = (1000 × Vc) / (π × D). For a Ø26 mm bore in carbon steel at Vc = 170 m/min: n = (1000 × 170) / (3.14 × 26) ≈ 2080 rpm. For a Ø60 mm bore, approximately 900 rpm is sufficient because the same cutting speed applies over a larger circumference.
Do not enter a bore smaller than Ø26 mm: the shank will contact the wall before the cutting edge reaches the full groove depth. Keep overhang from the holder as short as possible, approximately up to 4 × d = 80 mm, because a longer steel bar starts to vibrate and chips the insert corner. For a retaining ring groove, check the insert width with a caliper: the groove must be wider than the ring by the clearance specified in the ring standard, rather than equal to the insert width.
the BKTV M5x17 screw with the wrench SAK-AA4, 2–3 turns
clean the pocket, slide the insert in until fully seated
and check that the cutting edge is at bore centerline height ±0.1 mm
grooves in bores from Ø26 mm
Cutting insert not included
COMPATIBLE WITH:
| ✓ | MGMN 400 grooving inserts (Smoxh: MGM. 4C) – width 4 mm, length 21 mm, height 4.8 mm |
| ✓ | BKTV M5x17-9211 clamping screw (spare part) and SAK-AA4-9903 wrench |
| ✓ | Mirror-image version BIKT-L 20 K4C T6 (SM11366) with the same dimensions |
| ✓ | Holders for a Ø20 mm round shank with a flat: reduction sleeve or V-block tool holder |
The 4 mm BIKT-R 20 K4C T6 grooving boring bar cuts grooves 4 mm wide and up to 6 mm deep in bores from Ø26 mm, at a cutting speed of 120–200 m/min and a feed of 0.07–0.15 mm/rev in carbon steel. In hydraulic and pneumatic applications, it cuts internal grooves for sealing and retaining rings in bushings and cylinders. Inserts from other grooving systems, such as DGN or KGM, use different pockets and do not fit this holder.
An MGMN 400 grooving insert (in the Smoxh catalog: MGM. 4C) with a width of 4 mm, length of 21 mm, and height of 4.8 mm. It is double-ended, so one insert provides two cutting edges. DGN, GTN, and KGM inserts do not fit this pocket.
Ø26 mm. This is the shank diameter of 20 mm plus the groove depth of 6 mm. In a smaller bore, the shank will contact the opposite wall before the cutting edge reaches full depth. BIKT R 25 K4C T7 works in larger bores (from Ø32 mm), and this tool has no restrictions there.
Start at approximately 2080 rpm for carbon steel, at Vc = 170 m/min with a 4 mm insert. Calculate spindle speed from the bore diameter, so approximately 900 rpm is sufficient for Ø60 mm. For stainless steel, use Vc 120–160 m/min.
Up to 6 mm deep, which is T max. In a single pass, the groove width equals the insert width of 4 mm; wider grooves require adjacent passes and side turning. For grooves deeper than 3 mm, retract the insert every few millimeters to clear chips from the bore.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


