





- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot
Description
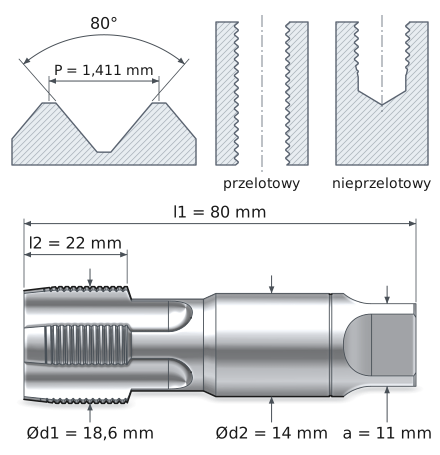
Technical data for PG 11 hand taps for electrical conduit
| Technical data | |
|---|---|
| Nominal diameter d1 | Pg 11 |
| Thread diameter | 18.6 mm |
| Thread pitch P | 18 threads per inch / 1.411 mm |
| Overall length l1 | 80.0 mm |
| Flute length l2 | 22 mm |
| Shank diameter d2 | 14 mm |
| Square drive size a | 11.0 mm |
| Thread angle | 80° |
| Thread standard | DIN 40430 |
| Tap drill hole | 17.25 mm |
Roughing tap and finishing tap – how much material each removes
Division of work in the 1–2 set
A Pg 11 thread is cut into the wall of a hole with a diameter of 17.25 mm. The thread groove extends 0.68 mm into the wall. A single tap would have to cut the entire groove at once – by hand, this means high resistance and a risk of breakage. The set divides this work into two passes.
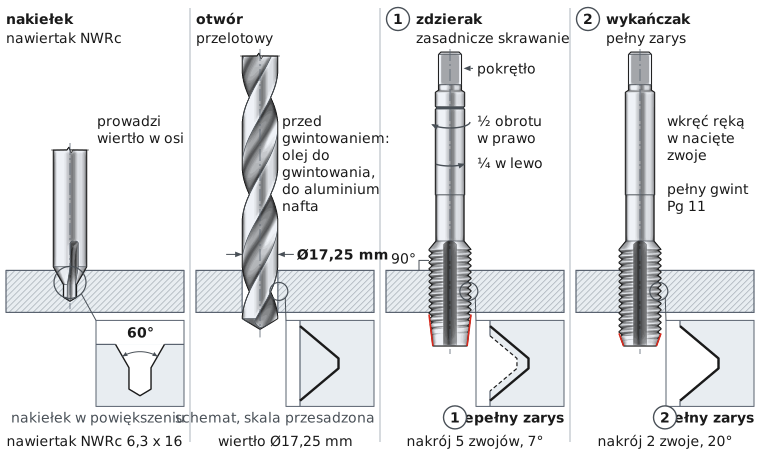
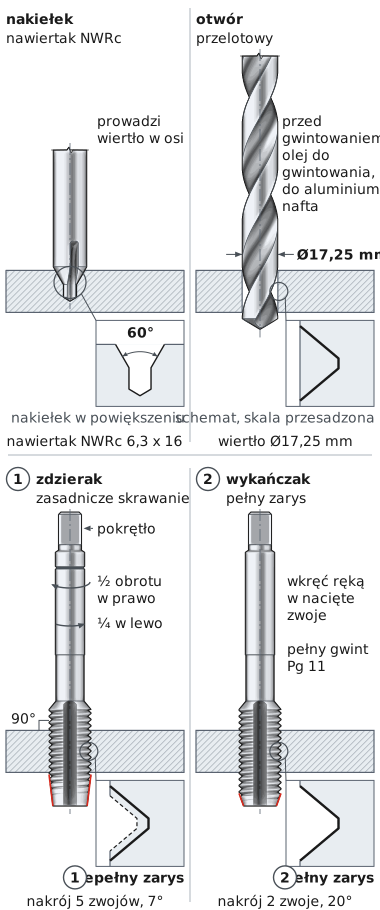
The drawing shows the entire set in operation. Both taps have the same shank and the same length. They differ in their chamfer, the tapered tip: No. 1 has a chamfer spanning 5 threads, while No. 2 spans only 2 threads. The detail windows at the hole wall show how the thread groove deepens after each tap.
| Tap | Chamfer | Chamfer angle | Material removed | How it works in the hole |
|---|---|---|---|---|
| No. 1 – roughing tap | long, 5 threads | 7° | the main portion of the groove | enters smoothly and establishes thread alignment |
| No. 2 – finishing tap | short, 2 threads | 20° | the remainder, to the full profile | screws into the previously cut threads and produces the full thread profile |
How to distinguish the taps in the set
The chamfer on No. 1 is 2.5 times as long as the chamfer on No. 2 – the difference is immediately visible when you place them side by side. No. 1 has an incomplete thread profile; only No. 2 has the full profile. The number is also indicated on the shank: No. 1 has one ring, No. 2 has none. Keep the set together and always start with the roughing tap.
How to tap a Pg 11 hole – sequence 1, 2
Hand tapping step by step
Thread Pg 11 in four steps
ØDrilling
Drill bit 17.25 mm
1Roughing tap
Chamfer 5 threads
2Finishing tap
Chamfer 2 threads
✓Finished thread
Thread Pg 11
Turning sequence: half a turn clockwise, a quarter turn counterclockwise | Between taps: remove chips from the hole
Start with the hole. Pg thread pitch is specified in threads per inch: 25.4 mm : 18 threads = 1.411 mm. The 80° profile is shallow, so the 17.25 mm drill bit is only 1.35 mm smaller than the 18.6 mm thread diameter – less than one pitch. Drill the hole with this exact drill bit. An undersized hole is a common cause of a tap twisting off in the material.
Through hole or blind hole – how deep to drill
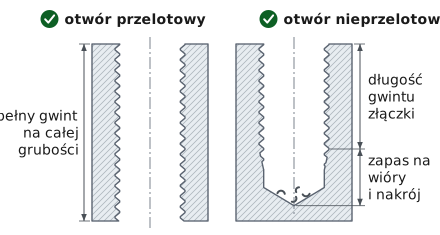
The set taps both types of holes. In a through hole, the thread extends through the full material thickness. In a blind hole, cut the thread to match the thread length of the fitting being installed. Drill the hole deeper than the thread. The finishing tap has a 2-thread chamfer, so approximately 2 incomplete threads remain near the bottom. The extra depth below the thread accommodates these along with the chips.
No. 1 – the roughing tap establishes thread alignment
Fit the roughing tap in the tap wrench and position it perpendicular to the surface. Check the angle from two sides, for example with a square. Turn half a turn clockwise, then a quarter turn counterclockwise. Reversing breaks the chip into short pieces – a slight crunch is normal. The first threads determine whether the thread will be straight.
No. 2 – the finishing tap produces the full profile
Unscrew the roughing tap and remove the chips from the hole. Screw the finishing tap into the cut threads by hand – it should engage them on its own. Continue turning at the same rhythm as with the roughing tap. The finishing tap removes the remaining material and cuts the groove to its full profile. When it screws in smoothly all the way, the thread is ready – check it with a fitting with a Pg 11 thread.
High-quality FWP hand taps for professional thread cutting in electrical conduits. Tap type NGSy, size Pg-11. The taps are sold as a set of 2 pcs. The complete thread is cut in two successive operations using a special tap wrench. Pg thread angle: 80°. Our NGSy hand taps are manufactured to DIN 40432 from modern high-speed steel (HSS). This steel offers high resistance to demanding cutting conditions, high hardness, and durability. These properties increase the strength of the taps and their resistance to potential breakage, cracking, and other cutting-edge damage when machining hard materials. The taps are suitable for cutting hard carbon steels, metals, nonferrous metals, metal alloys, and other materials.
Product accessories


HSSE 18.5 cobalt metal drill bit DIN 338
Reference: 13299 In stock > 10 items
€18.42
€22.66 brutto

Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you


This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.